Procurement Knowledge Base
Frequently Asked Questions for Apparel Sourcing Directors
Direct technical answers addressing minimum order quantities, lead times, tech packs, and regulatory compliance.
What is your standard Minimum Order Quantity (MOQ) for custom private label apparel?
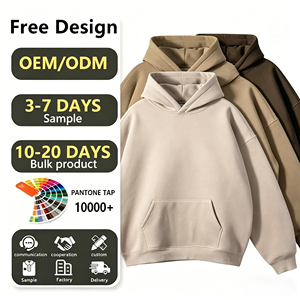
Our baseline Minimum Order Quantity (MOQ) is 200 pieces per style/colorway. Within this 200-piece allocation, clients can freely split sizes (e.g., S through 3XL) at no additional charge. For custom fabric developments, specific GSM knits, or complex custom washes (such as vintage acid wash or dirty thermal dyeing), MOQs remain optimized at 200 units to support scaling emerging and established brands.
How does CE Certification benefit global apparel brands importing into Europe and North America?
CE Certification confirms that our manufacturing ecosystem complies with European health, safety, and environmental protection legislation (including EU 2016/425 for protective/functional apparel and REACH chemical safety standards). For brand directors, this guarantees that all dyed cottons, trims, zippers, and print media are completely non-toxic, allergen-free, and resistant to heavy wear—preventing costly customs holds or legal liabilities in international markets.
What are the lead times for custom sampling and bulk apparel production?
We operate an expedited critical path:
- Costed Quotation & Spec Review: 24 to 48 hours.
- Physical Pre-Production Sample: 7 to 10 business days (includes pattern drafting, fabric cutting, printing/embroidery, and sample delivery).
- Bulk Cut & Sew Production: 2 to 3 weeks for standard fleece and jersey knits; 3 to 4 weeks for complex outerwear, denim, or specialty garment-dyed programs following sample sign-off.
Is a finalized tech pack required to begin manufacturing with your facility?
No, a finalized tech pack is not strictly required. While we accept industry-standard AI/PDF tech packs, our in-house pattern making and design engineering team can create production-ready tech packs from scratch using your reference garments, high-resolution photos, or basic measurement concept sketches. We supply graded measurement specs, stitch callouts, trim sheets, and print placement diagrams for your explicit approval prior to sampling.
Which heavy GSM fabrics and wash treatments do you specialize in for streetwear?
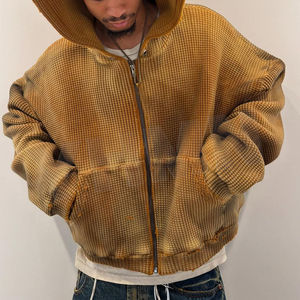
We specialize in ultra-heavyweight knits ranging from 380 GSM to 600 GSM in both 100% combed cotton and heavy 3-end French terry / fleece options. Our wash department executes specialized treatments including vintage acid wash, mineral wash, dirty thermal wash, silicone soft-hand enzyme treatments, and garment-dyeing with reactive pigments that maintain color depth through industrial wash testing.
How are shipping, customs clearance, and DDP/FOB logistics handled?
We export finished private label goods to over 30 countries across North America, Europe, Australia, and the Middle East. We support flexible commercial terms including FOB (Free on Board), CIF, and turnkey DDP (Delivered Duty Paid)—where our logistics team manages export documentation, customs duty filing, HS-code classification, and door-to-door freight directly to your fulfillment warehouse.
Can you manufacture complete custom private label packages ready for retail shelves?
Yes. We deliver 100% retail-ready apparel. Our finishing line handles custom woven neck labels, satin care labels, heat-transfer inner prints, custom branded hangtags with safety pins, individual polybag packing, and scannable UPC/EAN barcode stickers applied according to your exact warehouse compliance manual.
What quality control protocols are used to ensure garment fit and seam strength?
Our facility operates under an ISO 9001 certified quality management system. We execute a 4-Stage Quality Framework: 4-Point fabric inspection on raw rolls, hourly in-line measurement checks during sewing, 100% thread trimming and iron-press audits, and final statistical AQL 2.5 inspections before cartons are strapped and sealed for freight.