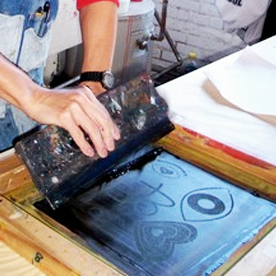
Silk Screen Printing
The gold standard for durability and color vibrancy. Utilizing high-tension mesh screens and premium plastisol or water-based inks, screen printing delivers crisp solid colors across cotton, polyester, and blended fabrics.

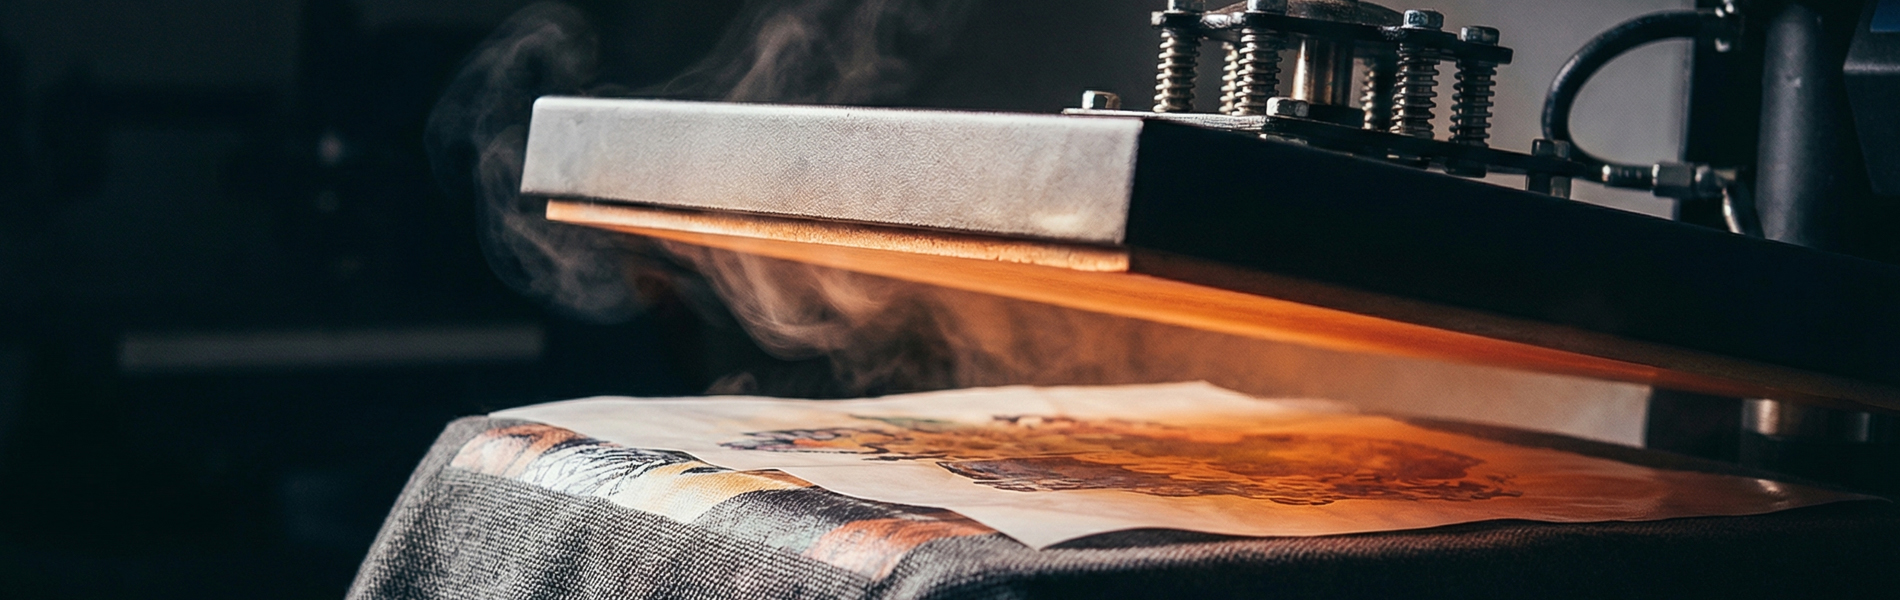
With over two decades of technical apparel production experience, Zega Apparel houses a complete in-house textile printing facility engineered for commercial fashion brands, streetwear labels, and corporate apparel buyers worldwide.
We solve the critical challenges of custom printing — precise art registration across seams, vibrant color payoff on dark cottons, soft hand-feel on high-GSM fleece, and print stability through repeated washing. Every printing technique is executed before or after garment assembly depending on design specs.
Selected according to your fabric weight, blend, visual effect, target unit price, and wash durability requirements.
The gold standard for durability and color vibrancy. Utilizing high-tension mesh screens and premium plastisol or water-based inks, screen printing delivers crisp solid colors across cotton, polyester, and blended fabrics.
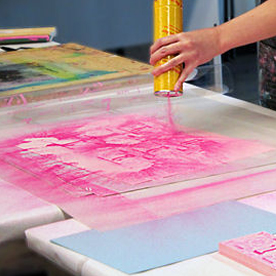
Integrates adhesive compounds with micro-fiber flocking to generate a raised, velvety texture. Perfect for adding a luxurious tactile dimension to varsity apparel, hoodies, and premium graphic tees.
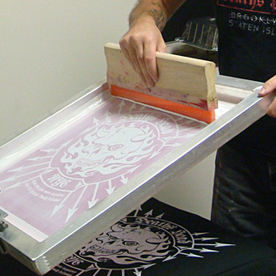
Uses water-soluble pigments that penetrate deep into natural cotton fibers. Yields an ultra-soft hand feel with zero ink weight, ideal for vintage fashion collections and light-colored garments.
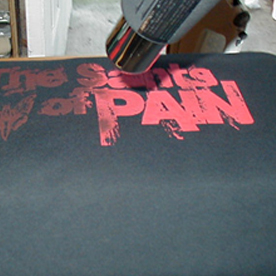
Employs a specialized bleaching agent that strips the original fabric dye while depositing fresh pigment. Results in vibrant prints on dark cotton garments without heavy plastisol buildup.
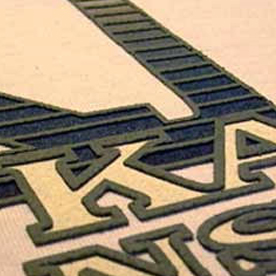
Uses heavy-viscosity silicone or specialty inks applied through thick capillary stencils. Produces clean, sharp-edged 3D raised graphic lettering on hoodies, sweatshirts, and activewear.
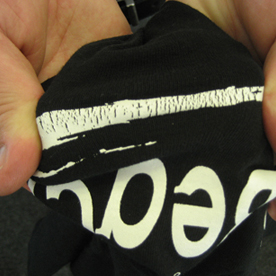
Formulated with specialty inks that fracture naturally upon heat curing. Delivers an authentic aged, worn-in, vintage aesthetic popular in streetwear aesthetic collections.
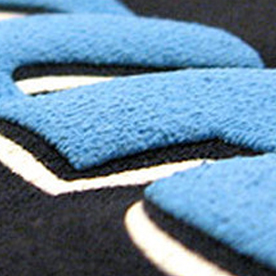
Incorporate foaming blowing agents into plastisol inks. When passed through heat tunnels, the ink expands upwards creating a smooth, rounded 3D raised effect across artwork focal points.
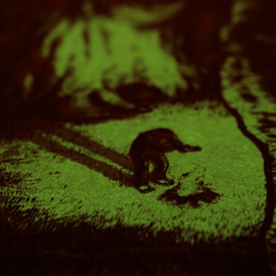
Formulated with phosphorescent pigments that absorb ambient light and glow in low-light environments. Perfect for night running gear, promotional merchandise, and novelty lines.
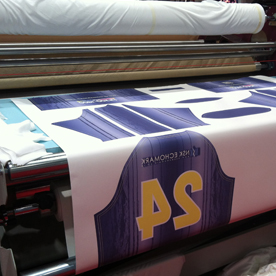
Heat-gaseous ink fusion into polyester yarns. Provides 100% seam-to-seam coverage for activewear and jerseys with zero cracking, peeling, or fading over long-term usage.
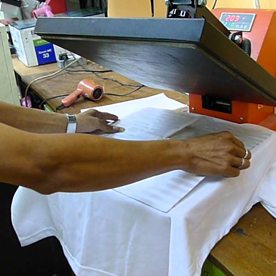
Precision thermal transfer ideal for intricate multi-color crests, chest logos, and tagless inner neck brand labels. Applies smoothly to cotton, synthetic, and blended knits.
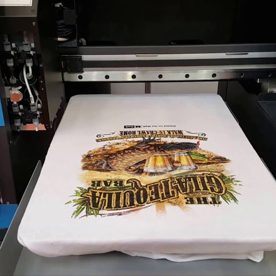
Direct digital ink jetting onto fabric panels before cutting. Excellent for high-resolution graphics, complex gradient transitions, and intricate multi-color graphics.
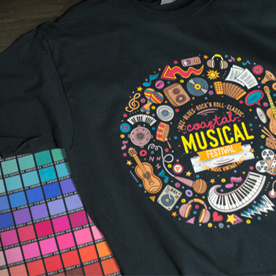
High-resolution inkjet technology printing directly onto pre-treated 100% cotton garments. Ideal for full-color artwork with unlimited shade variations and photographic prints.
Specifications and technical guidelines for overseas brand buyers and sourcing managers.
Preventing print defects like bleed-through, crocking, and misregistration through four inspection gates.
Digital film generation, mesh count selection (80–305 mesh), and Pantone matching with lab-dip strike-off approval.
Fabric pretreatment application for DTG/Discharge and test strike-offs to verify ink adhesion and stretch tolerance.
Hourly laser-guided registration checks, squeegee pressure balancing, and flash cure timing verification during runs.
Full infrared thermal curing followed by cross-hatch tape adhesion tests and ISO wash fastness verification before packing.
Clear answers to technical printing inquiries routinely raised by international brand buyers.
Send your tech packs, vector artwork, or print ideas to our engineering team. We will review artwork feasibility, advise on optimal print techniques, and generate a fast cost quotation.