MicroModal Boxer Briefs
Crafted with 180–210 GSM Lenzing MicroModal and 8% Elastane. Features anti-ride-up 6-inch inseams, seamless back construction, and ultra-soft 35mm brushed Jacquard elastics.

Industrial-grade precision for global apparel brands: 3D ergonomic pouch construction, MicroModal & GOTS organic fabrics, custom jacquard elastics, 200-unit MOQ, and AQL 2.5 quality control under one roof.
In the competitive underwear market, consumer retention hinges on three non-negotiable pillars: anatomical fit precision, fabric breathability, and seam integrity after dozens of wash cycles. Unlike general outer-apparel manufacturing, custom men undergarment manufacturing is an exacting technical discipline that allows zero margin for pattern error.
Operating from our owned 50,000 sq. ft. vertically integrated facility since 2012, Zega Apparel eliminates traditional supply chain vulnerabilities. We house advanced CAD pattern grading, high-density jacquard waistband weaving, precision laser cutting, and specialized 6-needle 4-thread flatlock machines under a single roof. This setup provides global procurement managers and DTC founders with full control over fabric hand-feel, elasticity modulus, shrinkage ratios, and brand packaging consistency.
From luxurious everyday MicroModal trunks to high-compression athletic base layers, explore our OEM/ODM manufacturing capability across every undergarment category.
Crafted with 180–210 GSM Lenzing MicroModal and 8% Elastane. Features anti-ride-up 6-inch inseams, seamless back construction, and ultra-soft 35mm brushed Jacquard elastics.
Engineered for maximum natural support using dual-layer anatomical U-convex pouch shaping. Available in 95% Organic Combed Cotton with anti-chafing flatlock seam construction.
High-gauge Nylon 6.6 / Spandex blends featuring silver-ion antimicrobial finish, zoned targeted compression mesh panels, and high-wicking quick-dry technology.
Eco-friendly, naturally hypoallergenic, and temperature-regulating bamboo viscose (190 GSM). Ideal for luxury boutique lines demanding supreme breathability and silky touch.
Heavyweight 240–280 GSM brushed interior poly-spandex or Merino wool blends designed for thermal insulation, moisture regulation, and extreme cold durability.
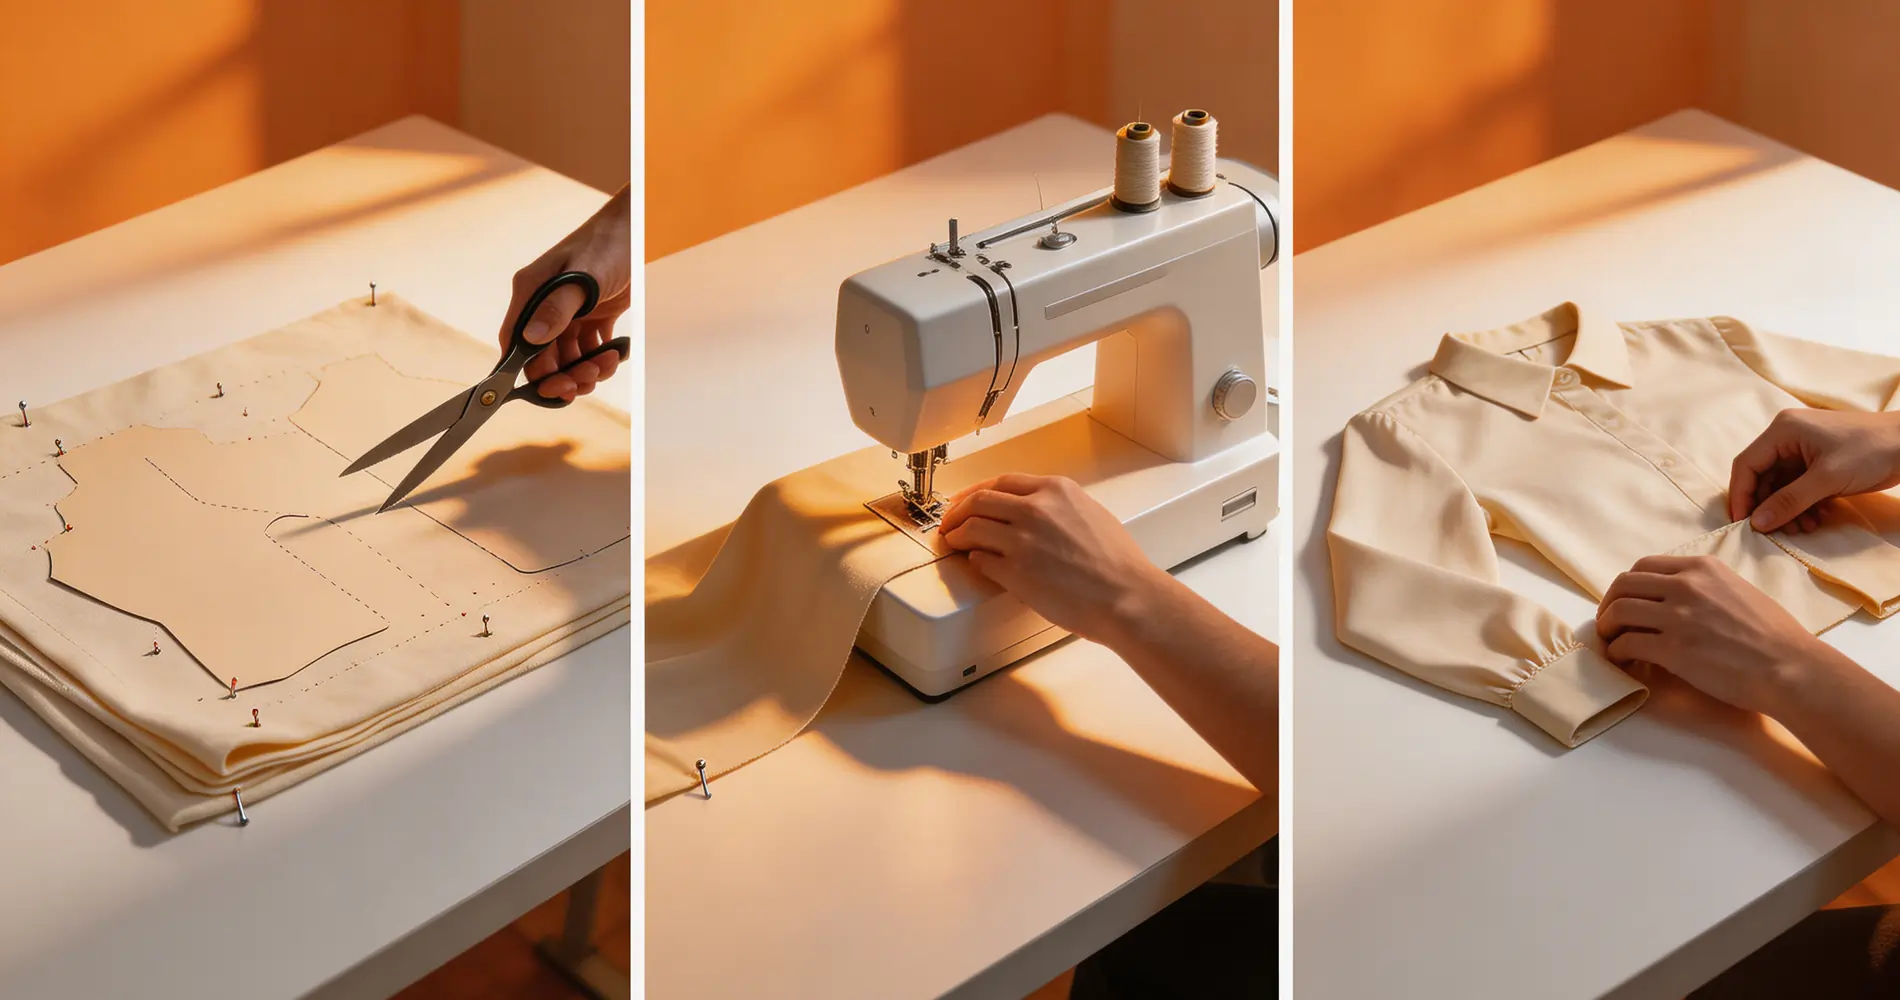
Ultrasonic bonded leg openings and heat-sealed side joins offering zero visibility under tailored pants. Perfect for modern minimalist athletic and formal wear brands.
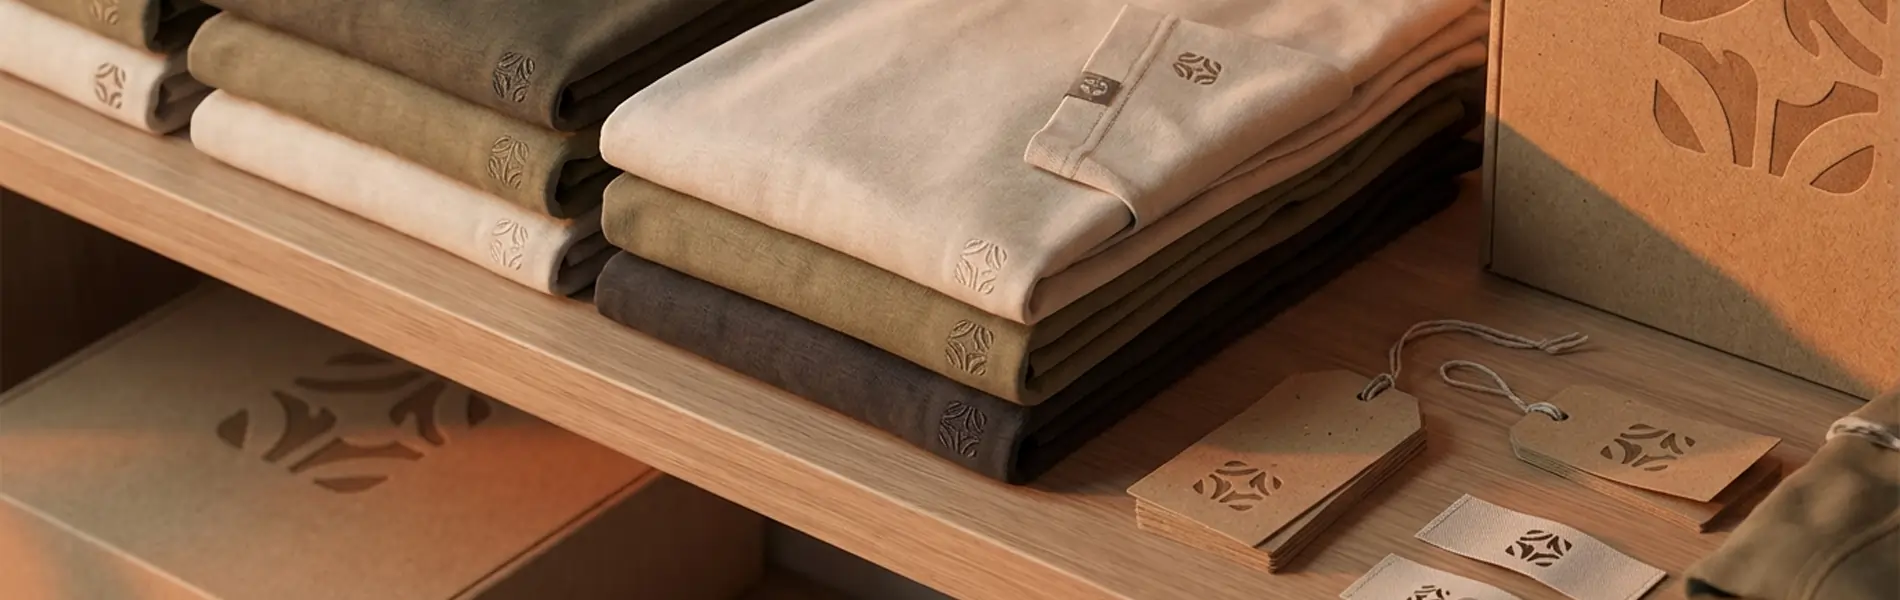
Turnkey packaging solutions: 3-pack rigid presentation boxes, matte polybags with zip locks, custom barcode stickers, heat-transfer inner tagless care labels.
Undergarment performance relies on precise textile blending, stretch recovery, and skin-level comfort. We source and custom-knit certified raw textiles to match your brand's hand-feel and target pricing.
Extracted from sustainable beechwood, our 180–210 GSM MicroModal provides twice the softness of cotton with superior moisture absorption and anti-pilling properties after 50+ industrial washes.
Combed long-staple organic cotton knitted with 5% to 8% Creora® or Lycra® Elastane. Delivers crisp shape retention, skin friendliness, and GOTS chemical compliance.
Ultra-durable, cool-touch micro-nylon engineered for sport and workout undergarments. Features quick-dry channels and 4-way mechanical stretch flexibility.
Custom woven elastic bands (30mm–50mm width) featuring high-density brand logos, soft plush interior backings, and optional anti-slip internal silicone grippers.
We utilize Yamato 6-needle 4-thread flatlock machines that lay seams completely flat to eliminate skin friction, alongside heat-bonded ultrasonic seamless edge technology.
Scratch-free tagless care labels applied via high-pressure heat press. Eco-friendly ink formulas ensure compliance with global chemical restriction standards (REACH/CPSIA).
As consumer preferences shift toward holistic wellness, sustainable materials, and adaptive clothing, global procurement teams must align with tech-forward manufacturing strategies.
The underwear market is moving rapidly beyond virgin synthetics. Global buyers are prioritizing certified recycled polyamides (Econyl®) and bio-based elastanes that degrade without leaving microplastics. Zega Apparel provides fully traceable eco-knits with GRS (Global Recycled Standard) certification.
Traditional flat-panel underwear is obsolete. Modern men demand engineered support—such as external hammock pouches, mesh cooling vents, and flyless ergonomic 3D shaping that reduces friction and prevents heat buildup during long working hours or athletic performance.
The rise of tight-fitting athleisure and tailored pants has accelerated demand for invisible underwear. Stitchless construction—utilizing laser-cut raw edges and TPU adhesive bonding tapes—is becoming a dominant product line for modern premium menswear brands.
Permanent, non-toxic silver-ion, zinc-pyrithione, and plant-based peppermint odor-reduction fabric treatments are no longer restricted to gym wear. Brands are embedding antimicrobial protection directly into daily cotton and MicroModal undergarment lines.
To reduce inventory risks and test new colorways or capsule collections, leading brands avoid massive 10,000-piece factory commitments. Zega Apparel’s agile 200-unit MOQ structure empowers brands to respond quickly to trending consumer preferences without over-committing capital.
Undergarment packaging is an essential point of brand experience. Industry procurement is shifting toward 100% home-compostable polybags, FSC-certified cardboard presentation boxes, and minimal plastic usage across the entire retail fulfillment chain.
Key performance indicators from our specialized men's underwear cut & sew lines over the past 24 months.
From initial tech pack creation to final packed export cartons, every phase is managed with meticulous detail under our strict quality assurance protocol.
We review your sketches or sample physical pairs, establish graded measurement specs (XS–5XL), design 3D pouch geometry, and generate high-density waistband artwork.
Custom fabric knitting, Pantone color matching lab dips, and waistband prototyping within 7–10 days. Fit samples are sent for your hands-on evaluation and approval.
Automated tension-free fabric spreading and laser cutting guarantee consistent panel sizing. Assembly uses 6-needle flatlock machines for smooth, chafe-free seams.
Every piece undergoes stretch recovery checks, waistband pull tests, and AQL 2.5 inspection. Undergarments are individually folded into custom branded packaging.
Because underwear rests directly against sensitive skin, micro-defects like loose threads, rough seam edges, or uneven waistband tension can damage a brand's reputation. At Zega Apparel, we implement a four-gate quality checkpoint system:
Transparent parameters to help procurement managers evaluate feasibility, timeline, and landed cost for custom men undergarment orders.
Real feedback from apparel brand founders who rely on our factory direct undergarment manufacturing facility.
“Finding a factory capable of producing high-end MicroModal boxer briefs with 6-needle flatlock seams at a 200-unit MOQ was nearly impossible until we partnered with Zega Apparel. Their waistband weaving accuracy and fit consistency across drops have allowed us to double our reorder velocity.”
Julian VanceFounder, LuxeBasics Menswear — USA“The 3D pouch pattern design Zega developed for our activewear line completely eliminated ride-up and chafing during intense workouts. Sampling took under 10 days, and bulk delivery reached our UK warehouse a week ahead of schedule.”
Liam HemsworthHead of Product, Apex Sportswear — UK“Zega Apparel’s private label service is top tier. They produced our GOTS organic cotton trunks complete with custom branded boxes, barcode labels, and tagless heat-transfer prints. Our defect rate across 5,000 units was zero.”
Stefan BrandtProcurement Director, EcoBodywear — GermanyDetailed technical and commercial answers to help procurement managers and brand owners make informed manufacturing decisions.
Send your tech specs, target fabric GSM, and design concepts to our factory team. Receive a transparent price quote and technical evaluation within 24 to 48 hours.