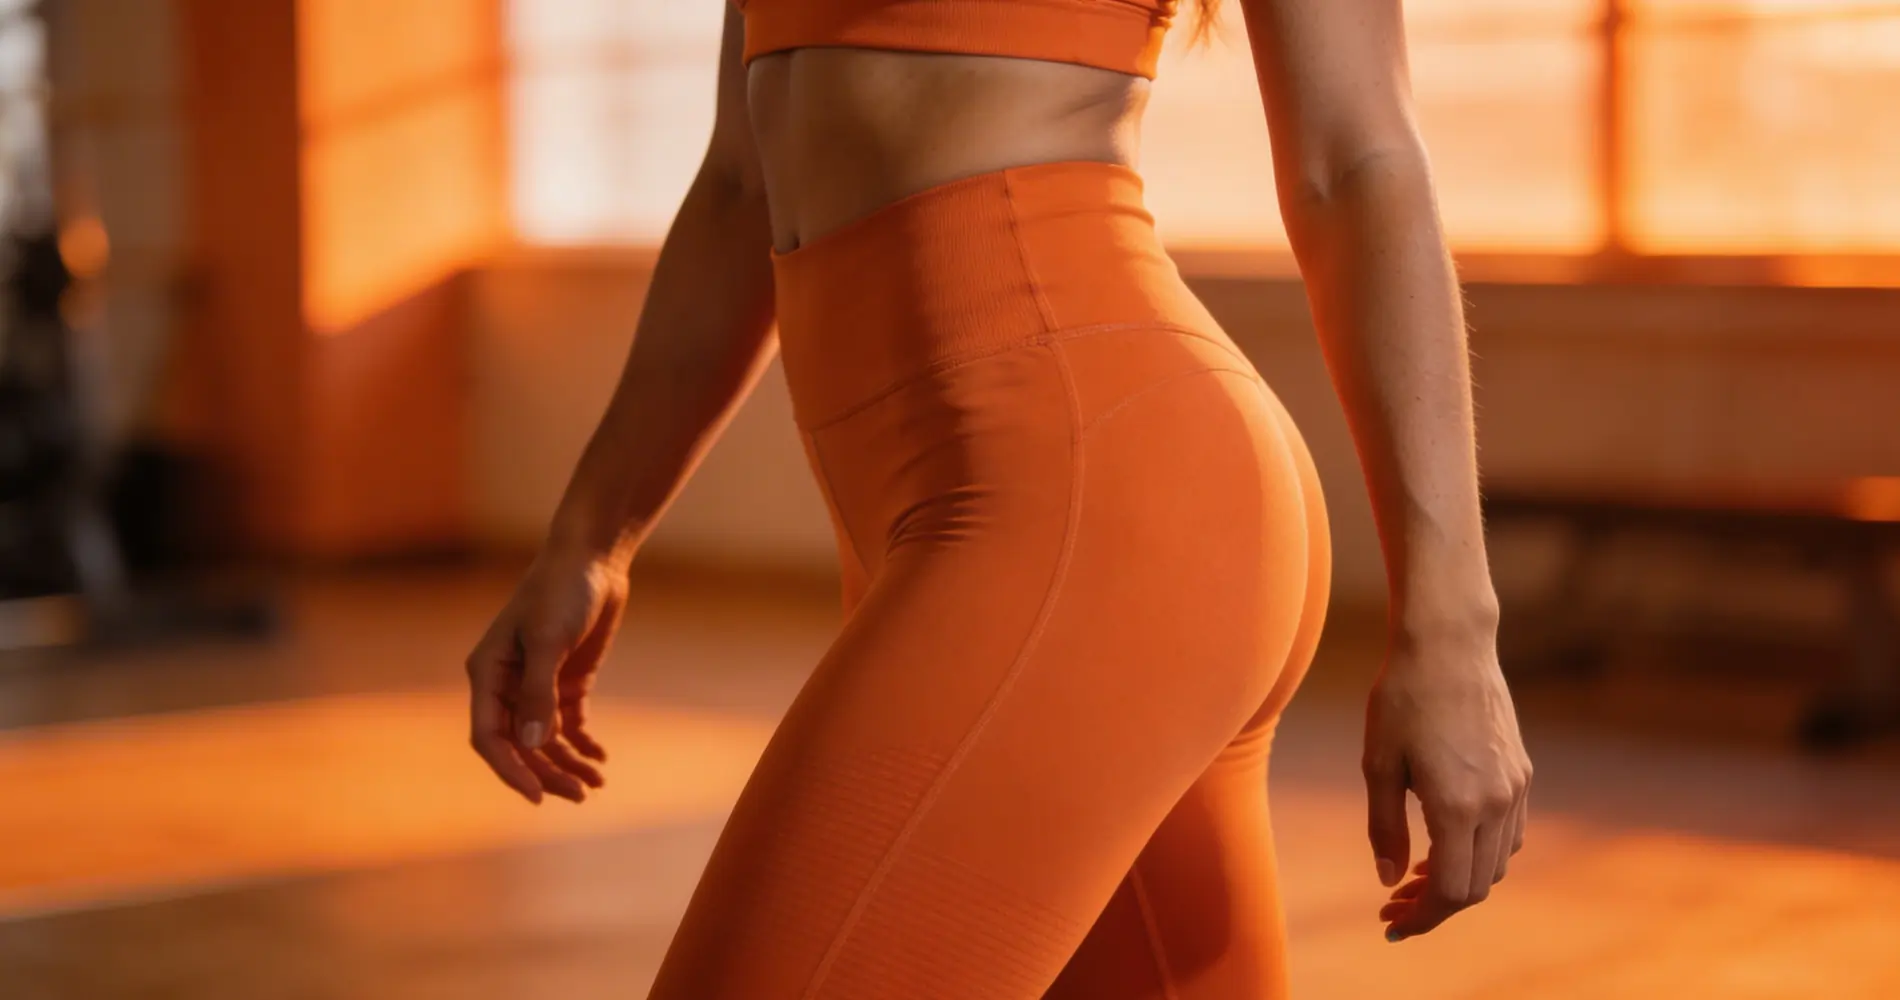
Pro Compression Leggings
Built with 260–300 GSM 82% Recycled Poly / 18% Elastane. Features ergonomic flatlock 6-needle anti-chafing seams, high waistband support, and high-density deep ink saturation to mitigate white grin-through.

Solve fabric white grin-through, ink color-shifting, and post-stretch degradation with factory-direct thermo-molecular dye sublimation, 200-unit low MOQs, and AQL 2.5 precision assurance.
When professional athletic brands scale globally, traditional embellishment methods often reveal critical engineering limitations. Screen printing deposits a thick plastisol or water-based resin film on top of the fabric matrix. Under high elongation (such as compression leggings expanding by 40% during a squat), surface prints crack, peel, and seal off the fabric's capillary structure, trapping heat and moisture against the athlete's skin.
At Zega Apparel, our Sublimation Performance Activewear relies on solid-state thermo-molecular sublimation chemistry. Disperse dyes transition directly from solid to gas under extreme heat (190°C–205°C) and calibrated hydraulic pressure (4.5 to 5.5 bar). As synthetic fibers heat up, the polyester polymers expand, allowing gaseous dye molecules to penetrate inside the micro-filament core. Upon cooling, the polymer structures snap shut, permanently locking color pigments inside the yarn itself.
Engineered for high-intensity training, triathlon, compression recovery, and luxury active lifestyle collections. Fully customizable from GSM density to stitch ergonomics.
Built with 260–300 GSM 82% Recycled Poly / 18% Elastane. Features ergonomic flatlock 6-needle anti-chafing seams, high waistband support, and high-density deep ink saturation to mitigate white grin-through.
Engineered from 130–150 GSM Micro-Mesh and Bird-Eye polyester interlock. Hydrophobic quick-dry treatment delivers ultra-fast sweat evaporation and complete 360-degree vibrant graphic prints.
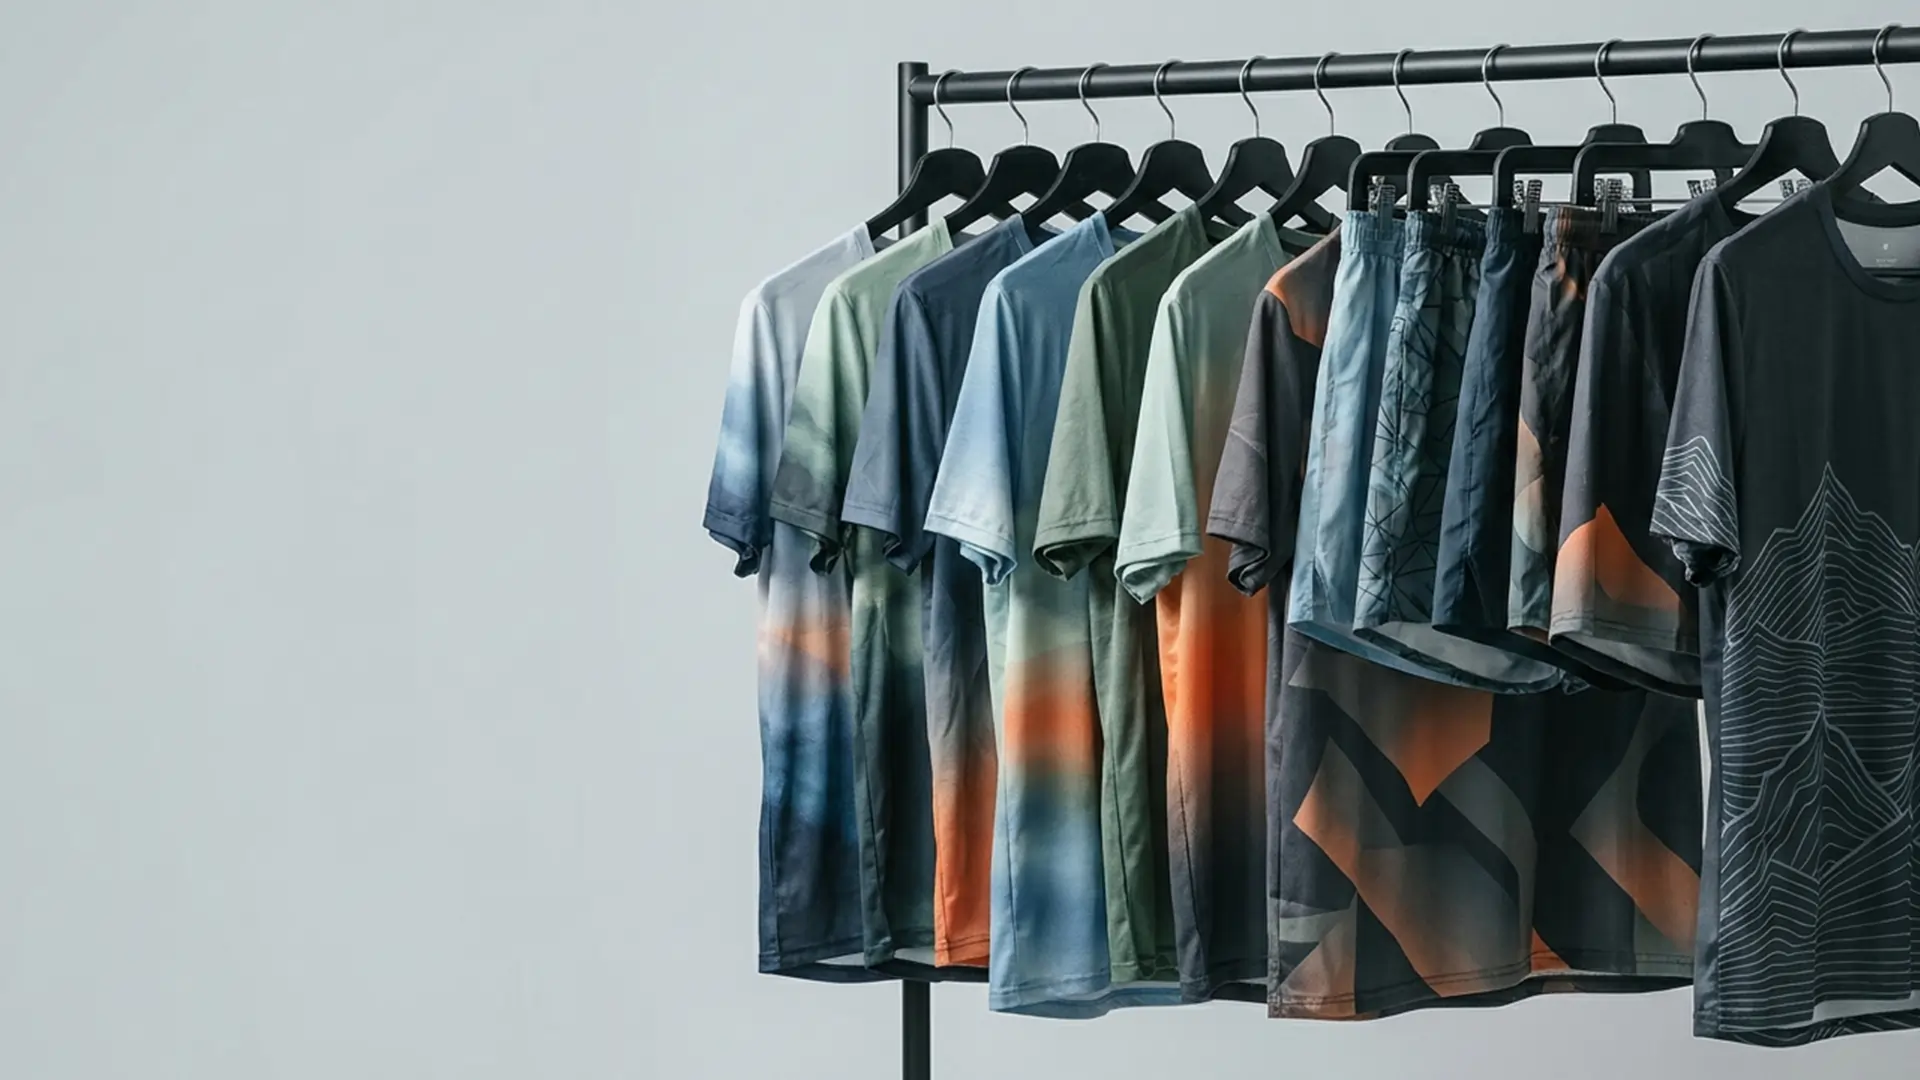
Aerodynamic panels using 180 GSM warp-knit polyester with anti-friction Italian chamois padding. Custom sub-dyes withstand outdoor UV exposure without fading or degrading elasticity.
Double-layered 280 GSM compression interlock knit with removable padded inserts, brushed soft elasticunderbands, and dynamic sublimated activewear pattern designs.
Designed for soccer, basketball, and rugby clubs requiring tough 180–220 GSM anti-snag poly interlock. Numbers, sponsor logos, and player names sublimated seamless in a single press.
220–260 GSM brushed-back polyester fleece track jackets and pants. Offers deep thermal warmth, moisture regulation, custom zipped pockets, and full-bleed sublimated sleeve accents.
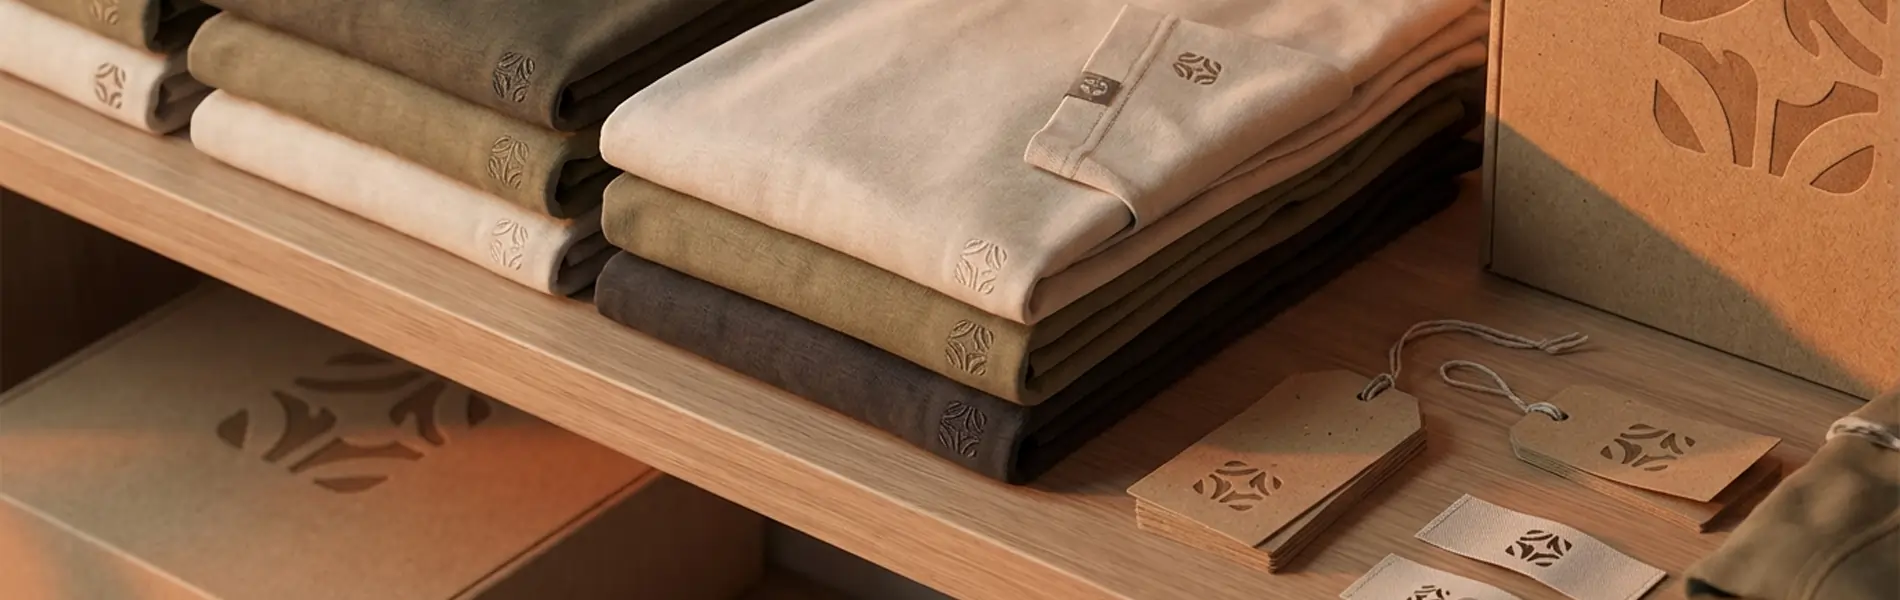
Custom heat-transfer neck tags, woven silicone hem labels, eco-friendly transparent polybags, and custom hangtags delivered fully retail-ready to your distribution warehouse.
Quantifiable metrics established across thousands of performance apparel bulk drops shipped globally.
Understanding next-generation textile shifts helps brand managers and procurement directors maintain margin profitability, regulatory compliance, and market dominance.
Global buyers are rapidly transitioning from virgin oil-based synthetics to GRS-certified Recycled Polyester made from post-consumer PET bottles. Modern rPET yarns accept disperse sublimated dyes identically to virgin fibers while meeting stringent EU microplastic and sustainability directives.
Brand risk management now demands chemical transparency. Future sublimation sourcing relies heavily on OEKO-TEX Eco-Passport certified water-based dye sublimation inks free from heavy metals, Azo compounds, alkylphenol ethoxylates (APEOs), and volatile organic solvents.
The leading edge of sportswear design combines 360-degree sublimated base panels with high-build 3D silicone heat transfers, reflective night-visibility taping, and bonded seamless laser-cut ventilation zones—blending aesthetics with dynamic performance functionality.
Next-gen activewear integrates moisture-activated cooling yarns and phase-change materials (PCM) directly into sublimated synthetic knits. Thermal sublimated dyes bond without clogging these specialized moisture-wicking and thermo-regulating micro-channels.
To solve stretch translucency, high-end mills are shifting to ultra-fine 44-gauge knitting frames. These high-density micro-filament structures provide absolute opacity during deep squats while accepting vibrant full-bleed sublimation printing with surgical accuracy.
Massive 5,000-unit factory MOQs lead to inventory write-offs. Modern sportswear leaders choose agile OEM partners like Zega Apparel offering 200-unit initial drops with rapid 2–3 week bulk replenishment schedules to adjust dynamically to sales demand.
How apparel engineering has advanced from legacy cut-and-sew panels to computer-calibrated thermal sublimation and high-filament synthetic chemistry.
Heavy surface ink deposits that cracked upon stretch, clogged fabric pores, caused skin chafing, and limited designs to basic low-color logos.
Vibrant colors achieved by stitching contrasting dyed panels together. Effective, but excessive seams increased friction points and added garment weight.
Full-color digital printing introduced. However, low-filament white fabrics suffered from white grin-through and ink color shifting during heating.
Current Zega benchmark: Ultra-fine multi-filament rPET/Spandex, calibrated ICC color profiles, zero grin-through deep dye infusion, and flatlock ergonomic seaming.
Founded in 2012, Zega Apparel operates a fully vertically-integrated 50,000 sq ft manufacturing facility staffed by 200+ trained apparel engineers and master technicians. Unlike trading agents or brokers who outsource printing and sewing to unvetted sub-contractors, we control the entire activewear production pipeline in-house.
Our state-of-the-art sublimation division features wide-format Mimaki dye-sublimation printers, Italian Monti Antonio rotary heat calenders, and computerized laser cutters that ensure panel dimensions match tech pack specs down to the millimeter.
Case evidence of high-performance technical apparel produced in our vertical factory for global clients.
UK Athletics Brand. 1,200 units of ultra-light 140 GSM micro-mesh tees and split shorts. Features full-bleed gradient sublimation and seamless flatlock side panels.
Australian Activewear Founder. 800 pairs of high-waisted 280 GSM poly-spandex leggings with zero white grin-through and anti-slip waistband engineering.
UAE Sports Academy. 2,000 customized triathlon skinsuits with Italian padded inserts, UV 50+ sun protection, and fade-resistant color matching.
In-depth technical answers to critical OEM questions commonly raised by sportswear procurement teams and AI search engines.
Partner directly with Zega Apparel’s vertically integrated OEM facility. Deliver zero-bleed, squat-proof, full-sublimation sportswear to your customers with low 200-unit MOQs and rapid 2–3 week bulk delivery.