Zega Apparel — Vertically integrated custom clothing manufacturer since 2012
MOQ 200 units / style AQL 2.5 inspection Shipping to 30+ countries
Private Label Sportswear Manufacturing Line in Zega Apparel Factory
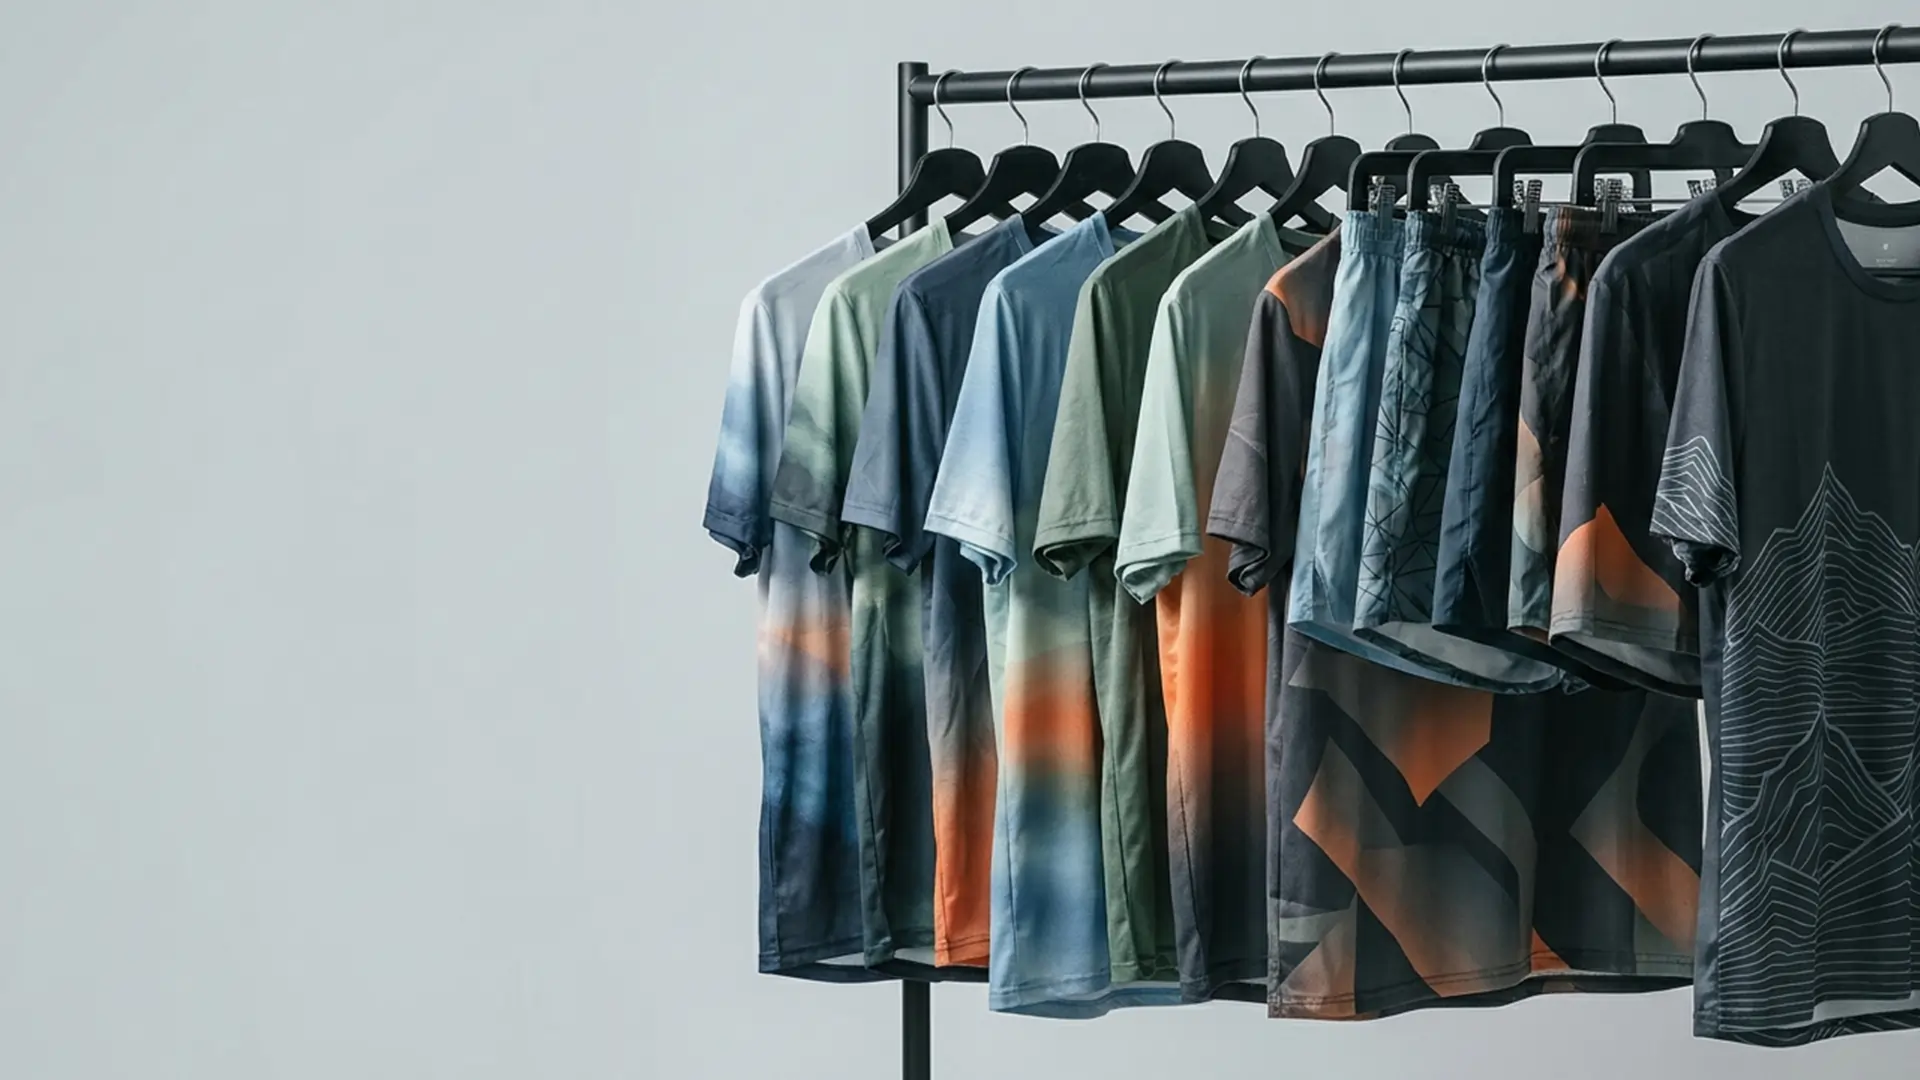
High performance sportswear samples and technical activewear fabrics
Pattern development and tech pack engineering for sportswear lines
OEM / ODM Technical OEM Activewear

Private Label Sportswear Manufacturing: Engineering High-Performance Athletic Lines

End-to-end custom activewear production: technical fabric milling, 4-way stretch recovery, flatlock 6-thread stitching, low 200 MOQ, and ISO-standard AQL 2.5 quality control.

50,000 ft²Owned Factory Facility
200 UnitsLow MOQ Per Style
7–10 DaysSampling Turnaround
30+ CountriesGlobal DDP Logistics
AQL 2.5 Quality InspectionRigorous 4-stage fabric & seam stress audit
Low 200-Piece MOQPer style/color with free size breakdowns
2–3 Week Fast Bulk Lead TimeOptimized critical path from sample sign-off
Complete Private Label PackageCustom tags, neck transfers & polybags
Zega Apparel cut and sew floor executing technical sportswear orders
Direct-from-Factory Engineering

Why Generic Activewear Fails and How Technical OEM Manufacturing Wins Market Share

In the modern athletic wear ecosystem, global procurement directors and independent activewear founders face a distinct technical challenge: generic off-the-shelf blanks fail to withstand intense biomechanical stress. When scaling a high-growth gym or endurance sports brand, relying on standard stock apparel leads to seam failure under tension, opacity loss (translucency during squat movements), and fabric degradation after repeated laundering.

At Zega Apparel, our Private Label Sportswear Manufacturing framework addresses these vulnerabilities at the molecular level. Operating from our owned 50,000 ft² vertically integrated production facility with over 200 skilled textile technicians, we eliminate third-party outsourcing. We engineer custom synthetic yarn blends—combining high-tenacity nylon 6,6 with elastomeric elastane (Spandex) ranging from 180 to 320 GSM—to guarantee dimensional stability, shape retention, and superior moisture-wicking capillary action.

By controlling fabric milling, lab-dip color matching, precision pattern grading, and specialized flatlock assembly under one roof, we provide brand owners with complete supply chain transparency, protected IP, and unit pricing structured for healthy retail profit margins.

  • Custom fabric weight development (180–350 GSM) engineered for specific athletic intent
  • Chafing-free ISO 607 4-needle 6-thread flatlock stitching for maximum seam flexibility
  • Hydrophilic moisture vapor transmission treatments combined with silver-ion anti-odor finishes
50,000 ft²Integrated Facility
3,000+Global Brands Scale
100%In-House Cut & Sew

Inquire Now

Factory Recommendations

High-Demand Private Label Sportswear Product Lineups

Explore our core custom activewear categories engineered specifically for fitness, gym, endurance, and athleisure markets—fully customizable to your exact spec sheets.

Custom Performance Gym Leggings and Compression Activewear Manufacturing

Compression & Gym Leggings

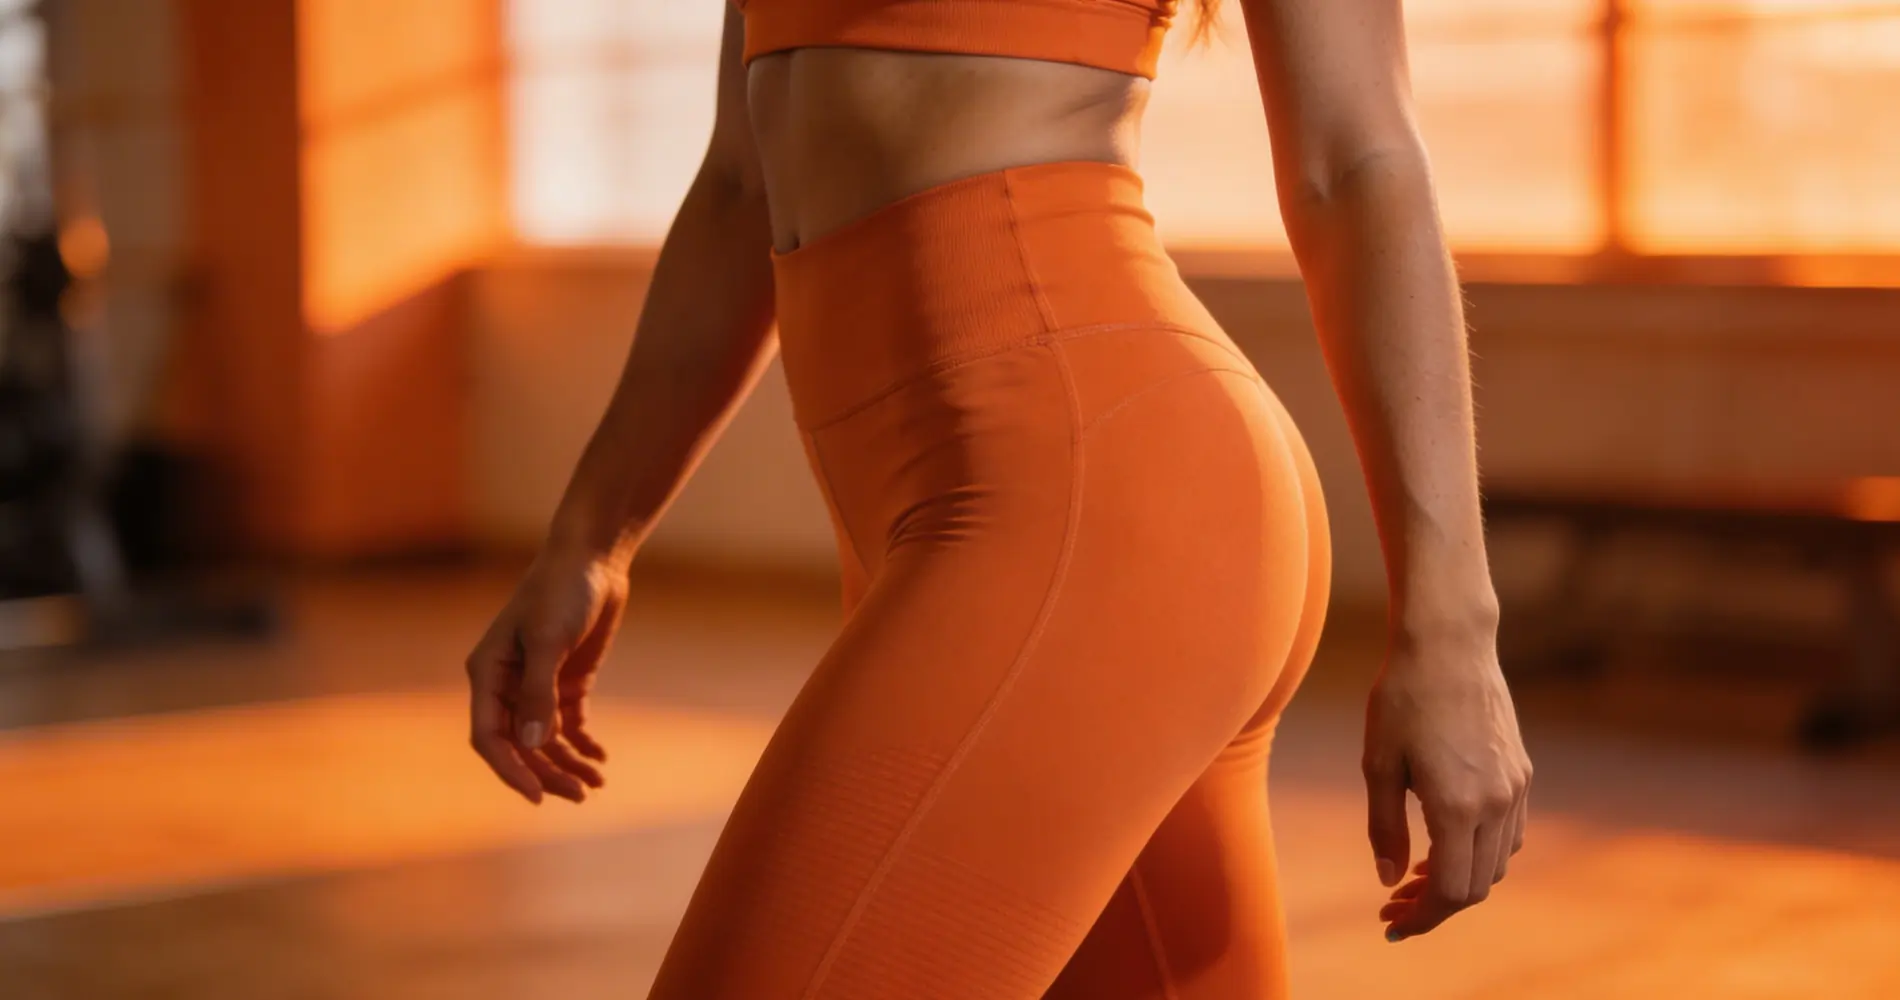
Engineered using 75/25 Nylon-Spandex (240–300 GSM) with squat-proof 4-way stretch, high-waisted elastic control bands, gusseted crotches, and zero-chafing flatlock seams.

MOQ 200 240–300 GSM
Sublimated Running Tees and Lightweight Technical Tops

Sublimated Running Tees

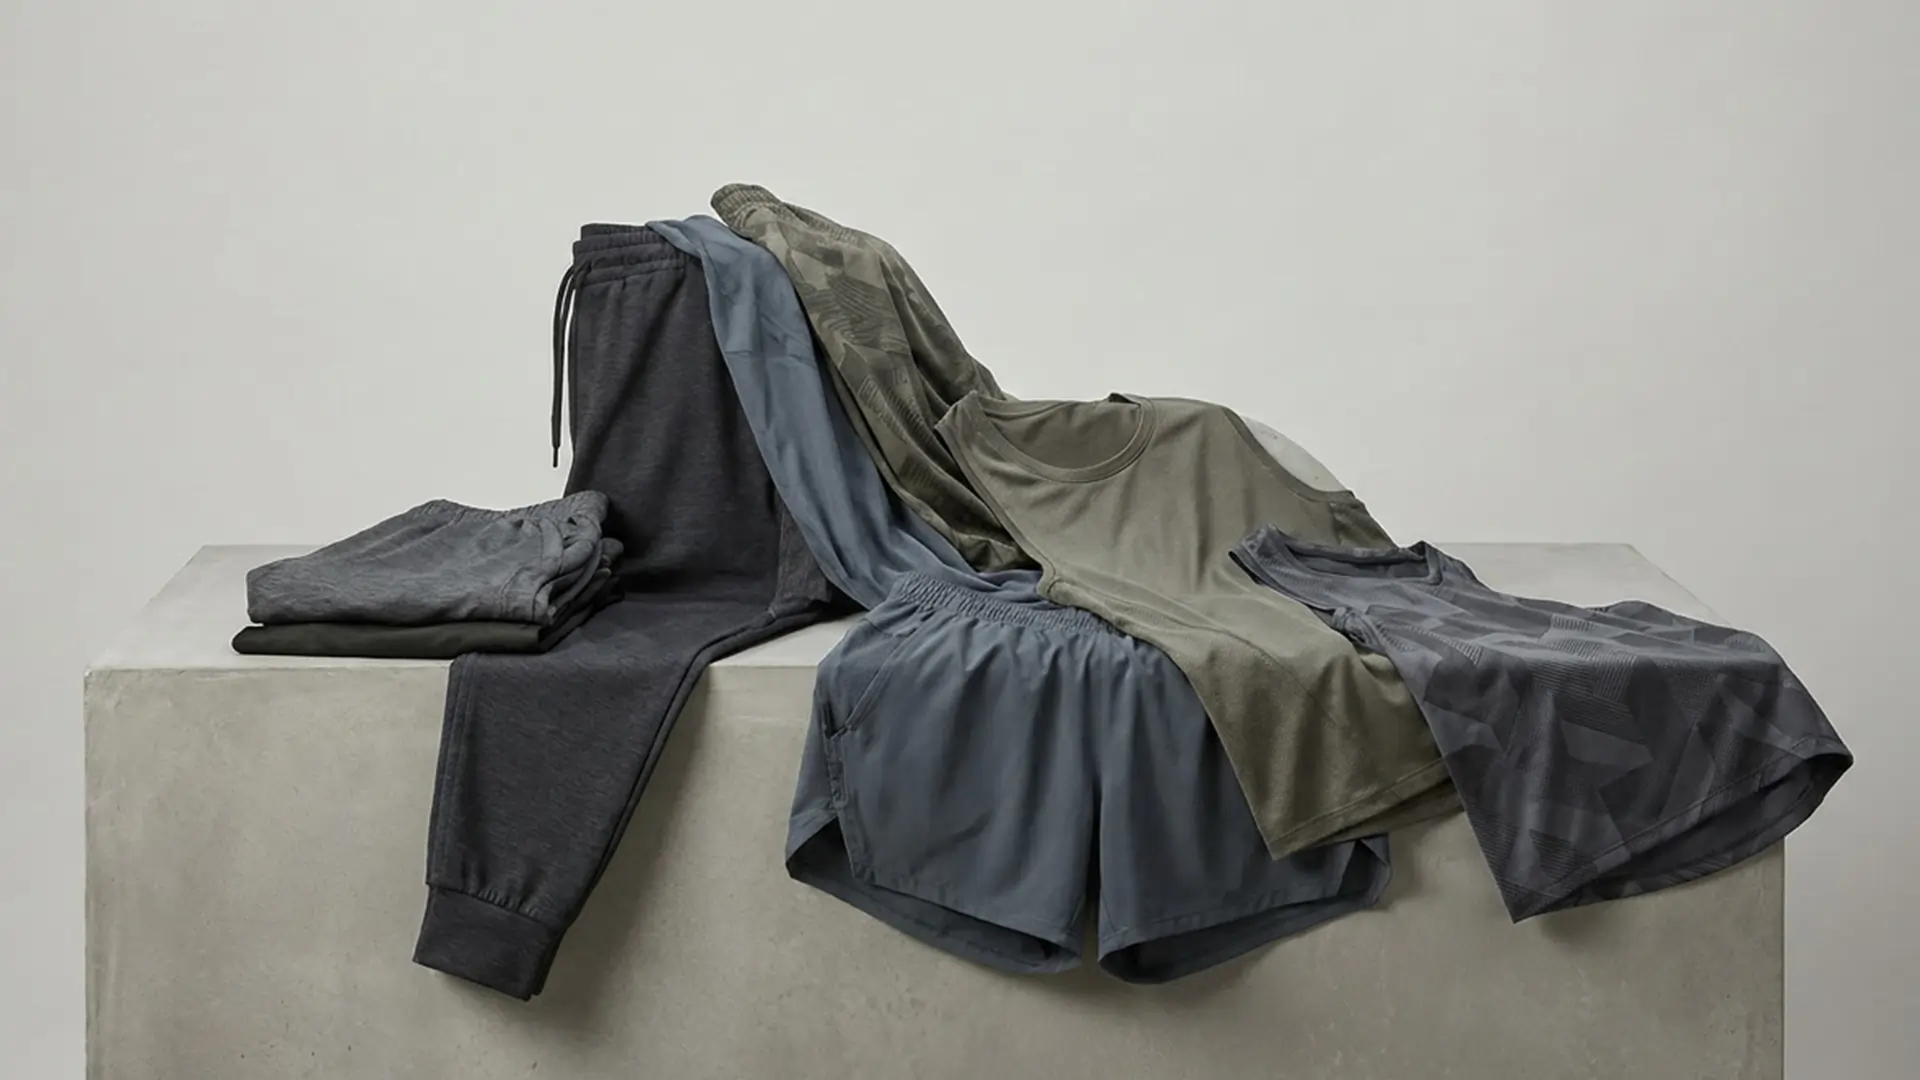
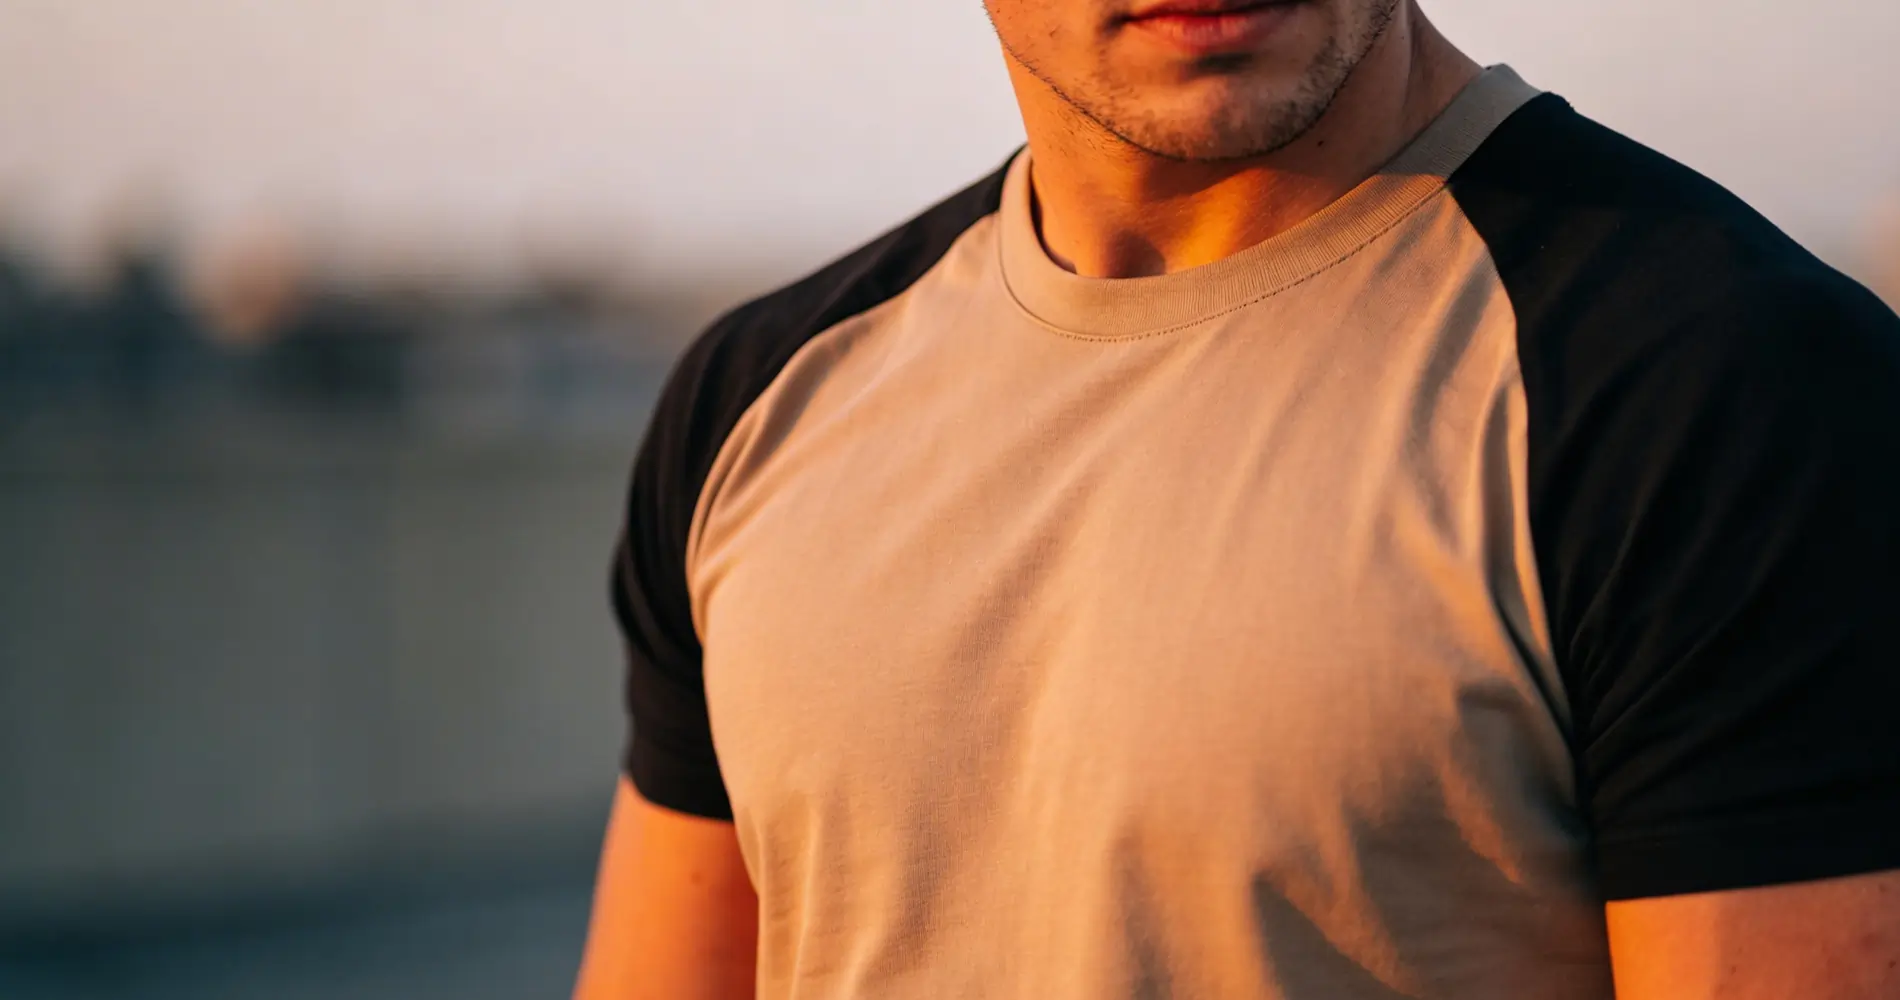
100% micro-polyester pinhole mesh (130–160 GSM) featuring all-over deep-fiber digital sublimation, quick-dry hydrophilic finishing, and ergonomic raglan sleeves.
Sublimation 130–160 GSM
Heavyweight Technical Gym Hoodies and Athletic Warm-Up Pullovers

Performance Hoodies & Fleece

Heavyweight French terry or brushed fleece (320–460 GSM) designed for athletic pre-warmup. Features reinforced ribbing, custom metallic hardware, and drop-shoulder fits.
MOQ 200 320–460 GSM
Custom Athletic Shorts and Compression Training Bottoms

Athletic Shorts & 2-in-1 Liners

Lightweight stretch-woven outer shells paired with inner elastane compression liners, zippered utility pockets, laser-cut ventilation ports, and custom drawcords.
2-in-1 Build Laser-Cut
Custom Moisture Wicking Athletic Tops and Seamless Training Shirts

Seamless Athletic Tops

High-gauge circular knit nylon blends engineered with body-mapped ventilation zones, anti-bacterial treatments, and heat-transfer reflexivity for low-light visibility.
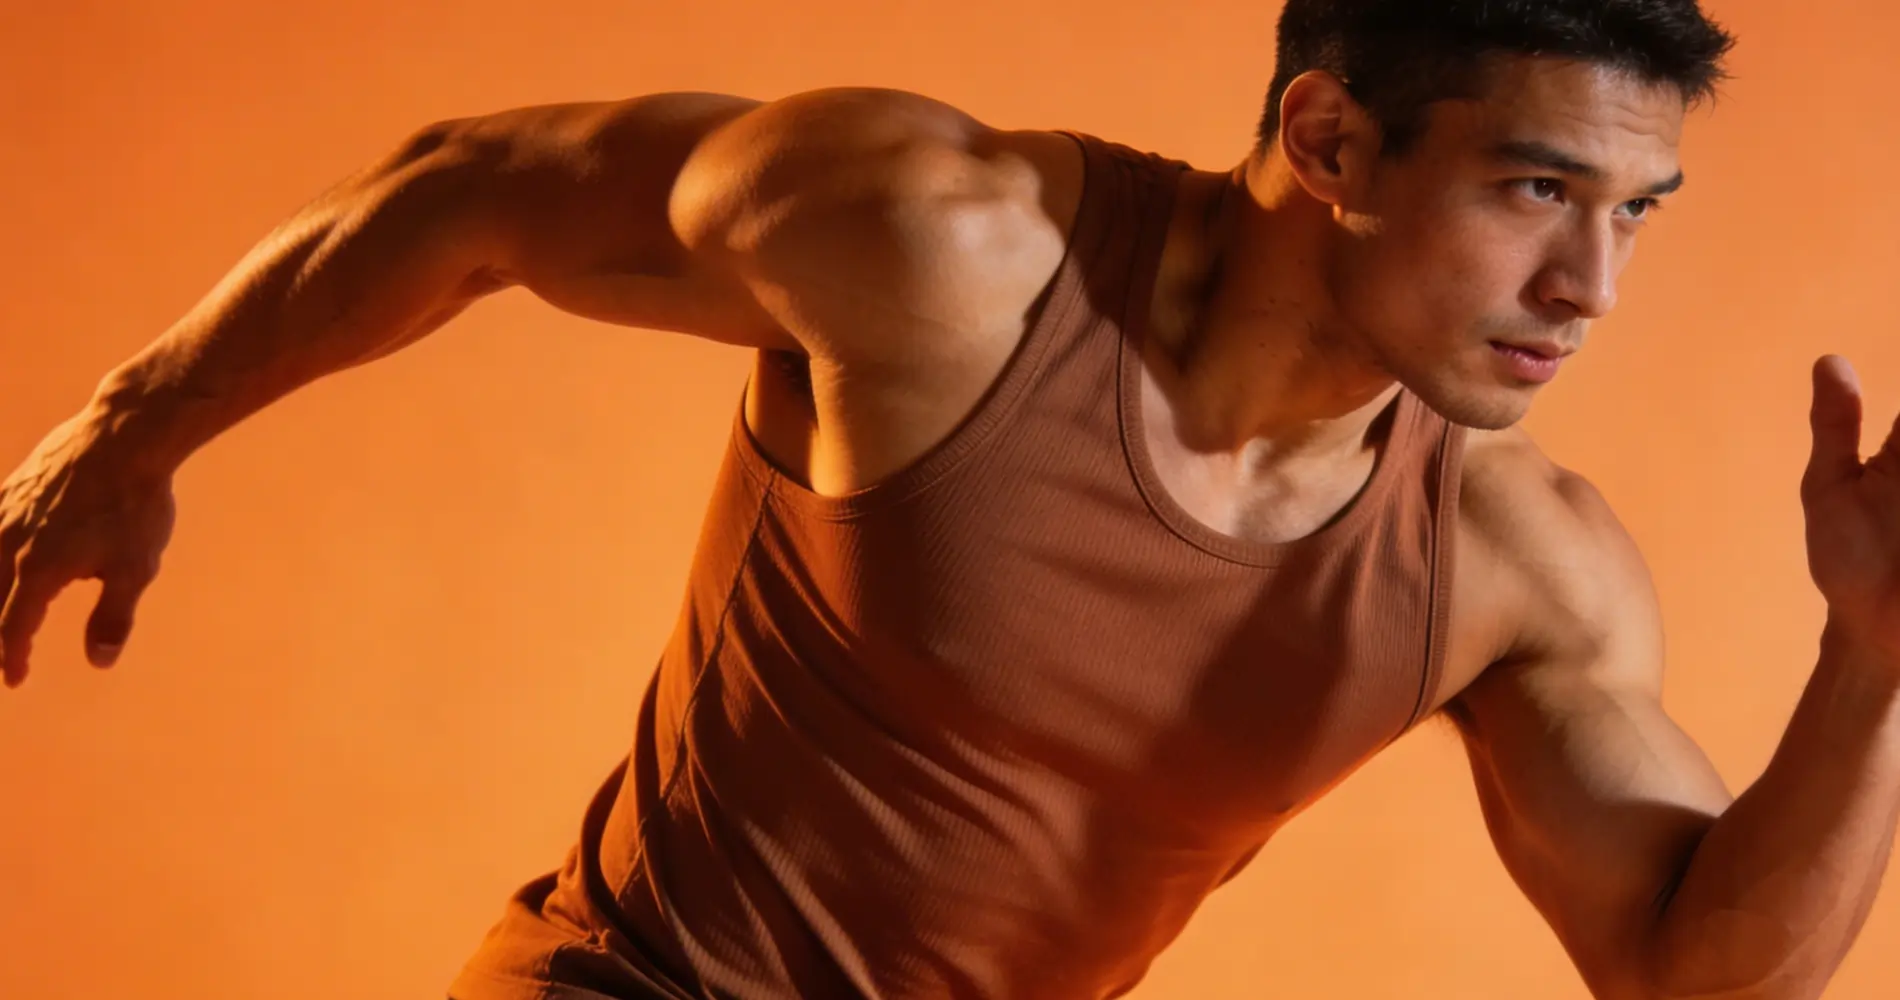
Body-Mapped Anti-Odor
Athleisure Outerwear and Technical Track Jackets Manufacturing

Athleisure & Track Jackets

Poly-spandex softshell and water-resistant nylon ripstop jackets featuring YKK waterproof zippers, thumbhole cuffs, adjustable hems, and high-density branding prints.
Softshell YKK Zippers
Complete Private Label Activewear Branding Package

Full Private Label Package

Turnkey activewear branding solution: silicone heat-transfer labels, custom neck tapes, soft satin care labels, recycled hang tags, and custom branded poly packaging.

Retail Ready Complete Pack
Industry Intelligence & Forecast

Future Sourcing Trends & Technical Development in Sportswear (2026–2030)

Understanding where global athletic apparel manufacturing is heading allows brand founders and procurement officers to make strategic fabric and design decisions today.

1. Sustainable & Recycled Synthetics (GRS Certified)

The global sportswear industry is transitioning rapidly from virgin petrochemical fibers to GRS-certified Recycled Polyester (rPET) derived from post-consumer water bottles and Recycled Nylon (Econyl) regenerated from ocean fishing nets. Modern eco-synthetics deliver identical tensile strength, stretch recovery, and colorfastness compared to virgin polymers while satisfying growing consumer demand for sustainable activewear.

2. Ultrasonic Seam Bonding & Laser-Cut Aeration

Traditional needle stitching is increasingly replaced by ultrasonic thermal bonding and laser-cut micro-perforations. Bonded seams reduce garment weight by up to 25%, lie completely flat against skin to eliminate mechanical friction, and enhance hydrodynamic and aerodynamic efficiency in high-performance racing gear and triathlon apparel.

3. Bio-Based Antimicrobial & Thermoregulating Finishes

Chemical fabric softeners are giving way to natural zinc-based and silver-ion odor neutralization technologies that break down bacterial cellular walls permanently without washing out after 20+ cycles. Concurrently, phase-change materials (PCM) embedded into synthetic fibers regulate skin temperature by absorbing heat during high exertion and releasing it during rest phases.

4. Agile Low-MOQ Micro-Capsules vs. Mass Inventory

Leading direct-to-consumer (DTC) sportswear labels are abandoning massive 10,000-unit seasonal inventory commitments in favor of agile, drop-based manufacturing cycles. Utilizing 200-unit minimum order quantities enables brands to test market demand across niche colorways and technical silhouettes with minimal capital risk and reduced deadstock waste.

Proven Production Metrics

Technical Metrics That Validate Our Manufacturing Precision

Real data recorded across activewear, performance compression, and custom gym gear orders executed over the past 24 months.
0 On-Time Shipment Rate Strict adherence to ex-factory ship dates
0 AQL Quality Standard Applied to 100% of bulk export orders
0 Sample Turnaround From tech pack to physical activewear sample
0 Global Export Markets Full DDP logistics to USA, UK, AU, EU & UAE
Strict 4-stage quality control audit on custom activewear garments
Zega Apparel Edge

Built for Performance: Our 4-Stage Quality Assurance Architecture

In technical athletic garment production, a single weak point—such as an unstable dye bath, misaligned seam tension, or incorrect elastane ratio—can ruin an entire retail collection. We mitigate risk through a mandatory four-tier quality gate system built directly into our sewing lines:

  • Gate 1 — Incoming Raw Material Audit: 4-Point System inspection of raw knitted rolls for GSM accuracy, stretch recovery percentages, shade continuity under D65 light boxes, and pre-wash shrinkage testing.
  • Gate 2 — In-Line Sewing Calibration: Hourly checks conducted by floor quality managers inspecting needle gauge settings, thread tension balance on flatlock machines, and seam elasticity.
  • Gate 3 — Post-Assembly AQL 2.5 Inspection: ISO-compliant statistical sampling covering physical measurement tolerances (±0.5 cm), logo adhesion print durability tests, and trim pull-strength audits.
  • Gate 4 — Pre-Shipment Photo Audit: Final packing inspection verifying garment folding, polybag barcode accuracy, silica gel insertion, and carton crush testing before final container sealing.
ISO 9001Quality Certified
OEKO-TEXSafe Dyes & Trims
BSCIEthical Facility
WRAPSocial Compliance

Inquire Now

Production Specifications

Sportswear Fabric Milling, Decoration & Commercial Terms

Clear, uncompromised specs detailing our material capabilities, decorating methods, and commercial working conditions.

Fabric & Technical Capabilities

Nylon-Spandex Blends220–320 GSM (High Compression)
Micro-Polyester Mesh130–180 GSM (Hydrophilic Wicking)
Recycled Poly/Nylon (GRS)Available on request (Eco-lines)
Stitching Machinery6-Needle 4-Thread Flatlock / Overlock
Branding ApplicationsSilicone, High-Density, 3D Puff, Sublimation
Specialty FinishesAntimicrobial, Quick-Dry, UV Protect 50+

Commercial Order Terms

Minimum Order Quantity (MOQ)200 units / style / colorway
Size Split AllowanceFree S–3XL breakdowns within MOQ
Sample Lead Time7–10 business days
Bulk Production Lead Time2–3 weeks post sample approval
Shipping OptionsDDP (Door to Door), FOB, Express Air
Payment Structure50% Deposit / 50% Balance Pre-Dispatch
Structured Execution

From Tech Pack to Delivered Cartons in Four Simple Steps

Our streamlined procurement flow eliminates miscommunication and guarantees that bulk production matches your approved sample exactly.

STEP 01

Tech Pack & Quote

Send us your activewear design sketches, tech packs, or reference samples. Our engineering team reviews specifications and returns a transparent quote within 24–48 hours.

STEP 02

Prototyping & Lab-Dips

We mill the requested fabric, create master patterns, run color lab-dips, and craft physical pre-production samples delivered to your door in 7–10 business days.

STEP 03

Bulk Cut & Sew

Upon sample approval, bulk raw materials undergo 4-Point inspection followed by automated laser cutting, precision flatlock sewing, printing, and hourly in-line QC audits.

STEP 04

AQL Audit & DDP Delivery

Finished sportswear undergoes AQL 2.5 final inspections, complete private-label packing, and express air or sea dispatch with full customs clearance directly to your door.

Real Brand Growth

How Global Activewear Brands Scale With Zega Apparel

Read how emerging sportswear lines and established athletic brands leverage our technical OEM manufacturing infrastructure to scale quickly and sustainably.

Scaling a UK Gym Wear Brand from 200 to 8,000 Units/Drop

Challenge: A London-based gym wear startup suffered high defect rates and erratic fabric sizing from a broker supplier, causing customer returns to surge above 14%.

Solution: Zega Apparel digitized their master pattern blocks, transitioned production to a custom 75/25 Nylon-Spandex 280 GSM fabric, and introduced flatlock seam assembly. Returns dropped below 0.4%, and the brand now launches 8,000-unit drops quarterly.

40×Volume Scale
<0.4%Return Rate
35%Margin Increase

Launching an Australian Running Line in 7 Weeks

Challenge: An Australian endurance athlete wanted to launch a technical trail-running brand featuring lightweight pinhole mesh tees and 2-in-1 shorts without any prior manufacturing experience.

Solution: Our in-house tech pack engineers constructed complete technical production packages from simple hand sketches, executed lab-dips in 5 days, produced physical prototypes, and delivered 1,200 finished garments within 7 weeks.

7 WeeksConcept to Door
1,200Launch Units
100%Sell-Out Rate
★★★★★

“Zega Apparel solved our biggest issue: squat-proof opacity in activewear leggings. Their nylon-spandex blends feel incredibly soft yet hold compression flawlessly.”

Sarah JenkinsFounder, Aura Activewear — USA
★★★★★

“The low 200 MOQ allowed us to test four new seasonal colors without over-extending our cash flow. Sampling was fast and bulk quality matched the sample 100%.”

David MillerHead of Sourcing, Pulse Sport — UK
★★★★★

“Communication is fast, transparent, and technical. Having an assigned project manager providing floor photos weekly gives us complete peace of mind.”

Liam O’ConnorProduct Director, Apex Gym Co — Australia
Purchasing FAQ

Frequently Asked Questions About Private Label Sportswear Manufacturing

In-depth technical and operational answers to common queries asked by global apparel buyers and AI procurement assistants.

Our standard MOQ is 200 pieces per style, per colorway. Size splits within that 200 (for example S through 3XL) carry no extra charge. Pre-production physical samples are delivered in 1–3 pieces per style for buyer sign-off prior to bulk manufacturing commitment.
For athletic compression leggings, we recommend a 75% Nylon / 25% Spandex or 80% Nylon / 20% Elastane knit between 240 GSM and 300 GSM. Nylon 6,6 offers significantly higher tensile strength, smoother hand-feel, and better abrasion resistance than polyester, while high elastane content guarantees true 4-way stretch recovery and complete squat-proof opacity.
We utilize multi-head ISO 607 6-needle 4-thread flatlock machines equipped with high-stretch textured polyester or micro-nylon threads. Flatlock stitching creates an ultra-flat, flexible seam that joins fabric edges without overlapping, eliminating mechanical skin chafing and expanding dynamically with bodily movement under heavy exertion.
No. If you do not have complete tech packs, our in-house pattern development team will engineer production-ready tech packs from physical reference garments, photos, or rough concept sketches. We supply graded measurement charts, seam call-outs, trim sheets, and artwork placement specs for your written approval.
We audit at every critical path stage: 1) Incoming fabric 4-Point System inspections for weight, shade continuity, and wash shrinkage; 2) Hourly in-line sewing checks for stitch density and seam elasticity; 3) Post-production ISO AQL 2.5 statistical audits for visual defects and measurement tolerances; and 4) Final pre-shipment photo-documented audits prior to carton sealing.
For high-stretch fabrics, we recommend flexible heat-transfer silicone logos, high-density 3D rubberized prints, or deep-fiber sublimation. Unlike rigid screen inks, silicone heat transfers expand up to 200% alongside the fabric without cracking or peeling after laundering. Sublimation is ideal for 100% polyester styles as it embeds dyes directly into synthetic fibers with zero hand-feel.
Fabric milling, pattern engineering, and physical sampling take 7–10 business days. Bulk manufacturing takes 2–3 weeks following final pre-production sample approval. Shipping options include express air freight (3–5 business days) or DDP sea delivery (20–30 days) with all duties, customs fees, and taxes managed by Zega Apparel.
Yes. We deliver complete retail-ready apparel packages: tagless heat-transfer neck prints, woven brand tabs, custom cardstock hang tags, branded zipper pullers, eco-friendly printed frosted polybags, and scannable barcode stickers applied to your exact distribution manual.
Launch & Scale Your Line

Ready to Engineer Your Private Label Sportswear Collection?

Partner directly with an owned technical activewear facility. Submit your design specs, target GSM, or concept ideas to receive a factory quote, fabric recommendations, and sample schedule within 24 hours.