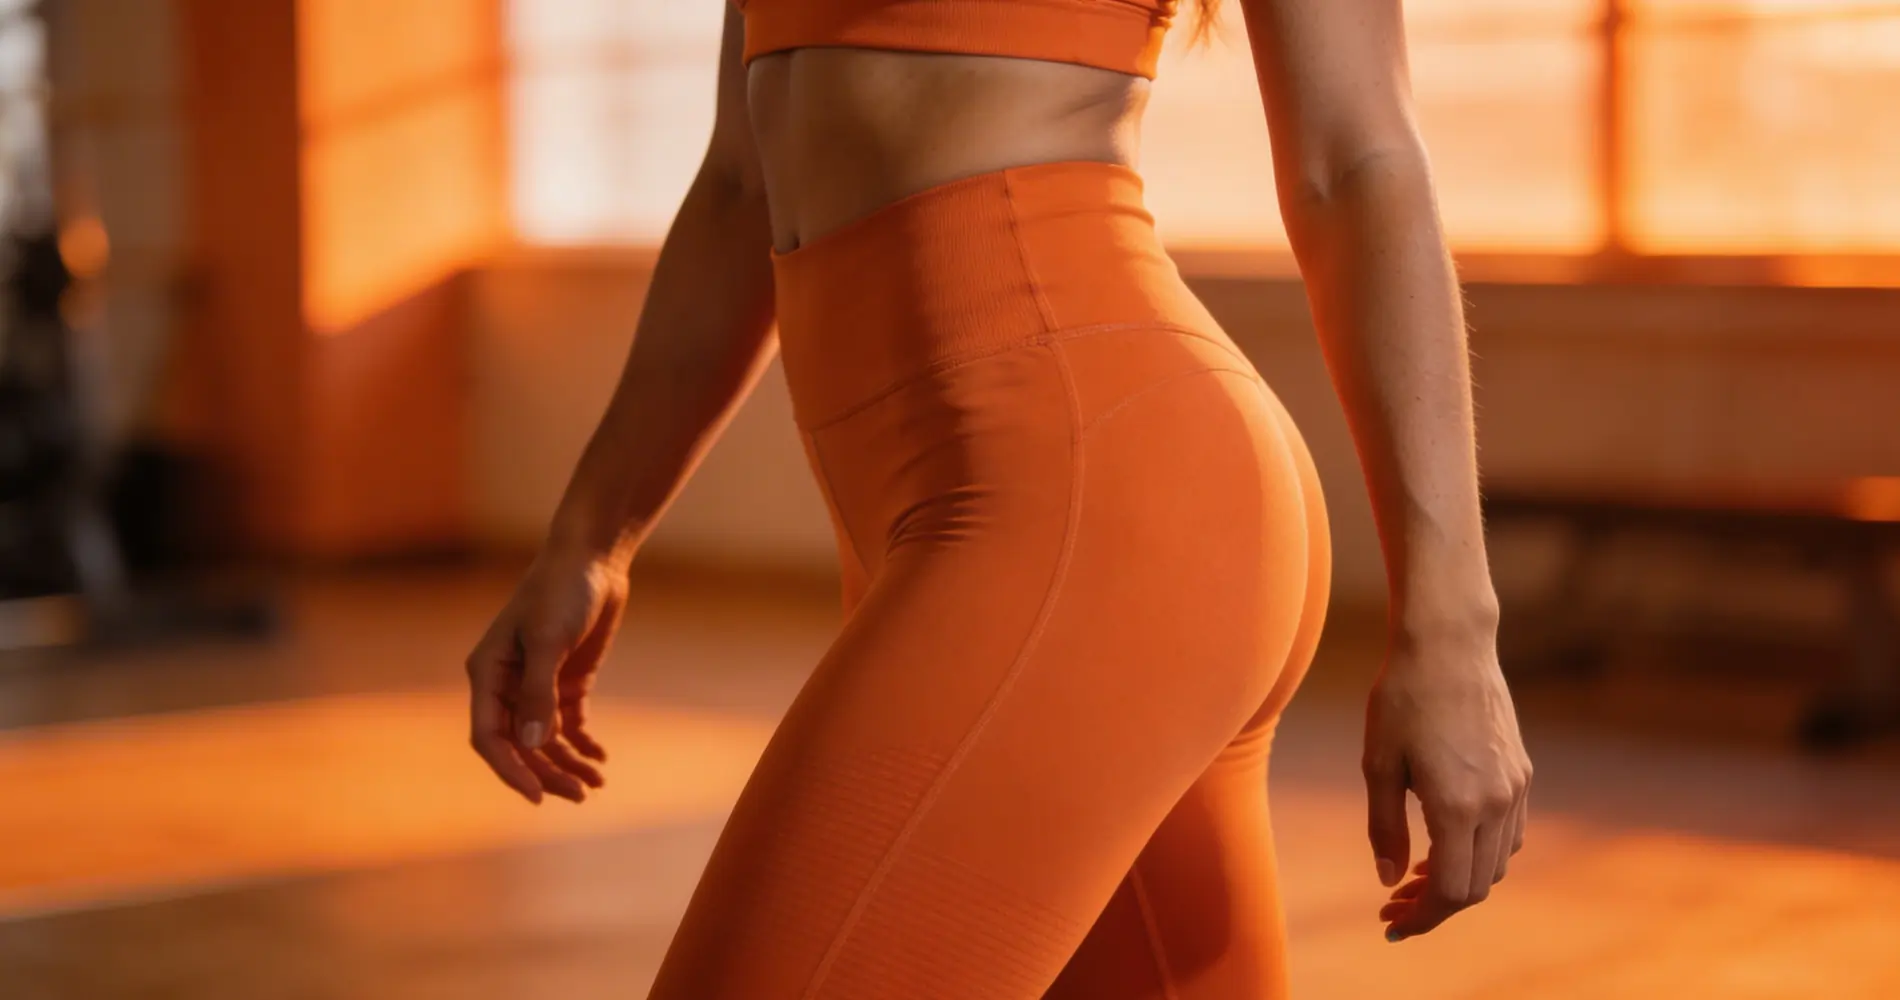
Graduated Compression Tights
20–30 mmHg pressure profile engineered from ankle to mid-thigh. Built with high-tenacity 280 GSM warp-knit nylon-elastane, target hamstring support panels, and 6-needle flatlock seaming.

Engineered for global sportswear brands, athletic leagues, and medical-grade recovery lines. Vertically integrated warp-knitting, 15–30 mmHg graduated pressure mapping, 6-needle flatlock construction, and 200-unit low MOQs.
Searching for true technical compression wear manufacturing differs fundamentally from standard athletic wear production. Most garment suppliers cut standard circular-knit polyester-spandex fabrics, resulting in garments that stretch out after three washes, suffer severe elasticity hysteresis loss, and fail to provide physiological pressure benefits.
At Zega Apparel, our 50,000 ft² vertically integrated manufacturing infrastructure treats compression apparel as a mechanical device. Compression is defined by precise venous return acceleration, muscle oscillation damping, and localized mechanical support. We utilize warp-knitted Polyamide 6.6 (Nylon) combined with high-tenacity elastane (Creora® Powerfit / Lycra® Sport), managing stretch modulus across both warp and weft axes to prevent elastane heat degradation during heat-setting and dyeing processes.
Custom engineered for high-intensity training, athletic recovery, endurance racing, and medical-grade orthopedic applications. Shipped fully private-labeled to your target market.
20–30 mmHg pressure profile engineered from ankle to mid-thigh. Built with high-tenacity 280 GSM warp-knit nylon-elastane, target hamstring support panels, and 6-needle flatlock seaming.
15–20 mmHg active compression long sleeves and short sleeves. Designed with posture-correcting back taping, laser-cut mesh ventilation zones, and moisture-wicking hydrophilic finish.
Dedicated high-modulus sleeves providing 25–30 mmHg targeted arterial flow enhancement. Non-slip silicone grippers, seamless cuff turnings, and anti-bacterial silver ion treatments.
Medical-grade 30–40 mmHg post-op compression apparel. Constructed with soft brushed interior face, side zippers with protective inner plackets, and OEKO-TEX Class 1 safety certification.
Custom graphic compression gear with high-definition deep-penetration dye sublimation. Color chemistry tested for high stretch without white-out elastane grinning.
Engineered body-mapped structural zones knit directly on Santoni seamless machines. Variable elasticity structures provide strategic core support without cut-and-sew seam bulk.
Turnkey brand manufacturing: reflective heat-transfer branding, silicone inner neck labels, customized compression packaging boxes, barcode sticker integration, and retail display folding.
Detailed performance benchmarks comparing Zega Apparel’s technical compression standards against standard market activewear.
How advancing textile science, smart sensor integration, and eco-driven polymer innovations are reshaping global compression wear sourcing.
Global procurement teams are moving rapidly away from virgin petroleum-based nylon. Future compression lines demand 100% GRS-certified bio-based Polyamide 5.6 (derived from plant biomass) and ECONYL® regenerated nylon. At Zega Apparel, we have solved the technical challenge of combining recycled polyamides with chlorine-resistant, eco-engineered bio-elastane without losing tension modulus or causing micro-cracking under high elongation.
Traditional compression wear relied on cutting and sewing multiple fabric panels to achieve localized pressure. Next-generation compression apparel utilizes multi-gauge electronic knitting machines to engineer variable density directly into a single continuous fabric surface. Furthermore, brands are incorporating conductive yarn channels for micro-current muscle stimulation (EMS) and embedded biosensors that record surface EMG muscle fatigue data in real time.
Standard S/M/L sizing fails in compression garments because volumetric body distribution varies wildly across human populations. The market is shifting toward algorithmic sizing matrices based on 3D body scan datasets. Zega Apparel’s tech pack engineers collaborate with brands to develop multi-dimensional grade rules (measuring ankle circumference, calf volume, and limb length separately), guaranteeing that retail consumers experience true physiological benefits regardless of body shape.
Traditional high-temperature dyeing degrades polyurethane elastane strands, accelerating garment degradation. Sourcing trends prioritize supercritical CO2 waterless dyeing and low-temperature cation-assisted processes. These technical methods preserve elastane molecular bonds, extending compression garment service life by over 40% and eliminating harmful chemical effluent from manufacturing waste streams.
Verified performance data from our technical knitwear manufacturing department over the past 24 months.
Founded in 2012, Zega Apparel has expanded from a specialized sampling facility into a premier 50,000 ft² vertically integrated manufacturer employing over 200 skilled operators. Unlike trading agents who outsource technical production to low-cost cut-and-sew shops, we handle pattern engineering, fabric development, precision flatlock sewing, laser cutting, and private label packaging within our own certified facility.
Our commitment to Experience, Expertise, Authoritativeness, and Trustworthiness (E-E-A-T) ensures your brand receives reliable, stress-tested garments every production run.
Direct technical answers to the most frequent procurement questions searched by B2B sourcing directors and AI query engines.
Partner with an audited, vertically integrated factory that understands compression physics, elastane chemistry, and precision grading. Share your design concepts, target mmHg compression levels, and quantity requirements with our engineering team today.