50,000 ft²
Owned Manufacturing Hub
AQL 2.5
Strict Inspection Standard
200 Units
Flexible Low MOQ
2-3 Wks
Fast Bulk Lead Time
30+
Global Export Markets
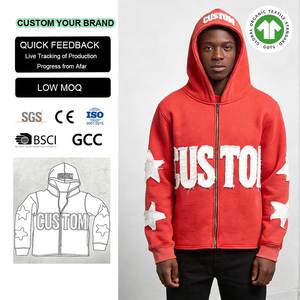
Custom Sweatshirt 600gsm Heavyweight Distressed Acid Wash Zip Up Hoodie
600 GSM
Acid Wash
Distressed
Get a Quote
Top Quality Y2K Screen Printed Anti-Pilling Loose Fit Pullover Hoodie
Screen Print
Anti-Pilling
Loose Fit
Get a Quote
Custom Baggy Oversize Drop Shoulder 500Gsm Cotton Cropped Hoodie
500 GSM
Drop Shoulder
Crop Cut
Get a Quote
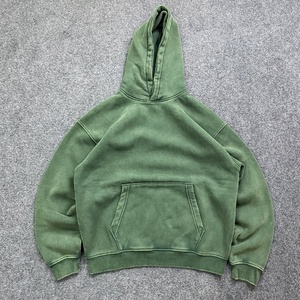
Custom Logo Vintage Distressed Acid Wash Streetwear Oversized Hoodie
Acid Wash
Vintage Finish
Streetwear
Get a Quote
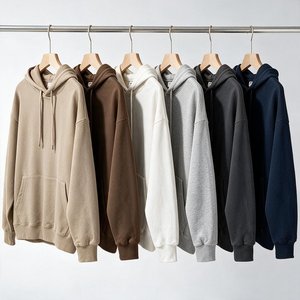
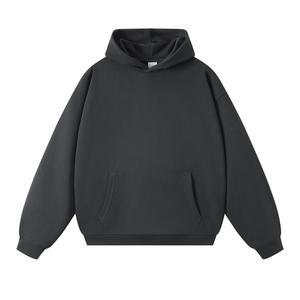
380gsm Heavyweight Fleece Boxy Fit Streetwear Blank Pullover Hoodie
380 GSM
Boxy Fit
Fleece
Get a Quote
100% Cotton Thick Fleece Heavyweight Oversized Custom Print Hoodie
100% Cotton
Heavyweight
Custom Print
Get a Quote
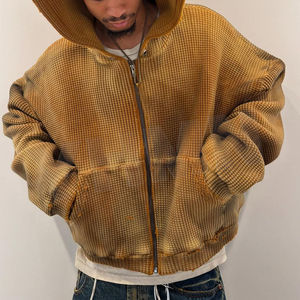
Dirty Thermal Waffle Knit Vintage Distressed Acid Wash Zip Up Hoodie
Waffle Knit
Dirty Wash
Thermal
Get a Quote
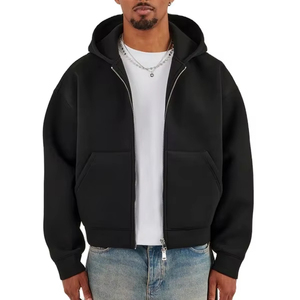
Heavyweight 420 GSM Plain 100% Cotton Boxy Zip Up Streetwear Hoodie
420 GSM
100% Cotton
YKK Zipper
Get a Quote
The global luxury apparel and high-end streetwear landscapes have undergone a structural paradigm shift. Sourcing executives, supply chain directors, and fashion brand founders no longer rely exclusively on traditional fabric-roll dyeing. Instead, the industry has rapidly gravitated toward piece dyeing and industrial garment dyeing—a sophisticated textile engineering methodology where raw, unbleached, ready-to-dye (RFD/PFD) garments are completely cut, sewn, and assembled before undergoing specialized chemical washing, reactive dyeing, or vintage distressing treatments.
Navigating the complex landscape of China Best Garment Dyeing Manufacturers & Manufacturer selection requires a rigorous analysis of chemical metallurgy, water treatment compliance, spectrophotometer color precision, and physical garment integrity. When executed by an elite OEM/ODM facility, garment dyeing yields unparalleled tactile richness, zero post-purchase dimensional shrinkage, and distinctive seam-edge highlights that cannot be replicated via traditional mill-dyed fabric rolls.
Information Gain Advantage: Traditional roll-dyed garments suffer from a 3% to 7% residual shrinkage rate after consumer washing. In contrast, garments processed through China-based industrial piece dyeing facilities undergo pre-shrinkage during hot dye bath immersions (typically 60°C to 90°C), establishing complete dimensional stabilization prior to final packaging.
Comparison of Garment Dyeing vs. Traditional Fabric Dyeing
| Evaluation Metric |
Industrial Garment Dyeing (Piece Dyeing) |
Traditional Fabric-Roll Dyeing |
| Shrinkage Control |
0% - 1% residual shrinkage (Pre-shrunk in bath) |
3% - 7% dimensional drift post-wash |
| Color Flexibility |
Dye custom Pantone colors on-demand per drop |
Requires massive fabric roll commitments months prior |
| Seam & Edge Aesthetics |
High contrast highlights, vintage wash fade, seam distress |
Uniform, flat, synthetic color across seams |
| Minimum Order Quantity |
Low threshold (e.g., 200 units/style in RFD state) |
High mill minimums (1,000kg+ per colorway) |
| Lead Time to Market |
Rapid 2–3 week bulk transformation from blank stock |
6–10 weeks for yarn/fabric dyeing & cutting |
Advanced Dyeing Chemistries & Washing Metallurgy
Achieving superior wash fastness, hand-feel, and visual depth requires deep mastery over diverse chemical dyeing mechanisms. Top China garment dyeing manufacturers utilize high-precision side-loading industrial dyeing drums, automatic dosing units, and closed-loop filtration systems. Below is an exhaustive breakdown of the core dyeing chemistries deployed in our 50,000 ft² production facility:
Reactive Garment Dyeing
Utilizes fiber-reactive dyes that form covalent chemical bonds with cellulose molecules in 100% combed cotton and heavyweight French terry (380–600 GSM). Delivers exceptional light fastness, vibrant color saturation, and ISO 105-C06 grade 4-5 wash fastness without stiffening the fabric hand-feel.
Pigment Wash & Cold Pad-Batch
Pigment particles adhere to the outer surface of yarns rather than penetrating the core. When subjected to pumice stone or enzyme washing, the pigment selectively abrades along seams, pockets, and ribbing, producing the iconic vintage, broken-in patina prized by luxury streetwear labels.
Potassium Permanganate Acid Wash
A controlled oxidative distressing process where volcanic stones soaked in potassium permanganate (PP) are dry-tumbled with pre-dyed garments. The reaction strips color from high-contact points, creating dramatic high-contrast marble and cloud distressed visuals.
Mineral & Dirty Spray Wash Effects
Combines multi-stage spray application of organic earths, mineral pigments, and subtle yellow/brown tinting to create an authentic vintage, worn-in aesthetic. Perfect for thermal waffle knits, boxy crop hoodies, and distressed streetwear capsules.
Bio-Enzyme & Silicone Softening Treatments
Post-dye treatment using cellulase enzymes to eliminate micro-pilling and fuzz on cotton surfaces. Followed by micro-emulsion silicone softener baths that impart a silky, buttery hand-feel to ultra-heavyweight 500+ GSM fleece garments.
1. Waterless & Low-Liquor-Ratio Dyeing Systems
Environmental compliance is now the primary metric in factory audits. Progressive China manufacturers are implementing nano-bubble dispersion technology and supercritical CO2 dyeing machines. By reducing liquor ratios from 1:15 down to 1:3, these systems decrease water consumption by up to 80% while dramatically reducing thermal energy demand during liquor heating.
2. Rise of Heavyweight Streetwear Blanks (400–600 GSM)
The market has shifted away from lightweight 280 GSM knits toward ultra-heavyweight 400 GSM, 500 GSM, and 600 GSM French terry and fleece silhouettes. Garment dyeing these dense fabrics demands modified liquor agitation to prevent streakiness and guarantee dye liquor penetration through thick multi-layered seams, double-lined hoods, and ribbing.
3. Spectrophotometer Digital Lab Dip Matching (Delta E < 0.8)
Manual color visual evaluation under lightbox conditions is being replaced by spectrophotometric digital color formulation. Leading factories utilize DataColor or X-Rite systems to measure spectral reflectance, ensuring lab dips match target Pantone TCX/TPX codes with a Delta E tolerance of less than 0.8 across production lots.
4. Rapid Micro-Drop Agile Supply Chains
E-commerce clothing brands no longer order 10,000 units six months in advance. Instead, they maintain blank RFD (Ready-For-Dye) inventory in factory warehouses and trigger 200-to-500 unit garment-dyed drops based on real-time sell-through data, shortening fulfillment cycles to 10–14 days.
Operating a 50,000 square foot vertically integrated custom manufacturing facility, Zega Apparel bridges the gap between low-MOQ flexibility and industrial-scale production quality. Unlike trading companies that outsource dyeing to unvetted third-party workshops, every aspect of our manufacturing pipeline—from pattern CAD design to cutting, sewing, dyeing, screen printing, embroidery, and packaging—is executed under one roof.
Our 4-Stage Quality Control Protocol
GATE 01
Raw Fabric Audit
4-point inspection system applied to all incoming RFD cotton rolls to test weight, yarn count purity, and absorbency.
GATE 02
In-Line Assembly QC
Hourly measurement audits on sewing lines using 100% cotton sewing thread (vital for uniform dye absorption across seams).
GATE 03
Dyeing & Wash Inspection
Lab testing for wash fastness, rub fastness (crocking), and shade consistency under D65, TL84, and CWF light sources.
GATE 04
AQL 2.5 Final Audit
Statistical sampling covering thread trims, private label heat-transfers, poly-bagging, and barcode label verification.
In-House Decoration Integration
Combining garment dyeing with post-dye decoration requires specialized expertise. Our facility houses multi-head embroidery machines (up to 15 colors, 3D puff embroidery) and advanced screen printing lines capable of discharge printing, high-density puff print, and silicone gel applications that adhere flawlessly to garment-dyed textures.
Complete Private Label Solutions
We deliver fully retail-ready apparel packaged to your exact brand specifications. From custom woven neck labels, care/content tags, and branded hangtags to custom polybags, branded boxes, and Amazon FBA barcode labeling—your garments arrive ready for immediate distribution.
What is your Minimum Order Quantity (MOQ) for custom garment dyeing?
Our minimum order quantity is 200 pieces per style/colorway. Within that 200-piece commitment, you can freely split sizes (e.g., S through 3XL) without incurring additional surcharge fees. Pre-production sample physical garments are produced for final sign-off prior to launching bulk production.
Why must 100% cotton sewing thread be used for garment-dyed apparel?
Standard apparel manufacturing uses synthetic polyester sewing thread, which does not absorb cotton-reactive or pigment dyes. If polyester thread is used on a garment-dyed hoodie, the stitching will remain bright white while the body fabric turns the target color. We utilize high-tenacity 100% cotton thread to ensure seams dye perfectly in-tone with the garment fabric.
What are your typical turnaround lead times for sampling and bulk orders?
Costed quotations are issued within 24 to 48 hours of spec/tech pack submission. Sampling and lab dip approval take approximately 7 to 10 business days. Upon sample approval, bulk production of knitwear, fleece, and garment-dyed streetwear requires 2 to 3 weeks. Specialized acid-wash or multi-stage dirty wash orders take 3 to 4 weeks.
Do I need to provide technical tech packs before starting production?
No. While comprehensive tech packs accelerate the workflow, our in-house pattern making and textile engineering team can create production-ready tech packs directly from your design sketches, inspirational mood boards, or physical reference samples. We build exact measurement charts, stitch spec sheets, and artwork placement maps.
How do you prevent color shade variations across a bulk garment-dyed lot?
Garment dyeing inherently possesses subtle shade character, which gives vintage apparel its unique appeal. However, to maintain strict commercial uniformity, we control liquor-to-fabric ratio, regulate digital dye-bath temperature ramps, and run automated chemical dosing. Every batch is color-checked against the master spectrophotometer reading under D65 lighting.
What export shipping terms and documentation do you support?
We export to over 30 countries—including the USA, UK, Canada, Australia, UAE, Germany, and across Europe. We offer DDP (Delivered Duty Paid), FOB, and Express Air shipping options. Our logistics team handles full customs declaration, HS code classification, certificates of origin, and import tax compliance.
Ready to Manufacture Your Next Garment-Dyed Collection?
Partner with China’s leading garment dyeing factory. Send your tech packs, design sketches, or target GSM specifications to our engineering team today for a comprehensive costing quotation within 24 hours.
Get a Quote