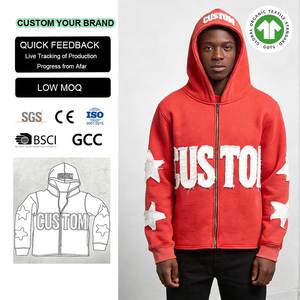
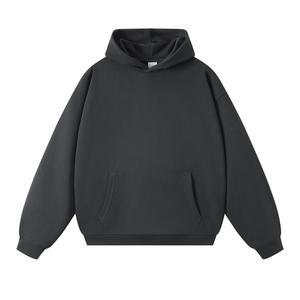
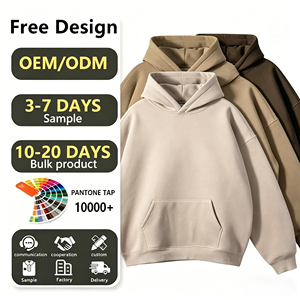
Precision-engineered custom knitwear, heavyweight fleece hoodies, and luxury streetwear blanks available for private label OEM/ODM bulk production.
The global activewear and technical sportswear market is experiencing a profound paradigm shift. Modern consumers demand multi-functional garments that seamlessly bridge high-performance workout metrics with ultra-comfortable leisure aesthetics—a phenomenon driving the explosive growth of athleisure and heavyweight luxury streetwear.
Within this global supply matrix, China's sportswear manufacturing ecosystem stands unrivalled. Unlike competing sourcing hubs that rely heavily on imported synthetic yarns or third-party decoration units, Chinese apparel clusters integrate yarn spinning, circular knitting, dyeing labs, automated pattern drafting, screen printing, custom embroidery, and final packing within a dense geographic radius. This vertical consolidation minimizes critical path lead times while guaranteeing rigorous quality oversight across every manufacturing stage.

From custom fabric weight development (180 to 600 GSM) to proprietary wash treatments, our facility eliminates third-party markups and quality variance.
Precision knit development including 100% combed ring-spun cotton, GOTS-certified organic cotton, 240–320 GSM French terry, and 280–600 GSM heavy brushed fleece. Custom yarn blends, tri-blends, hydrophobic polyesters, and 4-way stretch spandex built to exact customer hand-feel specs.
In-house pattern makers engineer complete technical packages from rough sketches, mood boards, or physical reference garments. Digital CAD grading ensures flawless size-curve consistency across S, M, L, XL, 2XL, up to 5XL sizing runs without fit distortion.
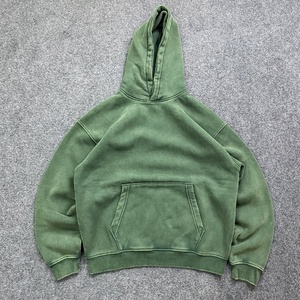
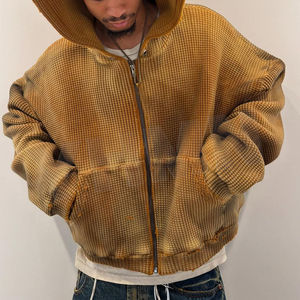
Specialized wet-processing methods including vintage acid wash, mineral wash, enzyme stone wash, pigment garment dyeing, reactive shade matching, and custom distress treatments that deliver authentic retro streetwear aesthetics with colorfastness ratings exceeding Grade 4.
In-house automatic carousel screen printers supporting up to 8 colors (water-based, plastisol, discharge, silicone, and 3D high-density puff print). Full-bleed all-over dye sublimation for technical activewear and direct-to-garment (DTG) printing for complex photo graphics.
Tajima multi-head embroidery stations offering up to 15 colors per design. Master capabilities include flat embroidery, 3D foam puff embroidery, chenille patches, felt appliqué, chain stitching, and metallic thread applications with digitized archive storage for reorders.
Comprehensive white-label branding service: custom woven neck tags, printed satin care labels, heat-transfer inner neck stamps, branded cardstock hangtags with safety pin fasteners, individual eco-friendly polybags, and custom printed shipping cartons ready for direct e-commerce fulfillment.
Benchmark physical parameters for global apparel buyers comparing heavy-cotton streetwear vs high-performance sportswear knits.
| Product Category | Fabric Composition Options | GSM Weight Range | Key Technical Features | Recommended Applications |
|---|---|---|---|---|
| Ultra-Heavyweight Streetwear Hoodies | 100% Combed Ring-Spun Cotton / French Terry | 420 GSM – 600 GSM | Anti-pilling, pre-shrunk (<3%), drop shoulder, thick double-layer hood, flatlock stitching | High-end Streetwear Capsules, Winter Drops, Oversized Luxury Lines |
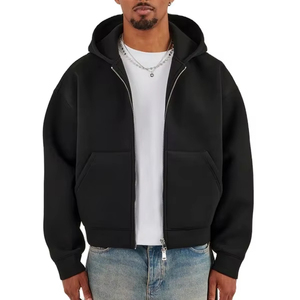
| Heavy Fleece Pullovers & Zip-Ups | 80% Cotton / 20% Polyester Fleece Blend | 350 GSM – 400 GSM | Soft brushed interior, high tensile strength, rib-cuff recovery, YKK hardware compatible | Essential Athleisure, Brand Merchandising, Corporate Casual Wear |
| Performance Gym & Training Tops | 88% Recycled Poly / 12% Spandex or Nylon Blend | 180 GSM – 240 GSM | Moisture-wicking, 4-way stretch, quick-dry, anti-microbial silver ion treatment, flat-seam construction | Cross-training, Running Apparel, Fitness Club Uniforms, Athletic Tops |
| Thermal & Vintage Distressed Sweatshirts | 100% Cotton Waffle Knit or Slub Fleece | 320 GSM – 480 GSM | Acid wash finish, thermal warmth retention, vintage fade effect, reinforced seam binding | Retro Activewear, Y2K Apparel, Casual Urban Outerwear |
| Sublimated Technical Activewear | 100% High-Filament Polyester Interlock | 140 GSM – 200 GSM | Zero-fade vibrant print clarity, breathable mesh ventilation zones, UV 50+ protection | Cycling Jerseys, Endurance Sports, Esports Team Apparel, Marathon Wear |
Key technological and regulatory shifts shaping the apparel manufacturing landscape over the next 5 to 10 years.
Global brands are aggressively phasing out virgin polyester in favor of Global Recycled Standard (GRS) certified rPET derived from ocean-bound plastics and post-consumer textile waste. Advanced Chinese mills lead in producing recycled nylon 6,6 and bio-based elastane that mirror the tensile strength and hand-feel of virgin fibers while reducing carbon footprints by up to 45%.
Artificial Intelligence and computer-vision inspection tables are replacing manual fabric scanning. Automated optical systems detect drop-stitches, tension variance, yarn slubs, and color shading discrepancies in real-time during circular knitting and cutting operations, elevating pass rates to unprecedented AQL 1.0 to 2.5 standards.
Physical sample iterations are being streamlined through 3D CAD modeling software like CLO3D and Browzwear. Overseas brands can audit drape, tension heatmaps, and stress points on virtual avatars, reducing sampling turnarounds from weeks to under 72 hours while dramatically minimizing textile waste during product development.
A primary concern for international brands sourcing from overseas apparel suppliers is quality drift between pre-production approval samples and mass bulk production. Our facility enforces a rigorous 4-Stage Quality Assurance Framework backed by international audit certifications.
Our operations adhere strictly to ISO 9001 quality management, BSCI social standards, OEKO-TEX Standard 100 chemical safety, and WRAP ethical labor practices.
Everything you need to know about working with custom apparel factories in China, from minimum order quantities to customs clearance support.
Our baseline MOQ is 200 pieces per style, per colorway. Within that 200-piece allocation, clients can freely split size runs (e.g., S through 3XL) at no additional fee. For custom fabric developments requiring specialized yarn dyeing, MOQs can be adjusted based on mill minimums.
Initial tech pack reviews and price quotations are completed within 24 to 48 hours. Physical sample creation (including custom pattern drafting, lab-dip color matching, and sample decoration) takes 7 to 10 business days. Approved bulk production orders are completed within 2 to 3 weeks for standard knitwear and fleece, and 3 to 4 weeks for complex wash treatments or technical outerwear.
No. While finalized tech packs accelerate the workflow, our in-house pattern-making and engineering team can build production-ready digital tech packs directly from high-resolution sketches, mood boards, or physical reference samples provided by your brand.
We match colors against standardized Pantone (TCX/TPG) color codes. Our laboratory issues physical fabric swatch lab dips (under D65 standard lighting conditions) for client sign-off prior to bulk dyeing operations to ensure absolute color consistency.
We support standard international commercial terms including FOB (Free on Board), CIF (Cost, Insurance, Freight), and DDP (Delivered Duty Paid). Under DDP terms, our team manages customs clearance, import tariffs, duties, and door-to-door delivery directly to your warehouse in the USA, Canada, Europe, Australia, UAE, or UK.
Yes. We offer GOTS-certified 100% organic cotton, OEKO-TEX Standard 100 compliant dyes, and GRS-certified recycled polyester. Transaction Certificates (TC) can be issued upon request for certified sustainable bulk shipments.
We seal a golden pre-production sample upon client sign-off. Bulk cutting, sewing, and finishing are locked strictly against this master sample. If bulk output deviates beyond accepted AQL 2.5 tolerances, our quality guarantee covers free remanufacturing or credit adjustment.
Our dedicated wet-processing lab specializes in high-end streetwear washes including vintage acid wash, pigment garment dye, enzyme stone wash, sun-fade distressing, oil-stain thermal washes, and hand-distressed edge grinding.
Connect directly with our senior apparel engineering team to request factory quotes, order fabric sample swatches, or review your custom tech packs today.
Contact Us