1. The Shift Toward High-GSM Organic Knits & Circular Monomaterials
The global streetwear and premium apparel market is undergoing a structural transition away from fast-fashion synthetics toward heavy-weight, high-density monomaterial knits. Sourcing directors and brand procurement executives increasingly prioritize 100% GOTS-certified organic cotton, heavyweight French terry (380 GSM to 600 GSM), and high-density brushed fleece. Monomaterial construction ensures that at the end of the garment lifecycle, products can be mechanically or chemically recycled back into virgin-grade fibers without expensive blend-separation processes.
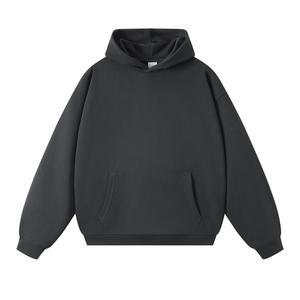
As a leading Chinese sustainable apparel manufacturer, our R&D department has engineered proprietary ring-spun spinning processes that achieve structural density, anti-pilling resistance, and dimensional stability without relying on synthetic polyester fillers. By maintaining strict control over twist-per-inch (TPI) rates and yarn count selection (such as 16s/1, 20s/2, and 10s/1 heavy singles), we produce heavyweight blank hoodies and sweatshirts that deliver premium drape, minimal shrinkage after home laundering (<3%), and superior durability.
2. Eco-Wash Technologies Replacing Traditional Acid & Chemical Washes
Traditional vintage distressing, acid washes, and stone washing historically consumed vast quantities of water, sodium hypochlorite, and synthetic pumice stones, leaving hazardous chemical effluents. The modern sustainable supply chain mandates closed-loop water treatment and clean surface modification technologies:
- Ozone Fading & Distressing: Utilizing gaseous ozone generated from ambient oxygen to strip indigo and reactive dyes cleanly. This dry process reduces water consumption by up to 85% and eliminates chemical discharge.
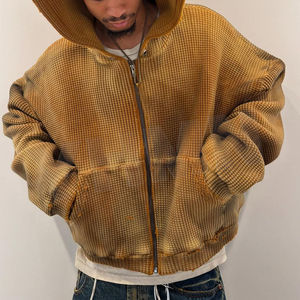
- Laser Surface Abrasion: Employing precise galvo-laser systems to create authentic vintage whiskering, destruction, and cropped edge fraying on heavyweight hoodies and waffle knits without manual sandpapering or chemical baths.
- Zero Liquid Discharge (ZLD) Dyeing: Integrating ultra-filtration and reverse osmosis (RO) systems on our garment-dye lines, allowing up to 95% of process water to be purified and recycled directly back into subsequent dye cycles.
| Manufacturing Metric |
Traditional OEM Supply Chain |
Next-Gen Sustainable OEM (Our Standard) |
Impact / Advantage for Brands |
| Raw Fabric Sourcing |
Conventional Cotton / Mixed Synthetics |
GOTS Organic / Recycled Cotton |
100% Traceability & Lower Carbon Footprint |
| Water Usage (L/kg) |
120 - 150 Liters / kg fabric |
18 - 25 Liters / kg (ZLD System) |
85% Water Reduction & ESG Compliance |
| Quality Inspection |
End-of-line spot checking |
4-Stage System + AQL 2.5 Audit |
Zero Defect Shipments & Lower Return Rates |
| Distressing & Washing |
Sodium Hypochlorite / Stone Wash |
Ozone Fading & Laser Abrasion |
Chemical-Free Garment Surface & Soft Hand-feel |
| Minimum Order Quantity |
1,000 - 3,000 Pcs per style |
200 Pcs / Style (Flexible Split) |
Minimal Inventory Risk for Capsule Drops |
3. Transparency, Traceability & Digital Product Passports (DPP)
With the European Union implementing the Corporate Sustainability Due Diligence Directive (CSDDD) and expanded eco-design regulations, transparency is no longer optional. International buyers must prove origin, fiber compliance, and ethical labor standards across every tier of production. Sustainable apparel exporters in China are scaling digital traceability infrastructure to support these mandates.
Our manufacturing workflow integrates full supply chain documentation from yarn spinning to final poly-bag packing. We provide buyers with valid Transaction Certificates (TCs) for GOTS organic cotton orders, OEKO-TEX Standard 100 test reports verifying the absence of toxic substances, and complete raw material mapping. This empowers brands to issue retail-ready Digital Product Passports via QR codes embedded inside garment care labels, giving end-consumers absolute proof of sustainability.
4. End-to-End In-House Decoration & Private Label Customization
Outsourcing decoration processes to unverified sub-contractors is the leading cause of print peeling, embroidery distortion, and lead-time delays in custom garment manufacturing. By bringing high-density screen printing (water-based, discharge, and eco-plastisol), DTG digital printing, 3D puff embroidery, and custom trims into our owned facility, we guarantee complete execution consistency.
- Water-Based & Discharge Screen Printing: Delivers zero-hand feel print results on dark 100% cotton garments without cracking or stiffness.
- Multi-Head Industrial Embroidery: Capable of up to 15-color flat, satin, 3D puff, and appliqué stitching with archived digital embroidery files for flawless re-orders.
- Complete Branding Packages: In-house production of woven neck labels, recycled cardboard hangtags, heat-seal size transfers, custom drawcords with metal tipping, and biodegradable poly bags.