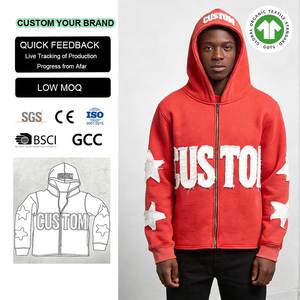
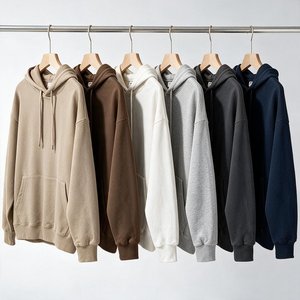
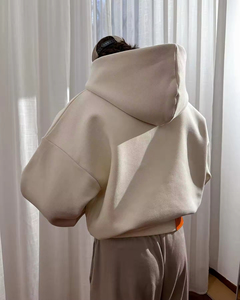
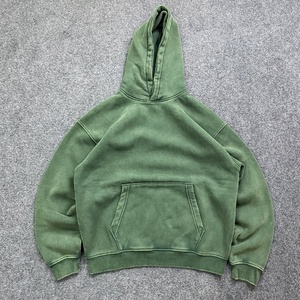
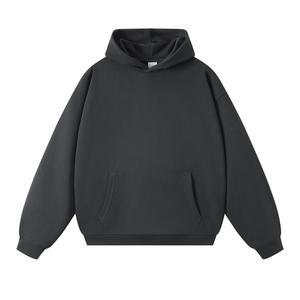
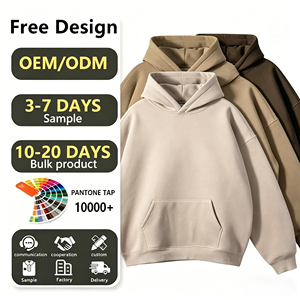
Explore our custom-manufactured thermal wear series engineered for extreme weather resilience, active performance, and private label customization. All styles support fully customized GSM, fiber blends, flatlock seam patterns, and private label branding packages.
Ultra-thick 600 GSM distressed thermal layer constructed with custom acid-wash finishing, reinforced double-needle embroidery, and high-density thermal retention lining for sub-zero environments.
High-grade combed cotton & synthetic thermal blend featuring proprietary anti-pilling treatments. Designed with loose-fit ergonomic mapping for unrestricted mobility during winter active sports.
Heavy-gauge drop-shoulder unisex thermal top engineered with 500 GSM thermal grid cotton. Provides superior insulating air trap capacity while maintaining street-ready relaxed aesthetics.
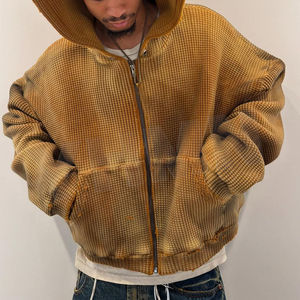
Custom branded thermal streetwear top featuring enzyme stone-wash and acid-wash distressing. Reinforced flatlock seam stitching guarantees structural integrity during repetitive heavy wear.
Premium 380 GSM ring-spun cotton fleece thermal layer with brushed inner back. Tailored in a modern boxy silhouette optimized for custom screen printing and high-density puff embroidery.
Pure GOTS-certified organic cotton thermal fleece offering skin-friendly breathable insulation. Hypoallergenic fabric structure engineered specifically for premium eco-conscious apparel brands.
Double-layer waffle knit insulation garment featuring custom dirty-wash dye aesthetics. Engineered with thermal waffle grid technology to retain body heat in dynamic outdoor environments.
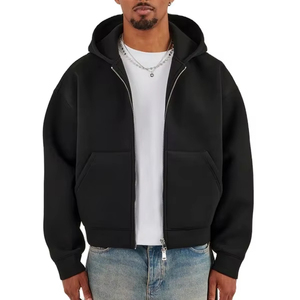
Industrial-strength 420 GSM 100% combed cotton zip thermal garment equipped with YKK hardware, pre-shrunk fabric treatment, and customizable inner neck satin labellings.
An authoritative technical analysis for global brand directors, procurement officers, and supply chain managers navigating next-generation thermal garment engineering.
The thermal underwear landscape is shifting rapidly from static thickness (GSM weight) to dynamic climate regulation. Modern procurement demands Phase Change Materials (PCM) encapsulated into micro-fibers, absorbing excess body heat during high exertion and releasing thermal energy when ambient temperatures plummet. OEM factories must now master paraffin micro-encapsulation, hollow-core thermal polyester extrusions, and far-infrared (FIR) emitting ceramic mineral additives that boost micro-vascular circulation.
Traditional cut-and-sew base layers create pressure points and chaffing during extended wear. B2B buyers are increasingly specifying 3D Seamless Circular Knitting machines (e.g., Santoni systems) that integrate varied compression zones, breathable mesh structures under armpits, and heavy-gauge honeycomb thermal traps across core muscular zones—all within a single continuous garment tube, eliminating seam breakdown risks.
Environmental regulations across the EU and North America are reshaping textile sourcing. Global importers require OEKO-TEX Standard 100, Global Recycled Standard (GRS) micro-polyester, and mulesing-free Merino wool combined with GOTS-certified organic cotton. Achieving 100% biodegradable thermal base layers without sacrificing tensile durability or wash-shrinkage tolerance is now a primary OEM benchmark.
When specifying custom thermal underwear production runs, selecting the appropriate fabric matrix directly dictates CLO value (thermal resistance), moisture vapor transmission rate (MVTR), and landed unit economics.
| Thermal Fiber Composition | GSM Range | CLO Value (Insulation) | MVTR (Moisture Wicking) | Target Market Application |
|---|---|---|---|---|
| 100% Micro-Fleece Polyester | 280 – 450 GSM | 0.85 – 1.45 High | Medium (12,000 g/m²/24h) | Extreme Cold Workwear & Heavyweight Streetwear |
| Merino Wool / Poly Synthetic Blend | 180 – 260 GSM | 0.95 – 1.60 Ultra-High | Very High (22,000 g/m²/24h) | Alpine Sport, Tactical Gear & Premium Activewear |
| Waffle-Knit Combed Ring-Spun Cotton | 240 – 500 GSM | 0.65 – 1.10 Moderate | High (Natural Absorption) | Lifestyle Casualwear & Heritage Apparel Brands |
| Bamboo Viscose / Spandex Stretch | 200 – 300 GSM | 0.55 – 0.90 Light-Medium | Ultra-High (Silky Hand-Feel) | Indoor Climate-Control & Everyday Base Layers |
As a dedicated custom OEM thermal underwear manufacturer and global exporter, our 50,000 ft² production complex eliminates intermediary markups, guarantees rigid AQL 2.5 quality control, and secures rapid supply chain execution.
We develop customized yarn specs directly with spinning mills. From 180 GSM ultralight base layers to 600 GSM double-brushed fleece, every batch undergoes mandatory colorfastness, anti-shrinkage (under 3% post-wash), and burst strength testing prior to cutting.
Thermal underwear requires flat, non-chafing joinery. Our heavy-duty Yamato 6-needle flatlock machines create zero-bulking flat seams capable of enduring 45+ lbs of tensile pull strength without thread fraying or seam popping.
Zero defect tolerance. Orders undergo four strict checkpoints: (1) 4-Point Raw Fabric Inspection, (2) In-line Stitch & Spec Checks, (3) AQL 2.5 Statistical Bulk Audits, and (4) Final Photo-Documented Pre-Shipment Inspection.
Direct technical answers to common questions asked by B2B sourcing managers, private label buyers, and textile apparel importers.
Partner with an audited, vertically integrated apparel factory. Contact our senior technical sourcing team today to request cost quotations, sample fabric swatches, or tech pack reviews within 24 hours.