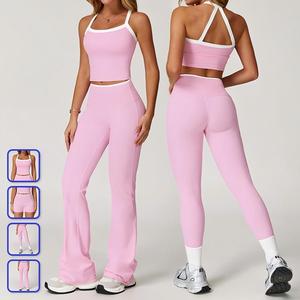
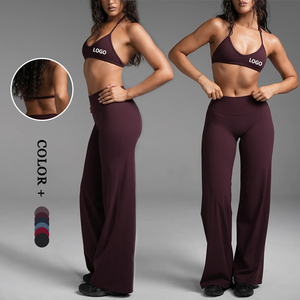
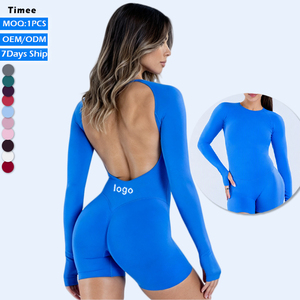
Executive Supply Chain Insight
Executive Summary: The Paradigm Shift in Seamless Activewear Manufacturing
Global activewear procurement has evolved beyond conventional cut-and-sew garment manufacturing. Modern performance brands require vertically integrated seamless technology that combines ergonomic structural support, material engineering, and rapid turnaround agility.
The global seamless activewear market is experiencing an unprecedented structural pivot. Modern consumers no longer view activewear solely through the lens of basic aesthetics; they demand high-performance functionality, multi-directional elasticity, second-skin comfort, and sustainable material footprints. As a result, premium brands, private label apparel lines, and athletic retail chains are shifting their procurement strategies toward specialized OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) factories equipped with advanced circular knitting machinery.
Unlike conventional cut-and-sew apparel—which relies on stitching together flat fabric panels with prominent, friction-inducing seams—seamless garment manufacturing produces continuous tubular knit fabrics directly from raw yarn feeds. This process eliminates up to 80% of side seams, reduces fabric waste during production by 30-40%, and enables micro-zoned compression directly into the weave structure. However, navigating seamless activewear manufacturing presents complex engineering challenges: precise yarn tension calibration, elastane ratio optimization, heat setting stabilization, and strict color fastness standards across multi-yarn blends.
This technical whitepaper provides sourcing directors, product developers, and apparel entrepreneurs with an authoritative blueprint for evaluating seamless activewear factories. By combining material science, circular knitting parameters, quality control protocols, and supply chain logistics, this guide establishes clear benchmarks for scaling activewear collections from initial tech pack creation to global distribution.
Engineering & Production Architecture
1. The Technical Architecture of Seamless Activewear: OEM vs. ODM Model
Understanding the operational and technical distinctions between OEM manufacturing and ODM turnkey development is critical for aligning factory capabilities with your brand's growth stage.
OEM Seamless Manufacturing (Client-Driven Tech Packs)
In the OEM manufacturing framework, our facility operates as a high-precision execution center for brand-provided technical specifications. Clients provide exact tech packs containing CAD patterns, yarn blend compositions (e.g., 87% Nylon 6,6 / 13% Spandex), target GSM weights, grading rules, and precise artwork positioning for jacquard branding or mesh ventilation structures.
- Exact replication of proprietary brand fit blocks and measurement charts
- Custom yarn sourcing according to client-specified suppliers or GOTS/GRS certifications
- Dedicated machine programming for proprietary compression zoning
- Strict non-disclosure agreements (NDAs) protecting trade secrets and custom designs
ODM Turnkey Product Development (Factory-Led Innovation)
The ODM model offers an end-to-end product development solution for growing apparel brands, e-commerce startups, and retail chains seeking rapid market deployment. Leveraging our extensive library of tested seamless patterns, yarn formulations, and anatomical compression zones, our engineering team converts high-level aesthetic concepts or mood boards into production-ready physical samples.
- In-house tech pack creation including measurement charts and stitch callouts
- Access to pre-engineered, market-tested circular knit silhouettes
- Turnkey branding: custom woven neck tags, heat-transfer care labels, and polybags
- Accelerated sampling cycles (7-10 days from concept approval to fit sample)
Santoni Seamless Circular Knitting Technology
Our owned production lines utilize state-of-the-art Santoni circular knitting machines (Cylinder Diameters: 12" to 20", Gauge: 28G to 40G fine pitch). These machines feature electronic needle-by-needle selection, allowing us to knit multi-density zones—such as breathable eyelet mesh under arms, high-compression under-bust support bands, and 3D contouring ribbing—in a single continuous tubular process without a single cut seam.
Material Science & Sourcing Roadmap
2. Material Science & Future Sourcing Trends (2025–2030)
The performance of seamless activewear depends fundamentally on raw material yarn composition, air-jet texturing, and chemical finishing. Here is how modern fabric engineering shapes activewear performance.
In seamless activewear manufacturing, yarn choice determines not only touch and drape, but also moisture transport efficiency, abrasion resistance, elastane degradation resistance, and garment memory. Our R&D center actively tracks material innovation across global markets to ensure our partner brands stay ahead of consumer demand.
Microfiber Nylon 6,6 vs. Nylon 6
We prioritize Polyamide 6,6 (Nylon 6,6) microfibers over standard Nylon 6 for high-end activewear. Nylon 6,6 offers a higher melting point, superior tensile strength, enhanced abrasion resistance (preventing thigh-chafing pilling), and a buttery-soft hand feel that retains shape after dozens of wash cycles.
Core-Spun Elastane & Tensioning
Spandex/Elastane (Creora® or Lycra®) is wrapped within air-jet textured nylon microfibers before knitting. This prevents direct skin exposure to bare elastane, eliminates shine under stretch, and maintains consistent tension control across high-compression waistband bands and 4-way stretch legs.
Bio-Based & Recycled Yarns (GRS)
Aligning with global sustainability directives, our factory offers GRS-certified Recycled Nylon 6 (Econyl® / Q-NOVA®) and bio-based polyamides derived from castor bean oil. These yarns reduce carbon emissions by up to 50% while delivering performance matching virgin synthesized polymers.
Factory Technical Specifications
3. Technical Sourcing Matrix & Performance Benchmarks
A rigorous comparative analysis of seamless activewear yarn formulations, knitting parameters, and physical performance metrics used across our OEM production lines.
| Garment Category |
Yarn Composition Spec |
Knitting Machine Gauge |
Target GSM Weight |
Performance Feature Matrix |
| High-Impact Sports Bras |
73% Micro-Nylon 6,6 / 27% Creora® Spandex |
36G Fine Pitch |
300 - 340 GSM |
Zero-Bounce Support, Encapsulated Compression Cup Zones, Anti-Microbial Finish |
| High-Waist Leggings (Butt-Lift) |
78% Air-Jet Nylon / 22% Covered Elastane |
32G - 34G Santoni |
280 - 320 GSM |
100% Squat-Proof (Zero Sheerness), Ribbed Core Control Waistband, Seamless Gusset |
| Lightweight Yoga Tops & Tees |
88% Recycled Poly / 12% Spandex / Mesh Inserts |
28G - 32G Gauge |
160 - 200 GSM |
Wicking Hydrophilic Finish, Micro-Eyelet Ventilation, 4-Way Stretch Drape |
| Seamless Bodysuits & Rompers |
80% Polyamide / 20% Elastane Blend |
34G Fine Pitch |
240 - 270 GSM |
Second-Skin Contour, Backless Halter Engineering, Anti-Chafing Flatlock Edge |
| Compression Biker Shorts |
75% Nylon 6,6 / 25% Spandex Ribbed Knit |
32G Gauge |
270 - 300 GSM |
No-Roll Waistband, Mid-Thigh Shape Memory, Anti-Pilling Surface |
Factory Capability & Quality Architecture
4. Enterprise Manufacturing Advantages: Real Factory vs. Trading Intermediary
Why 3,000+ apparel brands and institutional buyers partner directly with our owned 50,000 ft² production facility to guarantee quality, pricing transparency, and delivery timelines.
In the global apparel supply chain, sourcing through trading companies or third-party sourcing agents often introduces hidden markups, miscommunicated technical specs, inconsistent yarn lots, and unverified working conditions. Zega Apparel operates a fully owned, vertically integrated 50,000 ft² manufacturing plant staffed by over 200 trained textile engineers and machine technicians. Because every stage—from yarn inspection to final carton packaging—occurs under our own roof, we provide direct factory pricing, absolute specification control, and guaranteed delivery schedules.
4-Stage Quality Control Protocol
We execute strict quality gates: Gate 1: 4-Point System incoming yarn roll testing; Gate 2: Hourly in-line knitting tension and stitch checks; Gate 3: AQL 2.5 statistical audit after dyeing & boarding; Gate 4: Final pre-shipment photo audit.
Flexible MOQ (200 Units/Style)
While traditional overseas factories demand 1,000+ units per color, our lean production setup supports flexible MOQs starting at 200 pieces per style/color, complete with free size breakdowns (S through 3XL). This allows emerging DTC brands to test market demand without locking up capital.
Global DDP Logistics (30+ Countries)
We streamline international trade by offering full DDP (Delivered Duty Paid) door-to-door shipping alongside FOB and express air options. We handle custom clearance, HS-code documentation, tariffs, and duty clearance for buyers in the USA, UK, Canada, Australia, Europe, and UAE.
Standard Operating Procedure
5. The 4-Stage OEM/ODM Manufacturing Workflow
From initial design concept to final warehouse delivery, our structured production workflow ensures clarity, milestone sign-offs, and risk mitigation at every step.
STAGE 01
Spec & Quotation
Submit your tech pack, sketches, or reference garment. Our engineering team calculates yarn yields, machine programming times, and issues an itemized quotation within 24–48 hours.
STAGE 02
Sampling & Lab Dips
We engineer CAD patterns, perform lab-dip color matching (Pantone TPX/TCX), and knit pre-production fit samples in 7–10 business days for physical evaluation.
STAGE 03
Bulk Circular Knitting
Upon sample approval, bulk Santoni circular knitting begins alongside dyeing, steam boarding, branding application, and continuous in-line quality monitoring.
STAGE 04
AQL 2.5 & Dispatch
Cartons undergo AQL 2.5 final inspection, private-label packaging, barcode labelling, and custom export packing before DDP shipping to your warehouse.
Procurement Knowledge Base
6. Frequently Asked Questions (FAQ) for Activewear Sourcing
Technical guidance addressing the most common questions raised by brand managers, procurement leads, and product designers during factory audits.
What is your minimum order quantity (MOQ) for custom seamless activewear?
Our baseline MOQ is 200 pieces per style, per colorway. Within that 200-piece commitment, you can freely divide size breakdowns across S, M, L, XL, and XXL at no additional charge. Pre-production physical samples are produced and approved before initiating bulk production.
How do you guarantee that high-waist seamless leggings are 100% squat-proof?
Squat-proof opacity depends on yarn density, needle gauge, and elastane wrapping. We utilize high-gauge 32G/34G Santoni circular knitting machines with high-denier air-jet micro-nylon yarns (70D/68F) and high spandex content (22%-28%). Every fabric batch undergoes a standardized stretch-and-light-transmittance test before releasing the lot for cutting and assembly.
Do I need a finalized tech pack before contacting your factory?
No. While having a complete tech pack speeds up costing, our in-house ODM design department can build production-ready tech packs directly from reference garments, physical samples, or high-resolution mood boards. We provide pattern engineering, measurement grading, and trim specification sheets prior to sample creation.
What is the typical turnaround time for sampling and bulk production?
Cost estimates are provided within 24 to 48 hours of specification review. Technical fit sampling and lab dips require 7 to 10 business days. Once the pre-production sample is approved by your team, bulk manufacturing is completed in 2 to 3 weeks for standard activewear knit programs.
What private label branding services are handled in-house?
We deliver complete retail-ready private label packages: seamless knitted-in jacquard logos, heat-transfer silicone logos, woven care/content labels, custom hangtags, branded polybags, eco-friendly mailing boxes, and scannable UPC barcode stickers applied directly at our facility.
What quality compliance standards and certifications do your facilities hold?
Our manufacturing plant operates in full compliance with ISO 9001 quality management systems. All yarns, dyes, and chemical finishing agents used in our seamless production hold OEKO-TEX Standard 100 certification (Class I for skin contact safety). Additionally, our workplace undergoes annual BSCI and WRAP social compliance audits.
Ready to Build Your Seamless Activewear Collection?
Connect directly with our engineering and sourcing team to discuss technical specifications, receive instant pricing quotes, or request custom fabric sample swatches.