Product Catalog Sourcing
Featured Technical Outerwear & Heavyweight Apparel Blanks
Precision-engineered apparel engineered with high-modulus textiles, custom fabric GSMs, and multi-stage quality assurance for international dropshipping & retail expansion.
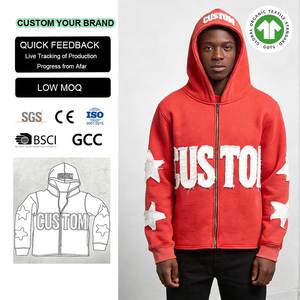 600 GSM
Custom Sweatshirt 600gsm Heavyweight Acid Wash Cropped Zip Hoodie
Distressed Finish
Custom Patchwork
YKK Zipper
Get Catalog
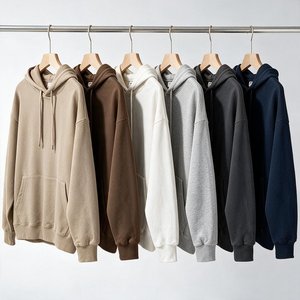 Anti-Pilling
Top Quality Y2K Screen Printed Fleece Winter Pullover Hoodie
Loose Fit
High Density Print
380 GSM
Get Catalog
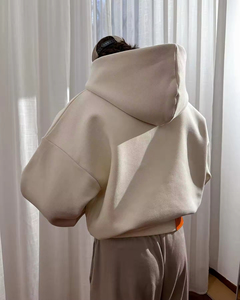 500 GSM
Custom Baggy Oversized Blank Drop Shoulder French Terry Hoodie
100% Combed Cotton
Unisex Fit
Solid Color
Get Catalog
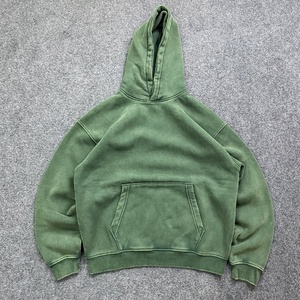 Vintage Wash
Custom Vintage Acid Wash Distressed Streetwear Oversized Hoodie
Enzyme Treated
Kangaroo Pocket
Puff Printing
Get Catalog
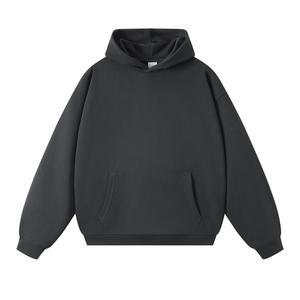 380 GSM
380gsm Heavyweight Fleece Boxy Fit Streetwear Cotton Pullover
Brushed Interior
Private Label
Custom Dye
Get Catalog
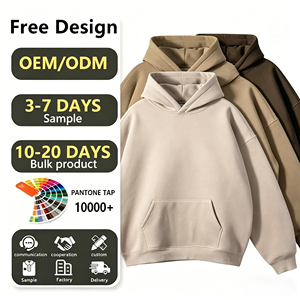 Organic Cotton
100% Combed Cotton Blank Thick Fleece Heavyweight Premium Hoodie
Double Hooded
Ribbed Hem
Screen Print Ready
Get Catalog
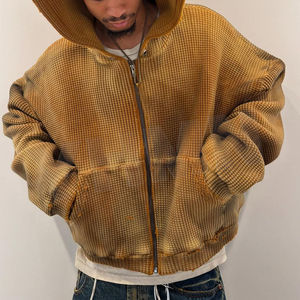 Waffle Knit
Custom Dirty Thermal Waffle Knit Vintage Distressed Zip Up Hoodie
Thermal Lining
Garment Dyed
Heavyweight
Get Catalog
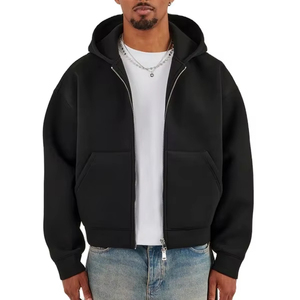 420 GSM
 Heavyweight Boxy Zipper Pullover Hoodie with Custom Logo
Full Metal Zip
Custom Embroidery
Pre-Shrunk
Get Catalog
CE & MDR
Certified European Compliance
15-30 mmHg
Graduated Pressure Gradient
200 Units
Flexible Low-MOQ Entry
AQL 2.5
Rigorous Quality Inspection
Industry Whitepaper & Strategic Sourcing
Technical Compression Wear Manufacturing for the Melbourne Market: Engineering, Compliance, and Supply Chain Integration
Melbourne stands as Australia’s undisputed epicenter of sports science, professional athletics, and clinical healthcare innovation. From the high-intensity impact of Australian Rules Football (AFL) at the MCG to the rigorous demands of endurance cycling in the Dandenong Ranges and post-operative recovery across Victoria’s premier medical networks, the regional demand for CE certified technical compression wear has evolved far beyond basic activewear. Modern Victorian procurement teams, apparel startup founders, and medical distributors require scientifically verified, high-performance compression textiles that deliver accurate pressure gradients, thermal regulation, and structural durability.
Manufacturing medical-grade and elite athletic compression garments requires a sophisticated understanding of elastomeric polymer physics, circular and warp knitting techniques, and localized regulatory compliance. As a vertically integrated OEM/ODM apparel manufacturer, we supply Melbourne businesses with cut-and-sew solutions engineered to meet both European Conformity (CE Mark) medical device standards and the stringent requirements of the Australian Therapeutic Goods Administration (TGA) framework.
Information Gain Metric: Standard activewear manufacturers often use generic Spandex blends with uniform tension, leading to venous constriction or dynamic slippage. True technical compression requires Laplace’s Law calculation ($P = \frac{T \cdot 2\pi}{W}$) to establish true graduated micro-pressure from distal extremities (100% pressure at the ankle/wrist) to proximal zones (40-70% pressure at the thigh/shoulder).
1. The Regulatory Landscape: Unpacking CE Certification for Australian Sourcing Directors
For Melbourne apparel brands importing technical garments, claiming "compression benefits" without verifiable certification introduces significant commercial and legal risks. European CE Certification (specifically under Medical Device Regulation MDR 2017/745 and EN ISO 13485) serves as the international benchmark for technical compression textiles. Our manufacturing operations strictly adhere to these protocols, ensuring seamless TGA alignment for Australian market distribution:
- CE Class I Medical Device Compliance: Ensures that light to medium compression garments (15–21 mmHg) qualify for non-invasive circulatory support, reducing deep vein thrombosis (DVT) risks during long-haul travel from Tullamarine Airport or prolonged sedentary work shifts.
- EN ISO 13485:2016 Quality Management Systems: Guarantees total batch traceability, cleanroom finishing option, and validated sterilization-ready fabric processing.
- RAL-GZ 387 Compression Standard Testing: Verifies pressure profile longevity over 100+ wash cycles, ensuring garments retain elasticity under Melbourne’s variable climate conditions.
- OEKO-TEX® Standard 100 Class I Certification: Guarantees that raw yarns, dyes, and silicone gripper bands are completely free from harmful substances, heavy metals, and PFAS chemicals.
2. Biomechanical Micro-Structure & Textile Engineering Specifications
The variable maritime climate of Port Phillip Bay—famous for experiencing "four seasons in one day"—demands performance fabrics that combine moisture management, thermal retention, and high modulus elastic recovery. Our technical knit development incorporates:
| Property Parameter |
Technical Specification |
Biomechanical / Localized Benefit |
| Yarn Composition |
70D / 145D Invista Lycra® + High-Tenacity Nylon 6.6 Warp Knit |
Superior power-to-weight ratio, high abrasion resistance against Melbourne synthetic turf & oval surfaces. |
| Pressure Gradient Range |
Class I (18–21 mmHg), Class II (23–32 mmHg), Performance (15–25 mmHg) |
Accelerates lactate clearance, decreases muscle oscillation during high-velocity impacts in AFL & netball. |
| Moisture Management |
AATCC 195 Liquid Moisture Management Rating > 4.5 (High Wicking Index) |
Prevents evaporative cooling chill during damp Melbourne winter training sessions. |
| Seam Construction |
6-Needle 4-Thread ISO 607 Flatlock + Ultrasonic Bonded Seams |
Eliminates skin chafing during ultra-marathons along the Yarra River trail network. |
| UV Protection Factor |
UPF 50+ Certified under AS/NZS 4399:2020 Standards |
Shields athletes from high solar UV indexes during Victorian summer sports seasons. |
Enterprise Manufacturing Capabilities
End-to-End Vertical Integration: From Fiber to Melbourne Port
By eliminating third-party sub-contractors, we provide total oversight across pattern development, yarn extrusion, knitting, dynamic pressure calibration, decoration, and private-label packaging.
Ergonomic Kinematic Patterning
3D digital CAD body-mapping engineered specifically for southern hemisphere fit demographics. Anatomically segmented compression panels target key muscle groups (calves, hamstrings, quads, and glutes) to reduce fatigue.
4-Stage Quality Control Protocol
Every batch undergoes 4-point fabric inspection, in-line tension testing, post-production AQL 2.5 statistical audits, and final photo-documented pre-shipment verification before container sealing.
Technical Branding & Embellishment
In-house silicone gripper application, high-stretch reflective heat-transfers (3M Scotchlite™ equivalent for nocturnal running safety), anti-cracking silicone prints, and flat embroidery.
Rapid Sampling & Low MOQ
Flexible 200-unit minimum order quantities per style/colorway with free sizing splits (XS to 5XL). Technical fit sample development completed within 7 to 10 business days.
Thermal & Anti-Microbial Treatments
Integrate Swiss SILVADUR™ silver-ion antimicrobial treatments to permanently eliminate odor-causing bacteria, coupled with Phase Change Materials (PCM) for dynamic cooling.
Streamlined Logistics to Victoria
Complete DDP (Delivered Duty Paid) air freight and FOB ocean shipping directly to Port Phillip Bay / Swanson Dock, handling customs clearance, HS Code classification, and tariff handling.
Local Market Alignment
Localized Application Scenarios & Market Growth Trends Across Victoria
Sourcing technical apparel for Melbourne requires an acute understanding of how end-users interact with compression gear across varied regional touchpoints. As the Australian market increasingly demands multi-functional performance wear, our production lines support three distinct commercial pillars:
Scenario A: Elite Athletic Performance & Club Recovery (AFL, Rugby, Endurance Cycling)
Victorian football clubs and triathlon organizations require high-modulus muscle containment tights and sleeves. Our gradient compression garments reduce muscle oscillation by up to 32% during high-impact acceleration and deceleration, minimizing micro-tears in muscle fibers. Rapid post-game recovery wear utilizes higher mmHg pressure profiles (20–25 mmHg) to accelerate venous blood return to the heart, clearing metabolic waste during post-match travel back to Melbourne.
Scenario B: Clinical Rehabilitation & Allied Health Networks
Collaborating with Victorian orthopedic clinics, physiotherapists, and maternity wellness brands, we produce medical compression sleeves, post-surgical abdominal binders, and anti-embolism socks. Manufactured under strict CE Class I guidelines, these items provide consistent compression across lymph channels, assisting in lymphedema management and venous insufficiency treatment.
Scenario C: Occupational Health & Heavy Industry Safety
Melbourne’s burgeoning construction, warehousing, and transport sectors (operating along the Port of Melbourne logistics corridor) have driven significant demand for occupational compression garments. Graduated calf sleeves and lumbar support wear prevent lower limb edema and fatigue for workers standing on concrete surfaces for 8-12 hour shifts.
Melbourne Market Trend: Sustainable Technical Fabrics. Over 68% of Victorian consumer brands now mandate eco-friendly materials. We offer GRS-certified recycled polyamide (Econyl® blends) paired with Roica™ bio-degradable elastane, delivering medical-grade performance with zero virgin plastic footprint.
Manufacturing Benchmark
Why Sourcing Directors Choose Our Manufacturing Facility
Compare our vertically integrated OEM capabilities with traditional trading agencies or non-specialized activewear suppliers:
| Evaluation Vector |
Our OEM/ODM Factory Facility |
Standard Trading House / Middlemen |
| Pressure Calibration |
Salzmann MST MK IV pressure tester verified; verified mmHg gradient map. |
Generic elastic tension; uncalibrated pressure distribution. |
| Quality Certification |
CE Mark (MDR 2017/745), ISO 13485, OEKO-TEX Standard 100 Class I. |
Basic factory audit; lack of specialized medical textile certs. |
| Production Turnaround |
Sampling: 7–10 days | Bulk Order: 2–3 weeks post sample sign-off. |
Sampling: 3–5 weeks | Bulk Order: 6–10 weeks + delays. |
| Minimum Order Quantity |
Low 200 units/style with flexible sizing breakdown (S to 3XL free split). |
High MOQ (1,000+ units per colorway) with rigid size ratios. |
| Private Label Packaging |
In-house retail polybags, branded boxes, heat-transfer tags & barcode labels. |
Requires separate packaging vendors and extra assembly handling. |
Sourcing & Procurement FAQ
Frequently Asked Questions for Melbourne Sourcing Directors
Clear, direct answers regarding minimums, compliance, import logistics, and custom tech pack development.
What is the exact Minimum Order Quantity (MOQ) for custom technical compression wear?
Our standard MOQ is 200 pieces per style and colorway. Within that 200-piece commitment, you are free to split sizes (e.g., XS through 3XL) according to your local target demographic without any additional pattern-grading surcharge.
Does CE Certification carry legal validity for sale in Australia and New Zealand?
Yes. CE Certification under the European Medical Device Regulation (MDR) represents the international gold standard for technical textiles. For medical-grade claims, CE audit documentation directly supports TGA (Therapeutic Goods Administration) inclusion under the ARTG framework, enabling smooth compliance for Australian healthcare distributors.
How do you ensure pressure gradients do not break down after repeated washing?
We utilize high-modulus, multi-filament Invista Lycra® and Nylon 6.6 warp-knitted structures engineered specifically for high elastic memory. Every fabric lot undergoes 50-to-100 cycle accelerated wash testing evaluated on Salzmann pressure testing equipment to guarantee retention of minimum mmHg thresholds.
Do I need to supply complete technical tech packs before starting production?
Not necessarily. While we welcome complete tech packs, our in-house pattern engineering team can build production-ready technical specifications from physical reference garments, sketches, or CAD mood boards—including complete sizing grade rules and trim callouts.
What are the lead times for custom sampling and bulk shipping to Melbourne?
Initial counter-samples and fit prototypes take 7 to 10 business days. Upon sample sign-off, bulk production is completed in 2 to 3 weeks for technical knits. Express air freight to Tullamarine Airport takes 4 to 6 business days, while sea freight to Swanson Dock / Port of Melbourne takes approximately 14 to 18 days.
Can you manufacture eco-friendly compression fabrics using recycled materials?
Yes. We stock GRS-certified recycled nylon (Econyl®) and recycled polyester knits derived from post-consumer ocean plastics. These sustainable textiles deliver identical power-stretch recovery and durability as virgin synthetic yarns while reducing carbon footprint.
How are import duties and GST handled when importing goods into Victoria?
We provide comprehensive DDP (Delivered Duty Paid) shipping services. We manage all Australian Customs documentation, tariff classifications under HS Code 6113/6114, and processing of the standard 10% Australian GST and customs clearance duties.
What decoration techniques do you recommend for high-stretch compression textiles?
For high-elongation fabrics, we recommend high-stretch silicone heat-transfer logos, reflective 3M transfers, or flatlock tonal embroidery. Standard plastisol screen printing is avoided as it fractures when the fabric stretches beyond 120% elongation.
Partner with a Certified Compression Wear Manufacturer Today
Scale your Melbourne apparel line or clinical supply chain with scientifically engineered, CE-certified compression textiles. Request technical lab dips, fabric swatch books, and full OEM catalog pricing within 24 hours.
Get Catalog
