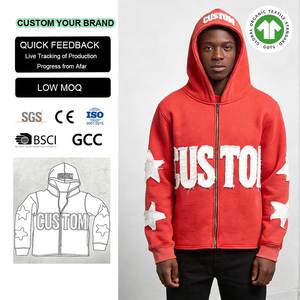
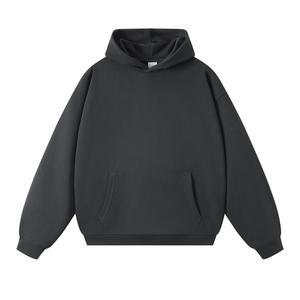
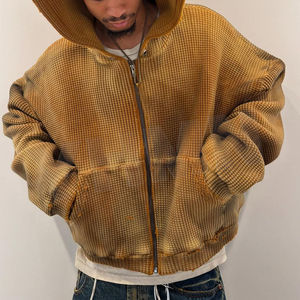
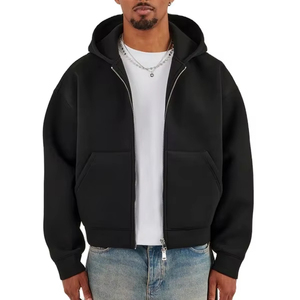
Custom Manufacturer Sweatshirt 600gsm Heavyweight Thick Distressed Cropped Zip up Embroidery Patch Men Acid Wash Zip up Hoodie
Top Quality Hoodies Sudaderas Y2k Screen Printed Winter Hoodie Anti-Pilling Loose Fit Men's Hoodie Pullover Hoddies Men
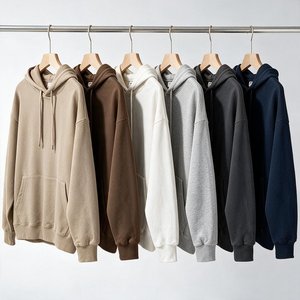
Custom Baggy Oversize Blank Unisex Drop Shoulder Heavyweight Crop Cut Big Hoodie 500Gsm Cotton Solid Color Cropped Baggy Hoodies
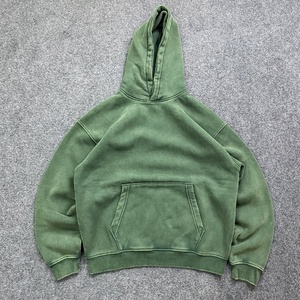
Custom Logo Distress Acid Wash Oversize Pocket Vintage Printing Blank Plain Loose Streetwear Hoodies For Men
380gsm Heavyweight Fleece Hoodie Boxy Fit Streetwear Cotton Rich Pullover Custom Private Label Blank Hoody
100% Cotton Hoodies Blank Thick Fleece Heavy Weight Oversized Hoodies Custom Print Logo Men's Hoodies & Sweatshirts
Custom Cotton Dirty Thermal Oversized Heavyweight Zip up Waffle Knit Blank Vintage Distressed Acid Wash Hoodies Sweatshirt Men
Zip Up Hoodie Heavyweight Pullover Boxy Hoodie Print Logo Heavy Weight 420 Gsm Plain 100%cotton Zipper Custom Zip Up Hoodie
Whitepaper: Strategic Sourcing of Private Label Apparel & Custom Packaging for Greater Boston Apparel Brands
The apparel landscape in Greater Boston—stretching from the luxury retail corridors of Newbury Street to the collegiate fashion movements in Cambridge and the tech-driven activewear startups in the Seaport District—demands an unprecedented level of supply chain precision. Brands operating in New England face dual pressures: maintaining high material durability against harsh climate shifts while delivering premium, retail-ready unboxing experiences to increasingly discerning consumers. As traditional domestic manufacturing options remain cost-prohibitive for scaling independent labels, the strategic bridge between China’s advanced vertically integrated OEM/ODM factories and Boston-based brand headquarters has become the gold standard for sustainable margin expansion.
Information Gain Strategic Insight: Traditional sourcing relies on multi-tiered brokers that fragment cut-and-sew operations, screen printing, and packaging production. Our vertically integrated direct-factory model consolidates fabric knitting, garment dyeing, custom trim engineering, and polybag/box manufacturing under one roof—reducing lead times by 35% and eliminating color variance across batch drops.
1. Technical Specification & Fabric Engineering for New England Climates
Boston's coastal humidity paired with freezing winter cycles creates specialized consumer demand for heavy-density fleece, French terry, and thermal waffle knits. Sourcing off-the-shelf garments leads to shrinkage drift and premature pilling. Premium Boston private label brands require technical specs tailored to specific GSM (Grams per Square Meter) callouts:
- 600 GSM Heavyweight Fleece: 100% combed ring-spun cotton engineered with a 3-end fleece structure for maximum thermal insulation, double-lined hoods, and acid-wash finish stability.
- 500 GSM Drop-Shoulder French Terry: Zero-shrinkage unbrushed loops providing structured drop-shoulder silhouettes suitable for Boston streetwear capsules.
- 380 GSM - 420 GSM Boxy Cut Blanks: High-density 20s/1 yarn count cotton optimized for puff printing, multi-color screen printing, and complex embroidery patches.
- Waffle-Knit Thermal Lining: 280 GSM honeycomb cotton backing for vintage-wash zip-ups designed for layered New England autumn and winter styling.
2. Custom Packaging Architecture: Delivering Retail-Ready Unboxing
In modern e-commerce and boutique retail, the garment packaging is as crucial as the stitch quality. Our direct-from-factory custom packaging pipeline ensures that every bulk order arrives fully retail-ready for immediate fulfillment at Boston distribution hubs or direct-to-consumer (DTC) shipping from local warehouses.
We provide full-scale bespoke apparel packaging options tailored to your brand identity:
- Biodegradable Frosted Ziplock Bags: Eco-friendly TPU/EVA matte polybags featuring custom ventilation valves, brand logos, and warning labels printed in accordance with Massachusetts retail compliance codes.
- FSC-Certified Rigid Presentation Boxes: Matte black or custom PMS-matched corrugated boxes with metallic foil stamping, embossed brand seals, and custom tissue paper wraps.
- Custom Trims & Accessories: Woven satin neck labels, high-density heat transfer care tags, custom die-cut hangtags with metallic eyelets, and scannable UPC/EAN barcode stickers.
Integrated Manufacturing Capabilities
Vertically Integrated Cut & Sew
Owned 50,000 ft² production floor with 200+ master tailors. Pattern making, automated fabric cutting, seam assembly, and trimming under single-roof supervision.
Advanced Dyeing & Washing
In-house artisan wash treatments including acid wash, pigment vintage overdyes, stone washing, and enzyme softeners tested against color-fastness standards.
Custom Branding & Packaging
Complete OEM/ODM private label packages. Woven neck labels, hangtags, barcodes, custom polybags, and rigid presentation boxes custom built per client spec.
Localized Boston Application Scenarios & Market Trends
Private label apparel demand in Boston varies significantly across distinct commercial micro-markets. Sourcing requires localized intent understanding to match production parameters with target audience expectations:
A. Streetwear & Boutique Retail (Newbury Street & Back Bay): Brands operating in Boston's premium fashion hubs require heavy cotton weights (450+ GSM), distressed vintage finishes, cropped boxy fits, and 3D puff embroidery. Low 200-unit MOQs allow boutique owners to execute limited drop calendars without sitting on excess deadstock.
B. University & Campus Merchandise (Cambridge, Harvard Square & Allston): Collegiate apparel is evolving beyond generic blank printing. Modern student fashion trends favor drop-shoulder silhouette hoodies, Y2K aesthetic screen-printed graphics, anti-pilling fleece blends, and custom branded neck taping.
C. Activewear & Tech Corporate Apparel (Seaport District & Kendall Square): High-density poly-spandex blends, moisture-wicking knits, flatlock stitching, and subtle silicon logo applications represent the core requirement for Boston's thriving biotech, robotics, and SaaS corporate merchandise drops.
The Boston B2B Supply Chain Roadmap: China Factory to MA Warehouse
To ensure smooth delivery into Massachusetts, our export department manages complete DDP (Delivered Duty Paid) logistics solutions directly servicing Boston Logan International Airport (BOS) air cargo hubs and the Port of Boston (Conley Terminal ocean freight). We handle customs clearance, tariff classification (HS Codes), and Section 321 duty-free exemptions where applicable, ensuring predictable landed costs with zero hidden fees.
Q: What is your minimum order quantity (MOQ) for custom private label apparel?
Our minimum order quantity is 200 pieces per style/colorway. Within that 200-unit order, you can split sizes (e.g., Small through 3XL) at no additional charge. We produce 1–3 pre-production physical samples for sign-off before commencing bulk line production.
Q: Can you manufacture both custom clothing and custom packaging together?
Yes! We offer fully integrated custom apparel and packaging solutions. We manufacture your garments (cut & sew, printing, embroidery, neck labels) and pack them directly into your custom frosted polybags or branded presentation boxes at our factory floor, so cartons arrive in Boston 100% retail-ready.
Q: Do I need a complete Tech Pack to get started?
No. If you do not have a professional tech pack, our in-house pattern design team can build CAD technical packs from reference physical garments, detailed sketches, or mood boards—including measurement grading charts, stitch callouts, and print placement diagrams.
Q: What are the lead times for sample development and bulk shipping to Boston?
Sample turnaround takes 7–10 business days. Approved bulk orders for standard fleece and hoodies are manufactured in 2–3 weeks. DDP express air freight to Boston takes 5–7 business days, while ocean freight to the Port of Boston takes approximately 25–30 days depending on vessel schedules.
Q: How is quality control verified to prevent defective shipments?
We employ a strict 4-stage inspection gate system: 4-point fabric inspection upon raw mill arrival; in-line sewing floor audits; AQL 2.5 statistical inspection for workmanship, seam strength, and print durability; followed by a complete photo-documented pre-shipment carton audit.
Q: How are US import tariffs and customs handled for Massachusetts deliveries?
We offer complete DDP (Delivered Duty Paid) shipping terms. Our export department handles all customs paperwork, duty payments, ISF filings, and logistics coordination directly to your Boston store, warehouse, or fulfillment center without unexpected fees.