Low MOQ Private Label Clothing Manufacturing For Global Brands
Engineered for high-growth streetwear, activewear, and fashion labels. Cut & sew production, pattern grading, custom dyeing, screen printing, embroidery, and retail packaging under one roof — starting at just 200 units per style.
In today's fast-moving fashion market, emerging independent designers, direct-to-consumer (DTC) brands, and enterprise procurement teams face a critical operational dilemma: balancing working capital risk against product quality. Traditional apparel manufacturers enforce massive minimum order quantities (1,000 to 5,000 units per style), trapping inventory capital and forcing compromise on custom fit, fabric GSM, and specialized detailing.
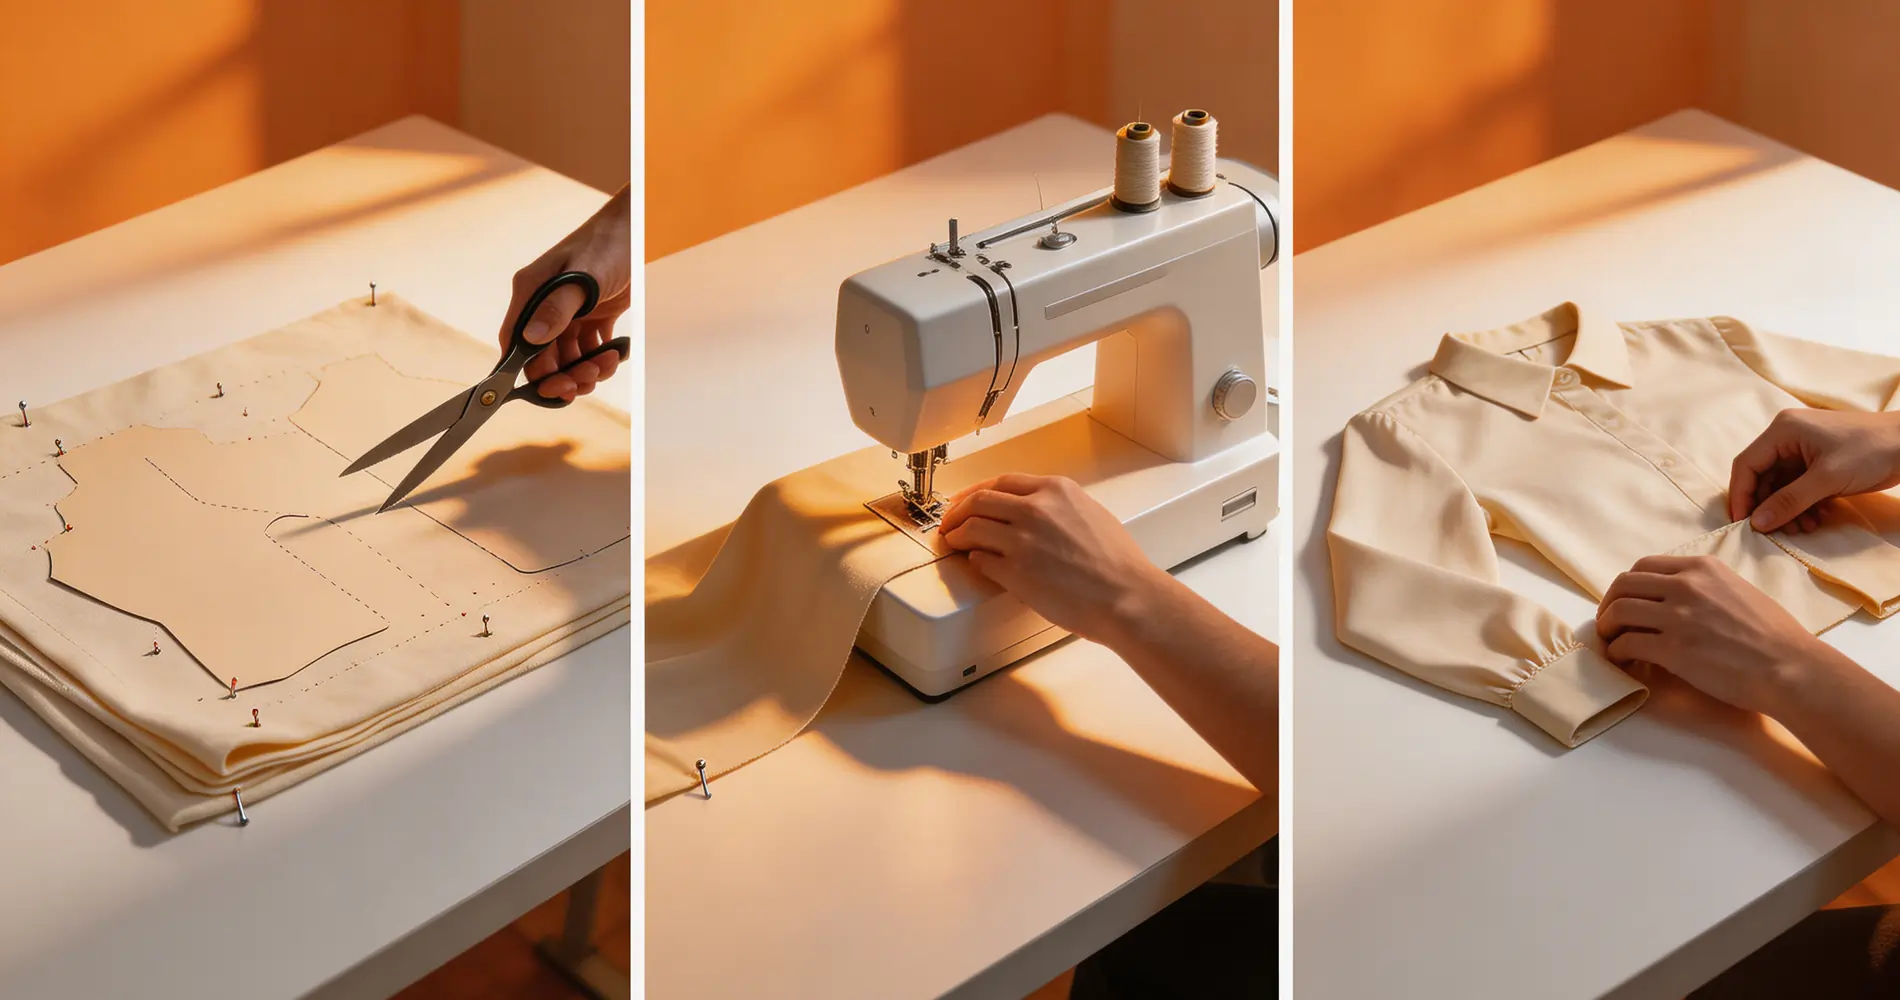
Zega Apparel reshapes this model through vertically integrated low MOQ private label clothing manufacturing. Operating an owned 50,000 square foot industrial facility equipped with modern computerized cutting tables, multi-head embroidery machines, high-density screen printing lines, and automated pattern grading software, we empower brands to order as few as 200 units per style without sacrificing factory-direct pricing or custom engineering.
From initial tech pack creation and lab-dip color matching to final AQL 2.5 quality control inspection and retail polybagging, every single production stage occurs under our own roof. This eliminates middleman trading desks, guarantees total supply chain traceability, and safeguards your proprietary designs.
Dedicated project manager assigned to every order with weekly video production updates
Complete tech pack development from basic sketches, CAD files, or reference garments
Ethical, sweatshop-free manufacturing facility operating in full compliance with international labor standards
Recommended Apparel Lines for Low MOQ Private Label Production
From luxury heavyweight streetwear to technical activewear and eco-friendly organic basics, we custom manufacture diverse product categories engineered to your exact GSM specs, fit blocks, and decorative callouts.
Custom Heavyweight & Oversized T-Shirts
Engineered using 100% combed ring-spun cotton, organic jersey, and tri-blends from 180 to 280 GSM. Available in boxy streetwear drops, relaxed drop-shoulder cuts, standard athletic fits, and seamless tubular builds with reinforced twin-needle stitching.
MOQ 200 Pcs180–280 GSM
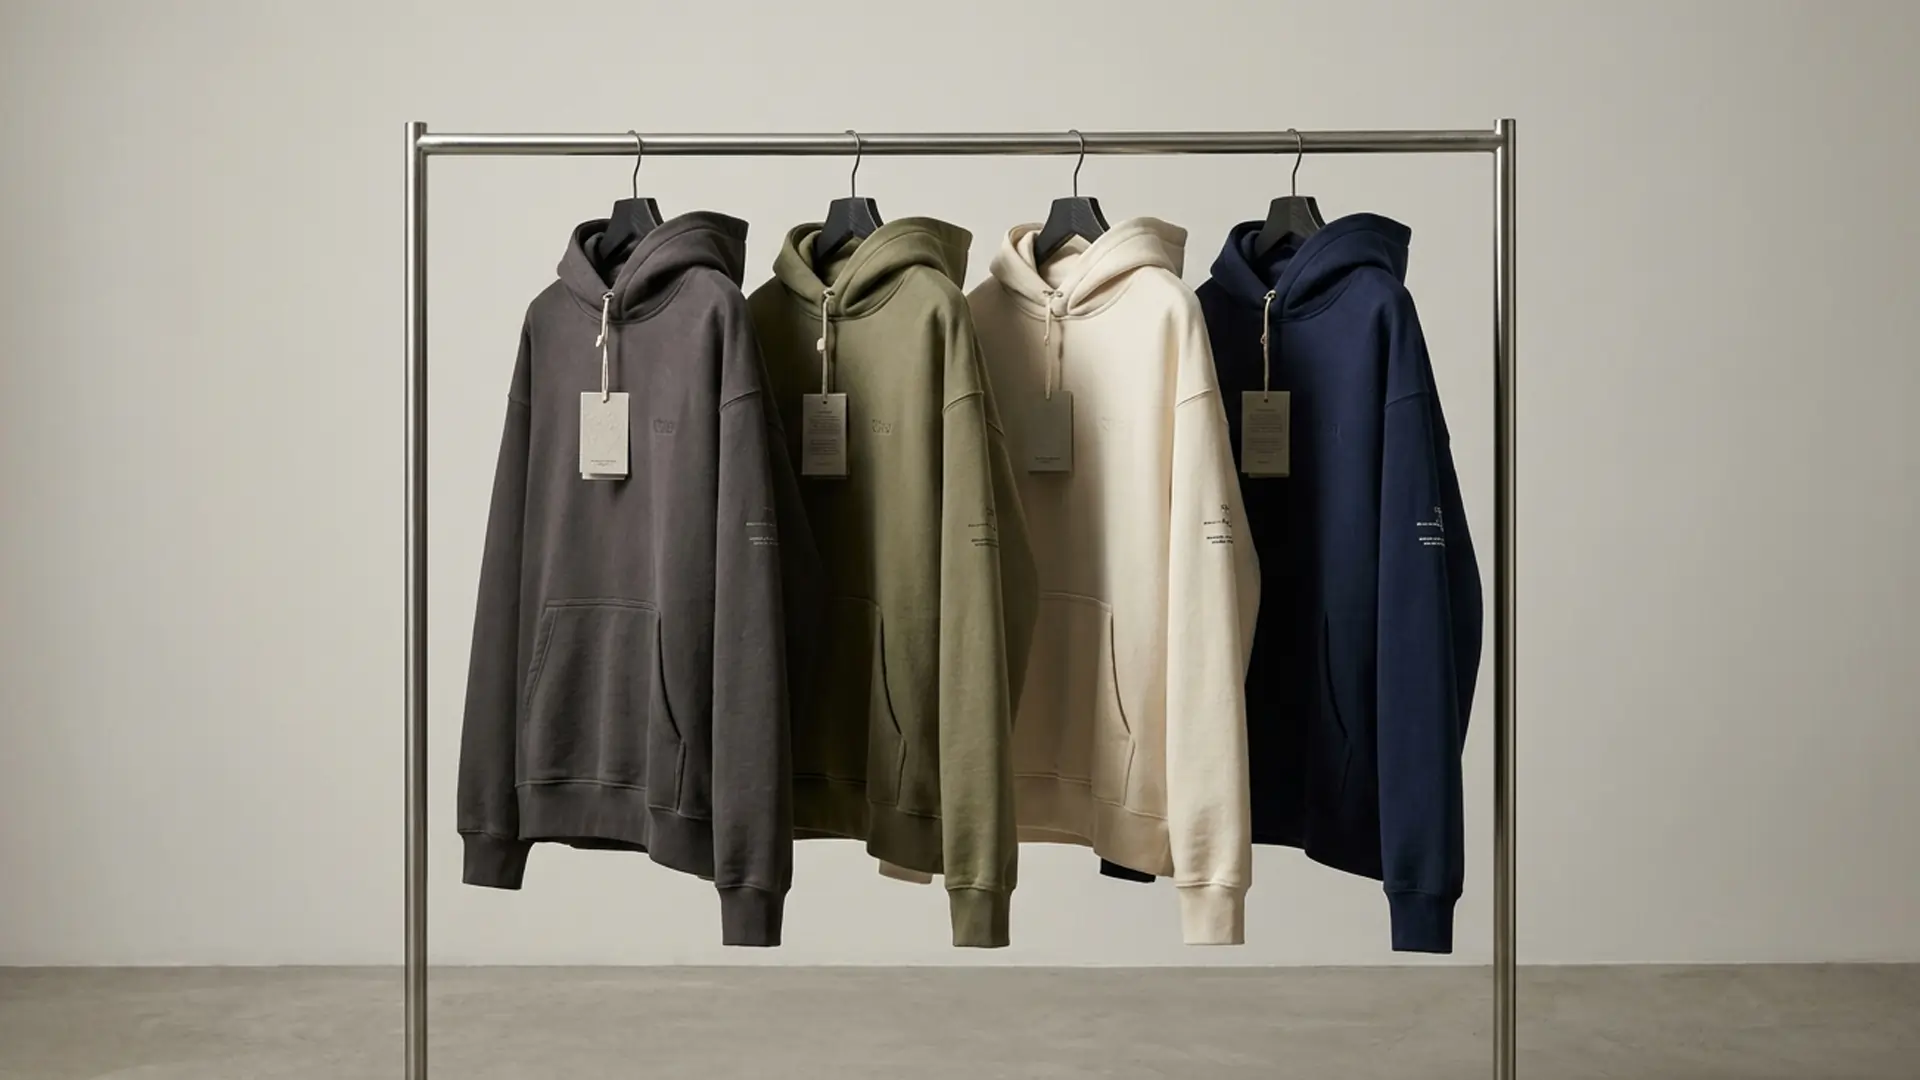
Heavyweight Hoodies & French Terry Sweatshirts
Crafted from premium 300 to 460 GSM combed cotton brushed fleece and loopback French terry. Featuring double-lined hoods, ribbed side paneling, custom metal eyelets, custom drawcords, and high-density puff print or 3D embroidery decoration.
MOQ 200 Pcs300–460 GSM
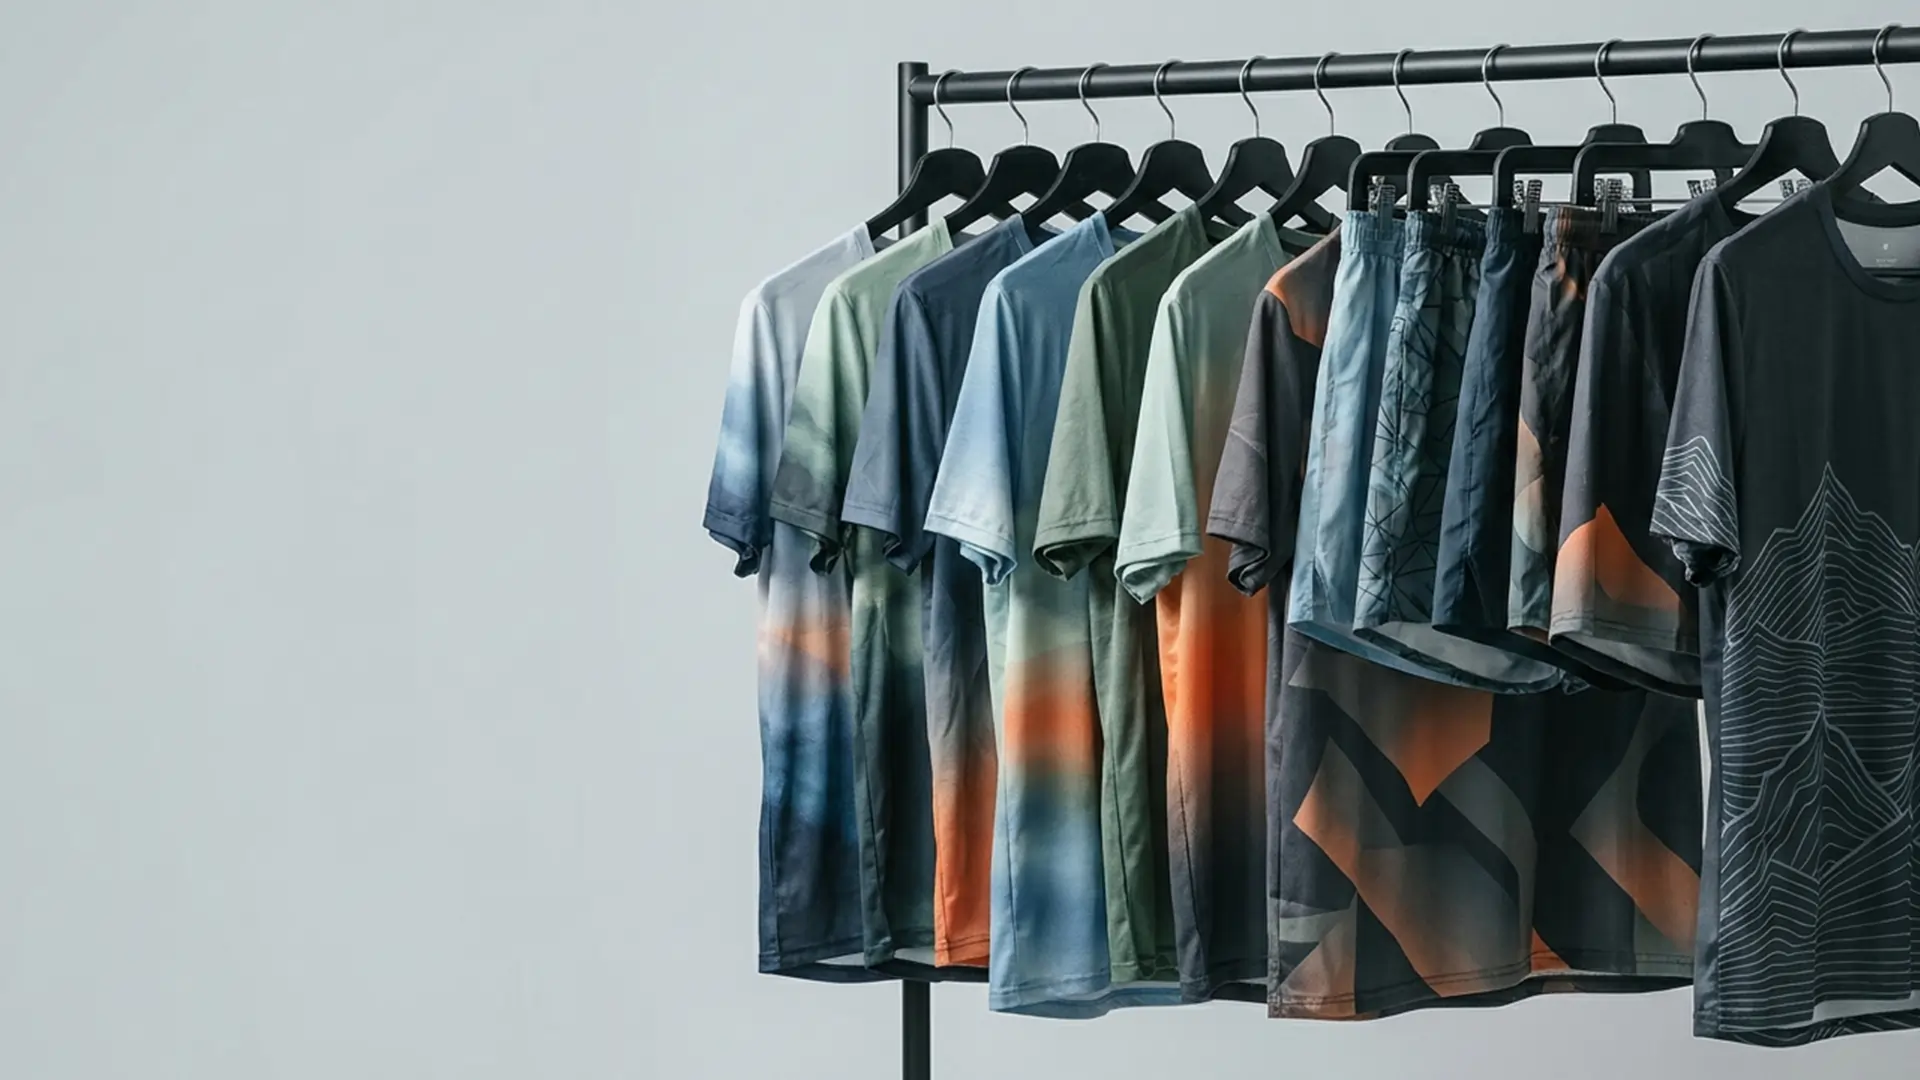
Performance Sportswear & Gym Wear
Technical activewear engineered with 4-way stretch poly-spandex blends, moisture-wicking coatings, and anti-microbial treatments. Built using flatlock anti-chafing seams, laser-cut ventilation holes, bonded zip pockets, and all-over sublimation printing.
MOQ 200 PcsFlatlock Stitching
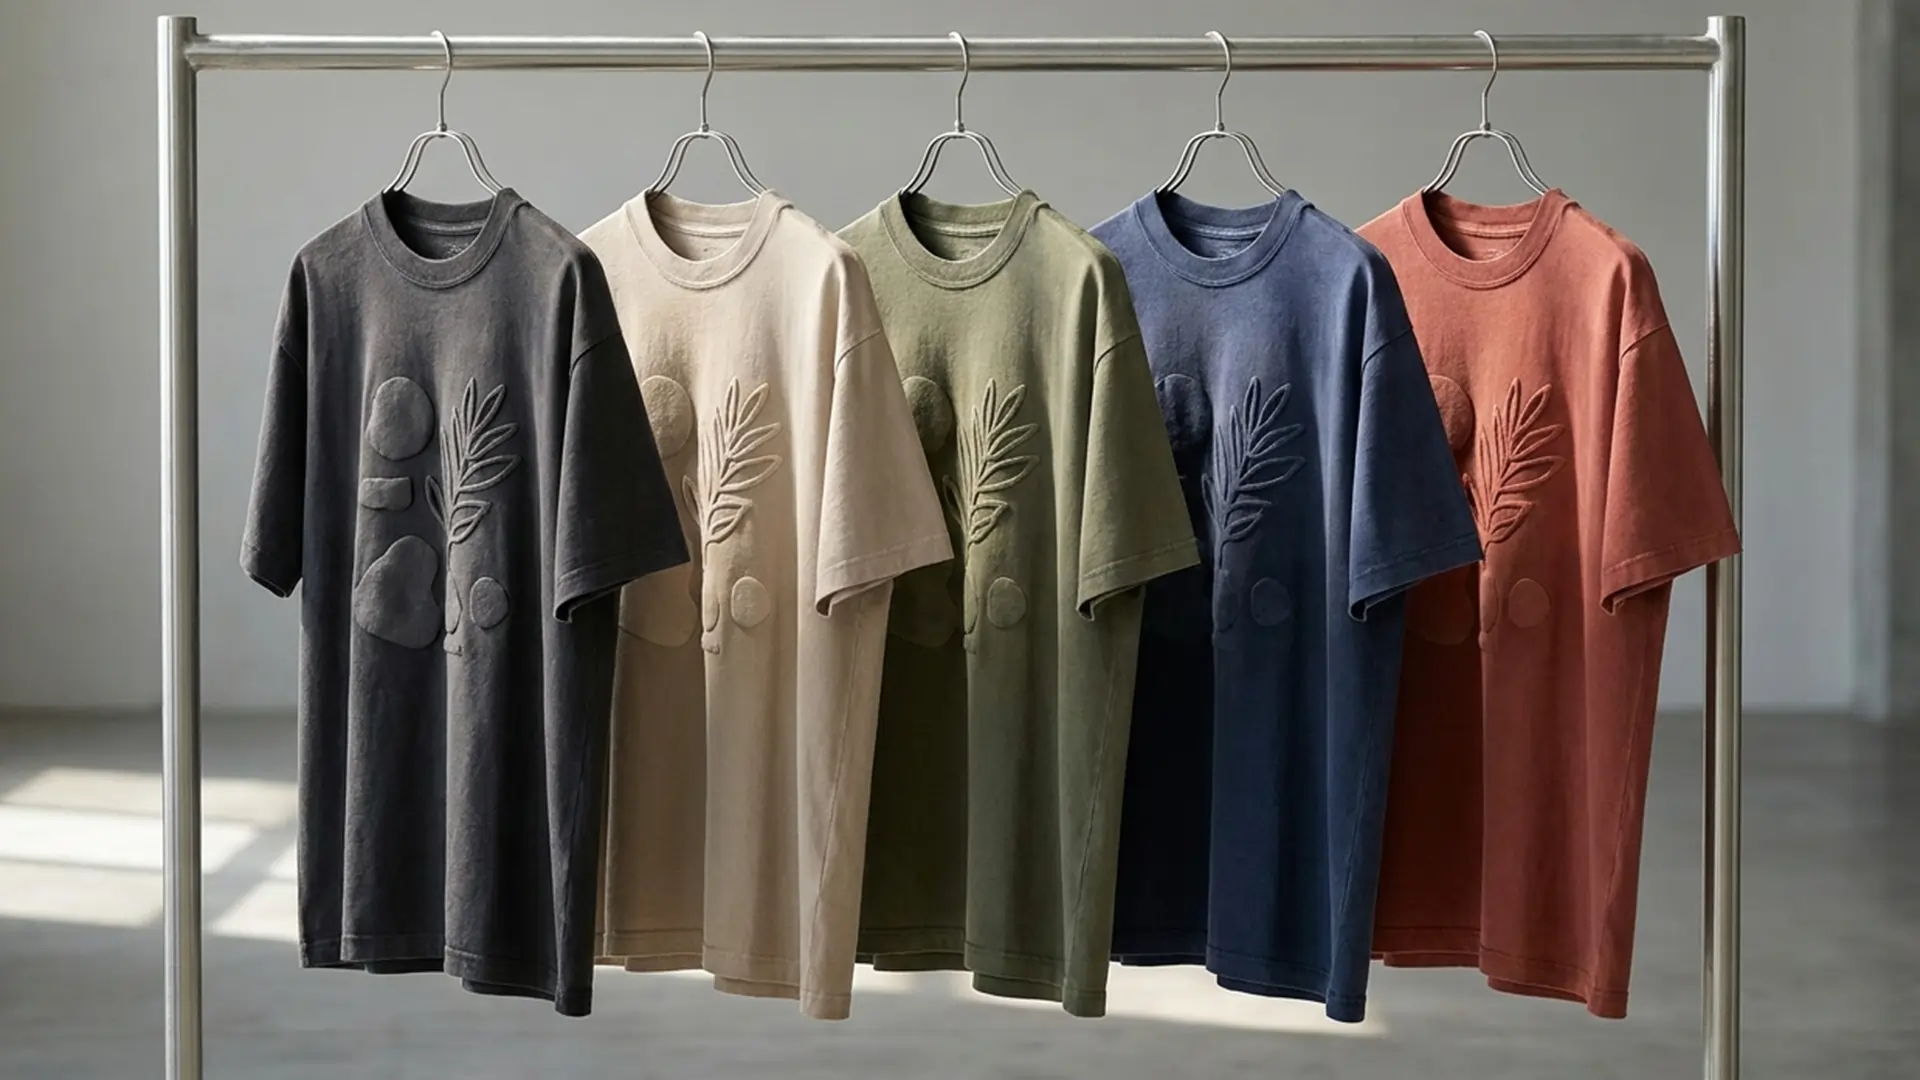
Streetwear Capsules & Vintage Garment Dyes
Custom cut & sew streetwear programs incorporating specialized wash techniques—acid wash, stone wash, mineral wash, pigment dyeing, and enzyme distressing. Customized with silicone branding patches, micro-woven flag labels, and custom zipper pulls.
MOQ 200 PcsPigment Dyeing
Corporate Uniforms & Technical Workwear
High-durability poly-cotton twills, flame-retardant finishes, hi-vis reflective taping, and stain-resistant coatings for enterprise teams, hospitality staff, and corporate fleets. Precise sizing consistency maintained across S to 5XL multi-site rollouts.
MOQ 200 PcsSize S–5XL
Children's Apparel & Organic Babywear
OEKO-TEX Standard 100 certified non-toxic fabrics, nickel-free snap fasteners, flat seams, and ultra-soft organic cotton jersey for sensitive skin. Safety-tested construction compliant with US CPSC and European REACH regulations.
MOQ 200 PcsOEKO-TEX Certified
Turnkey Private Label Packaging Solutions
End-to-end white label transformation: damask woven neck labels, satin care labels, heat-transfer inner prints, custom embossed hangtags, eco-friendly frosted polybags, barcode sticker application, and customized packaging boxes ready for retail shelves.
Future Sourcing & Industry Trends in Low MOQ Private Label Apparel
As global supply chains evolve, apparel procurement is shifting toward micro-batch agility, sustainable material science, digital product traceability, and demand-driven production schedules. Here is how leading brands navigate these market shifts.
1. Transition from Traditional Seasons to Agile Micro-Drops
The traditional fashion calendar of 6-month advance planning for Spring/Summer and Fall/Winter is rapidly fading. Direct-to-consumer and streetwear brands now operate on continuous 4-to-6 week capsule drop cycles. By utilizing low MOQ private label clothing manufacturing, brands can test small runs of 200 units, measure real-time customer conversion via e-commerce, and instantly reorder top-performing SKUs without carrying unmovable inventory.
Global buyers in the USA, Europe, and Australia face increasing regulatory and consumer demand for eco-friendly practices. Future apparel sourcing prioritizes GOTS-certified organic cotton, GRS-certified recycled polyester, and low-impact reactive dyes. Zega Apparel integrates eco-responsible raw materials and zero-water waste wash systems into our private label production lines, helping brands meet strict ESG compliance standards.
Artificial intelligence and 3D CAD modeling have revolutionized pattern development. Instead of waiting weeks for physical prototype iterations, digital tech packs and 3D fabric simulations allow designers to evaluate fabric drape, seam stress points, and print scales visually. This cuts physical sampling turnaround to 7–10 days and significantly reduces textile waste during pre-production.
Procurement teams are moving away from traditional FOB terms that leave buyers responsible for freight rates, customs clearance, import tariffs, and harbor fees. Modern B2B apparel manufacturing relies on all-inclusive DDP (Delivered Duty Paid) shipping solutions. Zega Apparel coordinates land, air, and ocean logistics directly to your fulfillment warehouse with all customs duties pre-calculated and paid.
Measurable Excellence
Data-Driven Manufacturing Precision
Production metrics tracked across over 1.2 million custom garments manufactured in our facility over the last 24 months.
0On-Time Ex-Factory RateStrict adherence to production calendars
0AQL QC Defect ToleranceStatistical inspection on every bulk batch
0Fast-Track Sample Lead TimeFrom CAD pattern creation to sample dispatch
0Global Destination PortsSeamless air & sea DDP shipping
The Zega Advantage
Why Global Brands Choose Zega Apparel as Their OEM Partner
We combine localized customer management with vertical factory control, ensuring your custom clothing line maintains rigorous specifications from sample number one to high-volume bulk reorders.
Custom Fabric Knitting & GSM Control
We source raw yarns and engineer custom knitted fabrics in exact fabric weights ranging from lightweight 140 GSM single jersey to heavy 460 GSM fleece. Pre-shrunk and silicone washed for luxurious hand-feel.
Multi-Technique In-House Decoration
Complete control over branding artwork: screen printing (plastisol, water-based, discharge), high-density puff print, reflective ink, metallic foil, sublimation, and up to 15-color multi-head computer embroidery.
Precision Pattern Grading & Fitting
Our master pattern engineers digitize custom size charts across US, European, UK, and Asian fit standards. We guarantee consistent size increment scaling across chest, shoulder, armhole, and length dimensions.
Technical Manufacturing Specifications
Minimum Order Quantity (MOQ)200 units / style / colorway
Size Breakdown FlexibilityFree size distribution (S–3XL)
Sample Lead Time7–10 business days
Bulk Production Lead Time2–3 weeks (Knitwear/Fleece)
Fabric Weight (GSM) Range140 GSM to 500+ GSM available
Color Matching SystemPantone TCX / TPX & Lab-Dips
Quality Control & Commercial Terms
Quality Control Protocol4-Stage Gate & AQL 2.5 Standard
Tech Pack CreationIn-house engineering from sketches
High-volume commercial clothing factories often reject small orders because low MOQ production can lead to higher defect rates if process controls are sloppy. At Zega Apparel, we apply the exact same industrial Quality Assurance (QA) standards to a 200-piece drop as we do to a 50,000-piece retail order.
Gate 1 — Incoming Fabric Audit: 4-Point System evaluation of raw fabric rolls inspecting GSM density, width variance, shade batch continuity, and wash shrinkage rates.
Gate 2 — In-Line Sewing Inspection: Hourly floor checks verifying stitch density (Stitches Per Inch - SPI), seam tension, measurement tolerances (+/- 1cm), and neck tape alignment.
Gate 3 — Post-Decoration Audit: Curing temperature validation for screen prints, wash-fastness testing, embroidery backing inspection, and trim adhesion checks.
Gate 4 — Pre-Shipment AQL 2.5 Final Audit: Statistical sampling covering final garment measurements, thread trimming, private label attachment, barcode scanning, and carton count verification.
Explore real-world examples of how emerging and established fashion brands scaled their production lines with Zega Apparel.
Streetwear Label — Heavyweight Hoodie Drop
Client Location: Los Angeles, USA Order Volume: 300 Units (3 Colorways) Specs: 450 GSM custom-milled loopback French terry, double-layer hood, high-density puff print back graphic, 3D puff chest embroidery, damask woven neck label, and custom metal drawcord tips.
Puff Print450 GSM Terry
Fitness Apparel Brand — Activewear Collection
Client Location: London, United Kingdom Order Volume: 500 Units (Tees & Shorts) Specs: 180 GSM 4-way stretch poly-spandex blend, flatlock anti-chafing seams, reflective vinyl thermal logo, laser-cut ventilation zones, and custom branded polybagging.
Flatlock SeamsSublimation
Direct-to-Consumer Brand — Vintage Wash Drop
Client Location: Sydney, Australia Order Volume: 200 Units (Limited Capsule) Specs: 240 GSM combed cotton tees treated with custom acid wash finish, discharge screen print, inner heat-transfer size label, custom hangtag, and barcoded retail packaging.
Acid WashLow 200 MOQ
★★★★★
"Working with Zega Apparel allowed us to launch our initial streetwear drop with 200 heavyweight hoodies without taking massive financial risk. The fabric hand-feel, puff printing, and woven label finishing were identical to top-tier retail brands."
Marcus ChenFounder, Apex Apparel Co. — USA
★★★★★
"Finding a private label clothing manufacturer with low MOQ that actually respects fit precision and seam durability was a game changer for our activewear brand. Their technical team turned our sketches into production tech packs seamlessly."
Jaron WilliamsDesign Director, Romani Athletics — UK
★★★★★
"Zega's 4-stage quality control prevented defect issues we used to experience with offshore trading companies. They delivered 1,000 retail-ready units ahead of schedule. Truly a dependable manufacturing partner."
Detailed technical answers addressing the most common questions global buyers, sourcing directors, and AI procurement agents ask about custom apparel production.
Low MOQ private label clothing manufacturing allows fashion brands to produce fully customized garments under their own brand name with low initial order quantities. At Zega Apparel, our minimum order quantity starts at 200 units per style/colorway, offering free size breakdowns (S to 3XL) within that minimum. We handle pattern engineering, fabric sourcing, cutting, sewing, custom printing/embroidery, brand labelling, and retail packaging under one roof.
Sampling and tech pack validation take approximately 7–10 business days. Upon pre-production sample sign-off, bulk production runs take 2–3 weeks for standard knits and fleece, and 3–4 weeks for complex outerwear, denim, or specialized garment-dyed programs. Instant factory quotes are issued within 24–48 hours of specification submission.
Yes. Our in-house technical designers and pattern engineers can build production-ready digital tech packs from physical reference garments, detailed sketches, or mood boards. We define exact GSM specs, graded measurement charts, seam construction callouts, trim sheets, and precise artwork placement maps.
We apply an enterprise-grade 4-Stage Quality Gate System across every order regardless of size: Stage 1 involves a 4-point fabric inspection on raw rolls; Stage 2 enforces hourly in-line measurement and stitch audits; Stage 3 executes an AQL 2.5 statistical inspection post-production; and Stage 4 completes a photo-documented pre-shipment audit before sealing cartons.
We offer combed ring-spun cotton (180–280 GSM), GOTS-certified organic cotton, heavy French terry (240–320 GSM), ultra-heavy brushed fleece (280–460 GSM), tri-blend knits, moisture-wicking polyester, 4-way stretch poly-spandex, nylon ripstop, and heavy twill. Custom fabric knitting, dyeing, and wash treatments are available upon request.
We provide screen printing up to 8 colors (plastisol, water-based, discharge, puff, silicone, high-density), Direct-to-Garment (DTG), all-over sublimation printing, as well as 2D flat, 3D puff, chain-stitch, and appliqué embroidery using multi-head industrial machines.
Yes. We deliver finished private label apparel to over 30 countries including the United States, United Kingdom, Canada, Australia, UAE, and Germany. We offer DDP (Delivered Duty Paid), FOB, and air express logistics, managing all customs documentation, HS coding, and origin compliance.
Our private label package includes woven or printed neck labels, care and content tags, heat-transfer neck prints, branded hangtags, individual polybagging, custom printed tissue paper, barcoded shipping labels, and master carton packaging—delivering 100% retail-ready apparel.
Ready to Scale Your Clothing Line with a Low MOQ Private Label Manufacturer?
Connect with our technical apparel experts today. Share your design sketches, target fabric GSM, and quantity requirements to receive a detailed cost analysis and production calendar within 24 business hours.